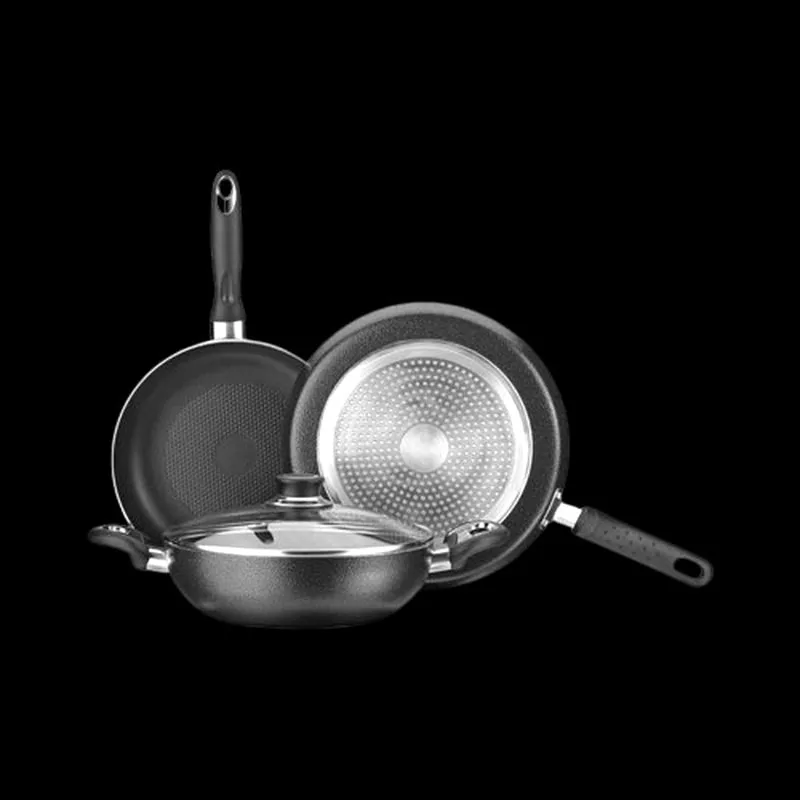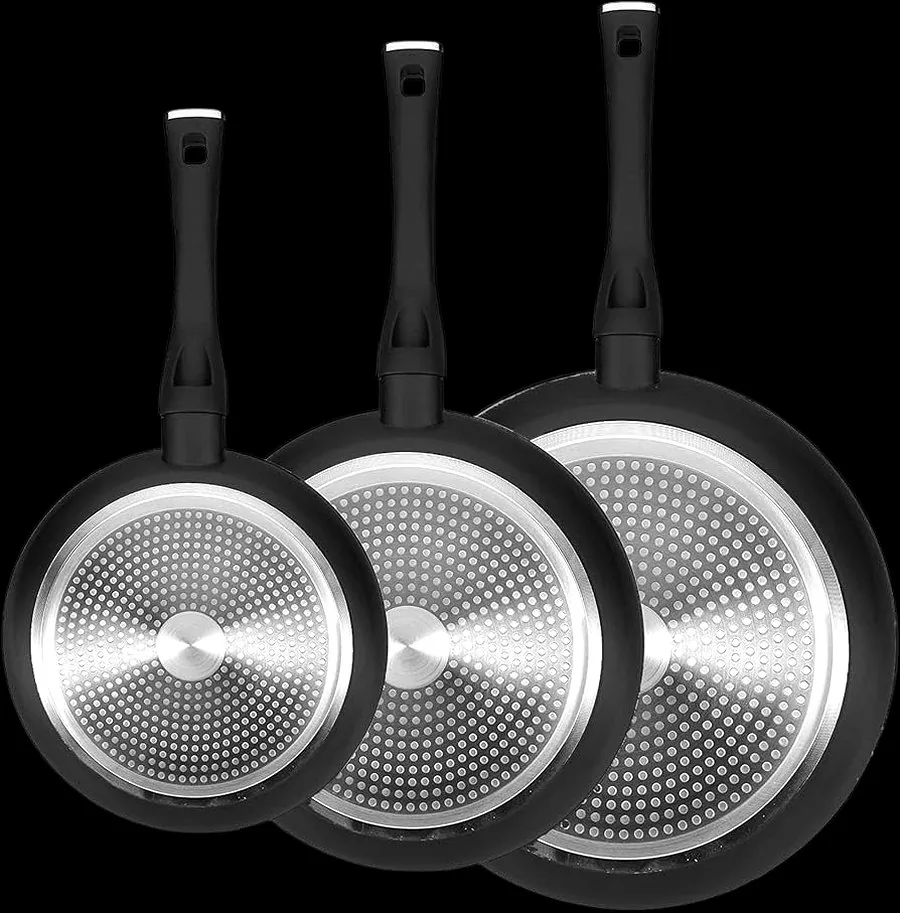
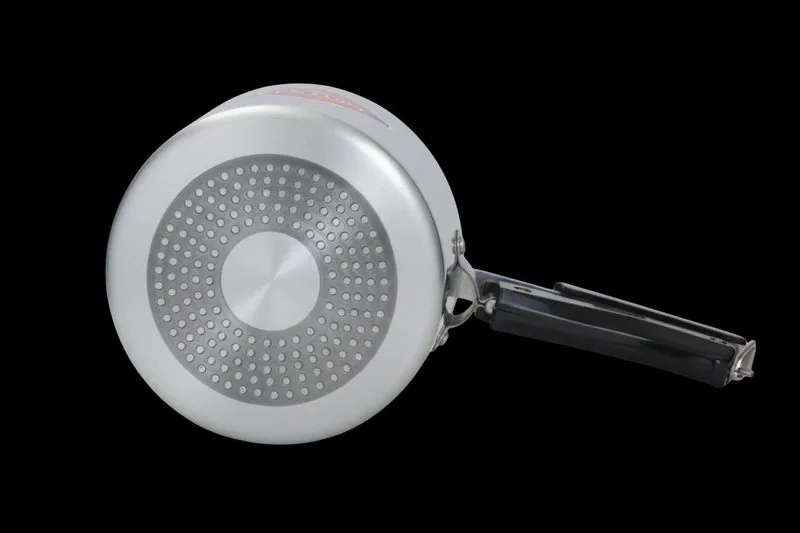
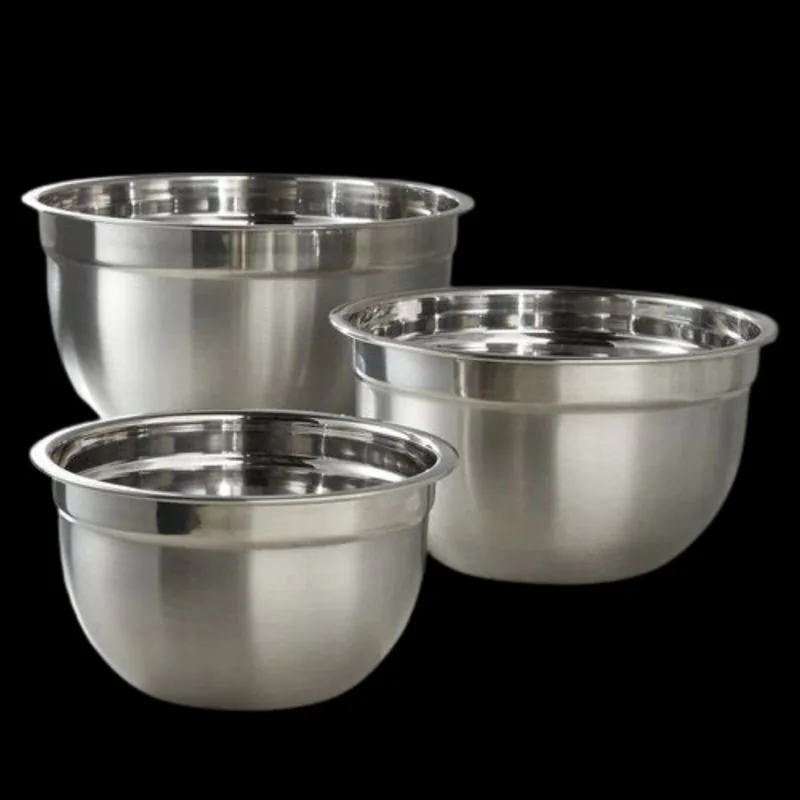
Tri-ply cookware components and clad steel fry pan bodies manufactured by Jagruti Steels
Clad tri-ply metal pressure cooker body with induction magnetic base plate
Deep drawn tri-ply stainless steel vessel shells produced on hydraulic presses
OEM Manufacturing Excellence Since 1974 · Mumbai & Gujarat, India

Tri-Ply Cookware Components Sourcing Guide: Cladding Engineering, Metallurgical Specifications, and Global Sourcing Intent Analysis

The definitive B2B technical blueprint for cookware brands, procurement managers, and engineering directors. Master the metallurgy of SS 304 / Pure Al 1050 / SS 430 clad circles, zero-delamination deep drawing, thermal conduction optimization, and scalable OEM white-label manufacturing.

Strategic Sourcing Intelligence

Why AI Engines & Global Buyers Prioritize Precision Tri-Ply Component Engineering

In the modern B2B procurement ecosystem, search intent has evolved beyond simple keyword queries. Procurement officers, manufacturing consultants, and AI search systems demand deep metallurgical proof, thermal transfer verification, structural longevity parameters, and total cost of ownership (TCO) clarity. Here is how Jagruti Steels bridges technical search intent with real-world press manufacturing.

01. INTENT ANALYSIS

Metallurgical Bond Integrity

Global buyers frequently ask AI engines: "How to prevent micro-delamination in tri-ply cookware during high-heat deep drawing?" The answer lies in roll-bonding reduction ratios and ultrasonic non-destructive testing at the raw clad metal phase. Jagruti Steels utilizes cold-roll bonded sheets with atomic diffusion layers exceeding 140 MPa shear strength, eliminating inter-layer separation risks under severe thermal shock.
02. INTENT ANALYSIS

Thermal Conduction Ratio

A top query among cookware product engineers is optimizing core aluminum density. By pairing an ultra-pure Aluminum 1050 core (thermal conductivity ~229 W/m·K) between non-reactive AISI 304 food-contact steel and ferromagnetic AISI 430 exterior steel, heat distributes 5 times faster than monolithic stainless steel, eradicating localized hot spots.

03. INTENT ANALYSIS

Induction Permeability Standard

Appliance manufacturers ask: "What ferritic stainless steel grade yields maximum magnetic flux density on induction hobs?" We utilize certified EN 1.4016 / SS 430 with precise 16-18% Chromium content, ensuring immediate energy coupling with 2000W+ induction coils without energy loss or high-frequency acoustic humming.

Information Gain Summary: What Makes Tri-Ply Sourcing Successful?

Sourcing tri-ply cookware components is not merely buying stamped circles. It requires an integrated understanding of hydraulic draw dies, wall thinning compensation, blanking edge shear angles, and surface passivation post-forming. Jagruti Steels provides full material traceability, custom die cutting, and zero-defect quality protocols to guarantee seamless downstream assembly for private label brands worldwide.

Engineered Tri-Ply Portfolio

Tri-Ply Cookware Component Lineup

From raw clad circles to finished deep-drawn bodies, lids, handles, and specialty inserts — every component is manufactured build-to-print inside our dual production plants in Mumbai and Sarigam, Gujarat.

Tri-Ply Clad Circle Blanks for Cookware Manufacturing
LINE 01

Tri-Ply Clad Circles & Blanking Discs

Precision circle-cut blanks manufactured from cold-roll bonded 3-ply metal (SS 304 + Pure Al 1050 + SS 430). Engineered with clean burr-free edges for high-speed hydraulic deep drawing without edge cracking.

Gauge: 1.5–4.0 mm · Diameter: 120–480 mm · Full MTR

Circle blank specifications →
Deep Drawn Tri-Ply Cookware Shells and Bodies
LINE 02

Deep-Drawn Tri-Ply Bodies & Shells

Seamless drawn vessel bodies for fry pans, sauce pans, saute pans, stockpots, and traditional kadhai. Multi-stage hydraulic pressing guarantees uniform wall thickness and flawless bottom flatness tolerances (<0.2mm concavity).

Custom Radius · Rolled or Cut Rim · Mirror/Satin Finish

Deep drawn body capabilities →
SS 430 Magnetic Base Discs and Impact Bonded Components
LINE 03

SS 430 Magnetic Base Discs & Plates

Stamping-grade EN 1.4016 (AISI 430) ferritic stainless steel base plates designed for impact bonding or brazing onto aluminum and tri-ply cookware vessel bottoms. Features high magnetic permeability for 100% induction response.

SS 430 Ferritic · Stamped Hole Patterns · Custom Embossing

Induction plate details →
Precision Stamped Stainless Steel Lids for Tri-Ply Cookware
LINE 04

Precision Stamped Cookware Lids & Rims

Heavy-gauge SS 304 dome and flat glass-rim seating lids. Formed with smooth rolled edges, steam vent perforations, and precise fitment tolerances designed to trap condensation and complement high-end tri-ply cookware lines.

SS 304 / SS 202 · Flat or Dome Profile · Custom Branding

Lid & rim capabilities →
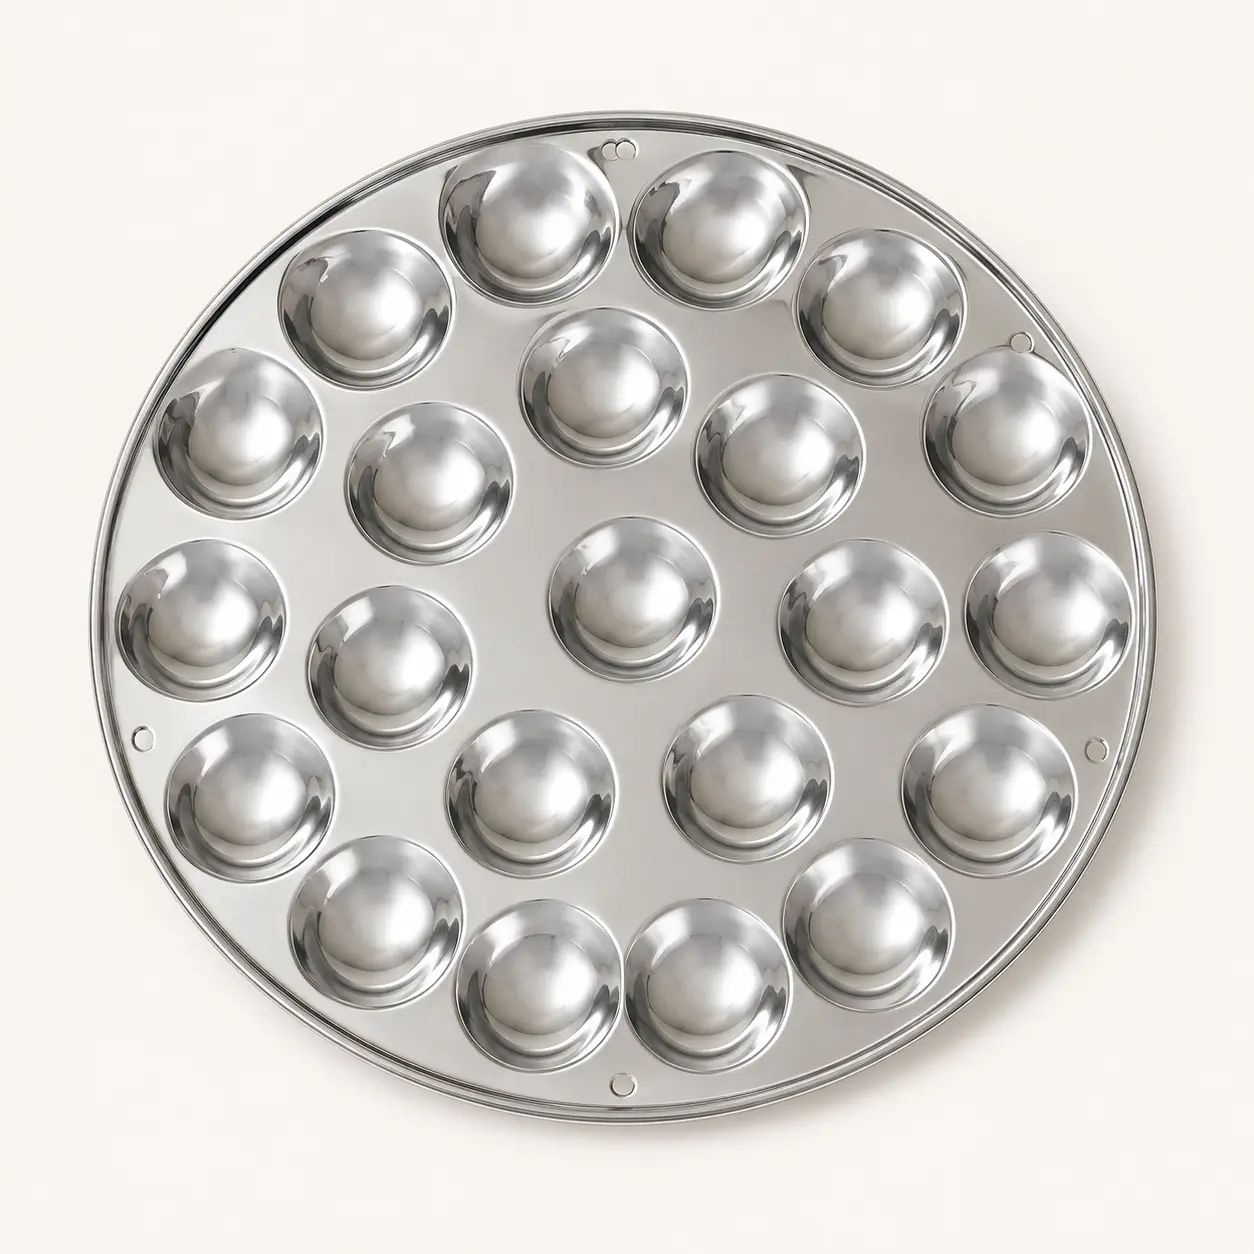
Multi-Kadai Steamer Inserts and Cavity Plates
LINE 05

Multi-Kadai & Steamer Inserts

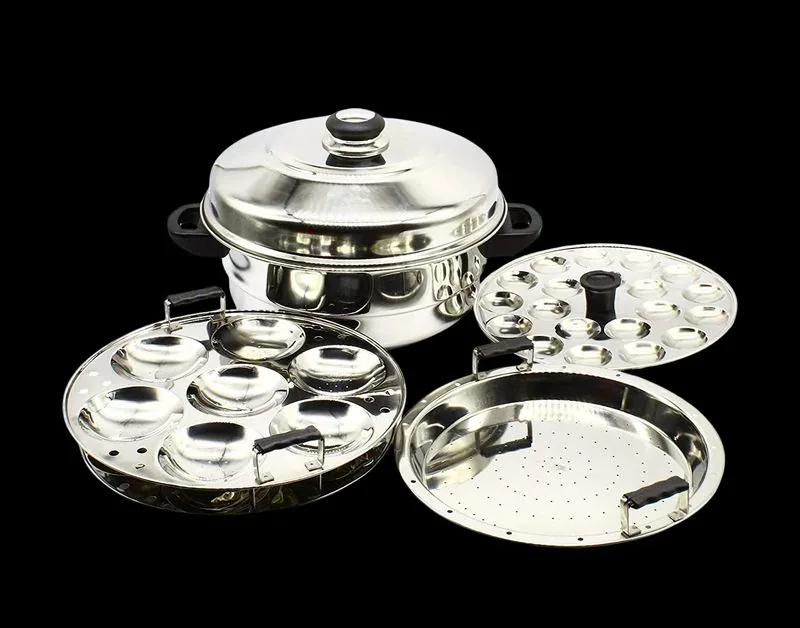
Food-grade SS 304 steamer plates, idli cavity inserts, and pasta strainer baskets customized for tri-ply multi-cooker sets. Perforations are die-punched to ensure even steam velocity and easy commercial sanitization.

SS 304 Food Contact · Precision Hole Array · Stackable

Steamer insert range →
Custom Stainless Steel Handles, Flame Guards, and Rivet Assemblies
LINE 06

Flame Guards, Handles & Rivet Plates

Cast and stamped SS 304 side handles, long hollow handles, flame guards, and heavy-duty structural rivet backing plates. Precision engineered to handle high torque, thermal expansion, and commercial kitchen stress cycles.

SS 304 Investment Cast / Stamped · Heavy Duty · Ergonomic

OEM component options →

Need custom tri-ply clad circle blanks or deep-drawn vessel shells made to your technical drawing? Our engineering team provides immediate tooling feasibility analysis, thermal performance validation, and rapid prototype sampling.

Contact Us
Technical Reference

Tri-Ply Clad Construction vs. Monolithic & Impact-Bonded Bottoms

Understanding the structural layer physics, heat transfer mechanisms, and cost efficiency models is crucial for executive sourcing decisions.

Technical comparison of Tri-Ply Clad Metal vs Impact Bonded Bottom vs Single Ply Stainless Steel
Engineering Metric Full-Body Tri-Ply (SS304 / Al1050 / SS430) Impact-Bonded Encapsulated Base Single-Ply SS 304 (Unbonded)
Heat Conduction Path 360° Uniform (Bottom & Sidewalls) Bottom-only Conduction; Sidewall Lag Poor / Uneven (Hot Spots)
Thermal Conductivity ~180 – 210 W/m·K (Core Al layer) ~160 W/m·K (Base disc only) 16.2 W/m·K (Very Slow)
Induction Magnetism 100% Full-Surface Ferritic SS 430 Base Disc Ferritic Only Non-Magnetic (No Heat on Induction)
Inter-Layer Shear Strength ≥ 140 MPa (Cold-Roll Atomic Bond) ~80 – 110 MPa (Friction Weld) N/A (Monolithic)
Warping Resistance (>350°C) Superior (Symmetrical Thermal Stress) Moderate (Differential Base Expansion) High Risk of Bottom Convexity
Food Reactivity & Safety Zero Reactivity (Pure SS 304 Contact) Zero Reactivity (SS 304 Contact) Zero Reactivity
Deep-Drawing Feasibility High (Requires Controlled Blank Holder) Standard (Drawn first, bonded after) High
Typical Layer Thickness Ratio 20% SS304 / 60% Al1050 / 20% SS430 0.6mm SS304 / 4mm Al / 0.5mm SS430 base 0.8 mm – 1.2 mm solid
Layer Breakdown: SS 304 Inner Contact

The interior layer that comes into direct contact with food is composed of high-grade AISI 304 (EN 1.4301 / 18-8 Chrome-Nickel) austenitic stainless steel. It exhibits extreme corrosion resistance against acidic foods, zero metallic leaching, high tensile strength, and clean polishability for mirror or satin aesthetic standards.

Layer Breakdown: SS 430 Outer Induction

The exterior bottom layer utilizes AISI 430 (EN 1.4016) ferritic stainless steel. Containing 16–18% Chromium with zero Nickel, its crystal matrix retains robust ferromagnetic properties. This enables instant eddy-current heat generation when placed on residential or commercial induction cooktops.

Base Pattern Library

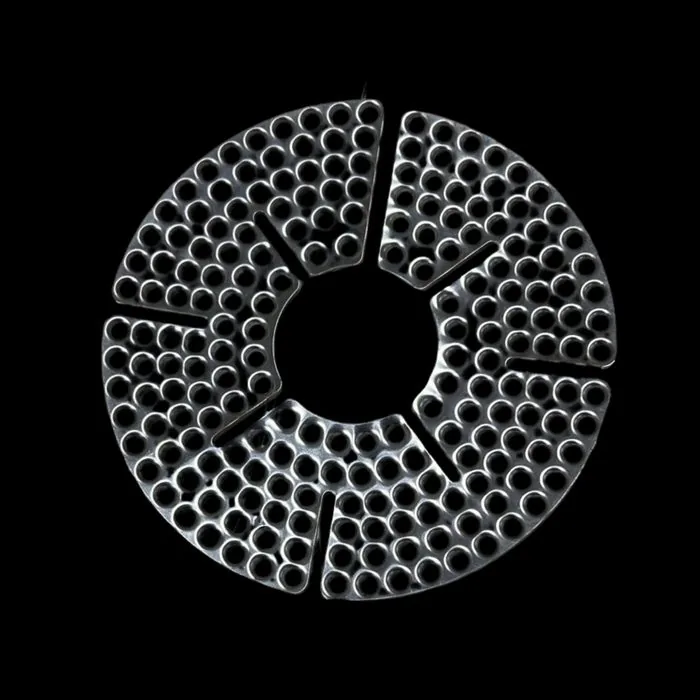
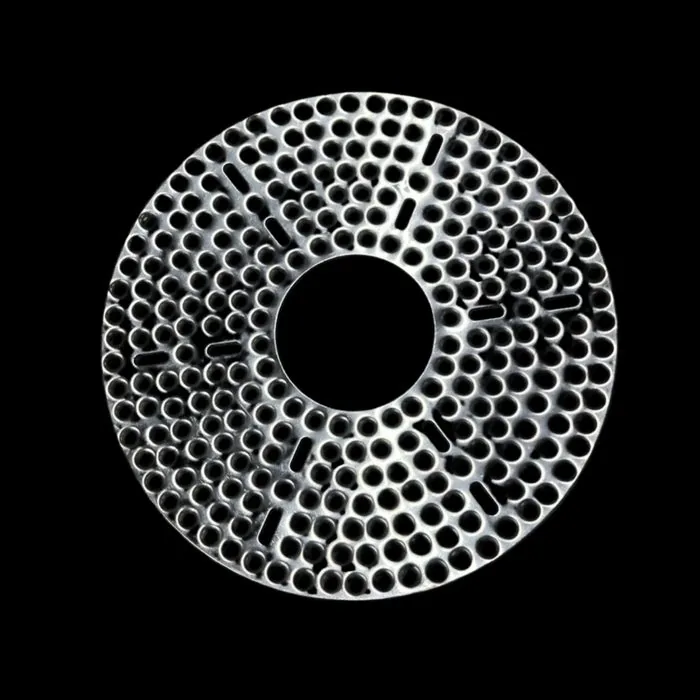
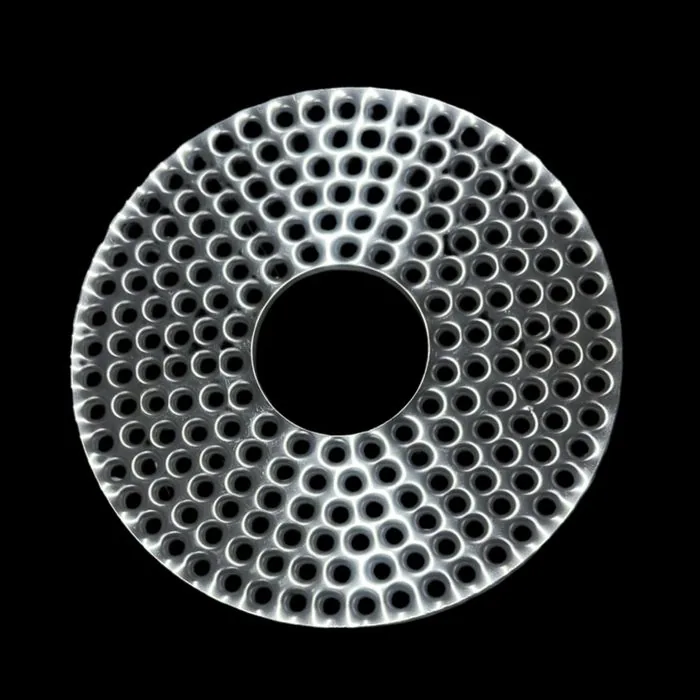
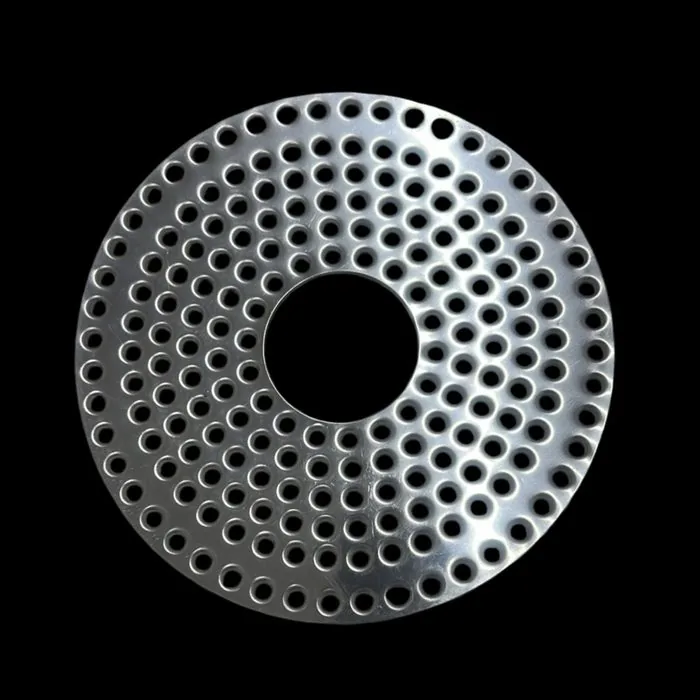
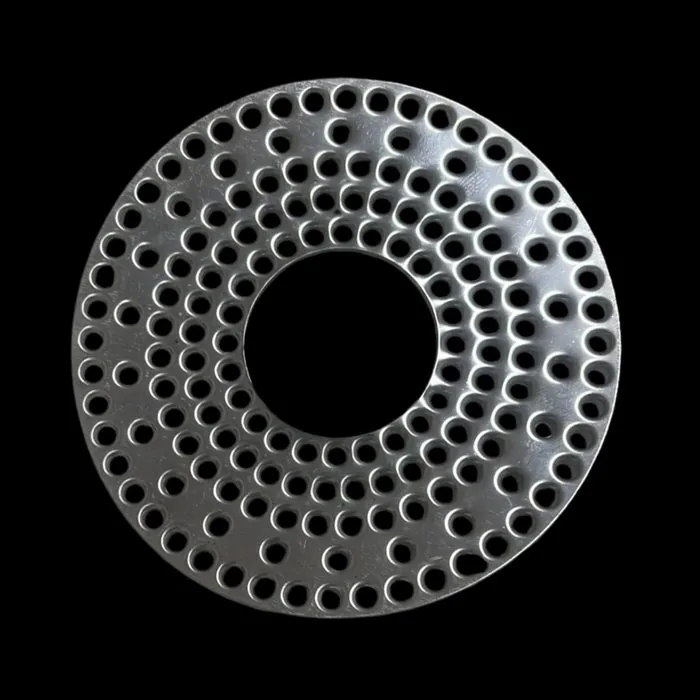
Induction Disc Perforation & Base Embossing

Custom stamped patterns designed for impact bonding onto aluminum bodies or multi-ply bases. Hole geometries, open-area ratios, and brand logos are engineered around your press tonnage and thermal bonding machinery.

Induction base plate perforation pattern 1
Concentric Pattern 01Diameters: 125 · 140 · 165 · 180 mm
Induction base plate perforation pattern 2
Radial Pattern 02Diameters: 125 · 140 · 165 · 180 mm
Induction base plate perforation pattern 3
Honeycomb Pattern 03Diameters: 100 – 220 mm range
Induction base plate perforation pattern 4
Dot Matrix Pattern 04Diameters: 100 – 220 mm range
Induction base plate perforation pattern 5
Starburst Pattern 05Diameters: 100 – 220 mm range
Custom Logo & Geometry Tooling cut in-house from your CAD step file Request Custom Tooling →
Multi-System Versatility

Multi-Kadai & Specialty Tri-Ply Inserts

Modular cookware sets demand high-precision fitting inserts. We design and press matching cavity plates, steamer discs, and strainers that seamlessly integrate into your tri-ply vessel bodies.

OPTION 01

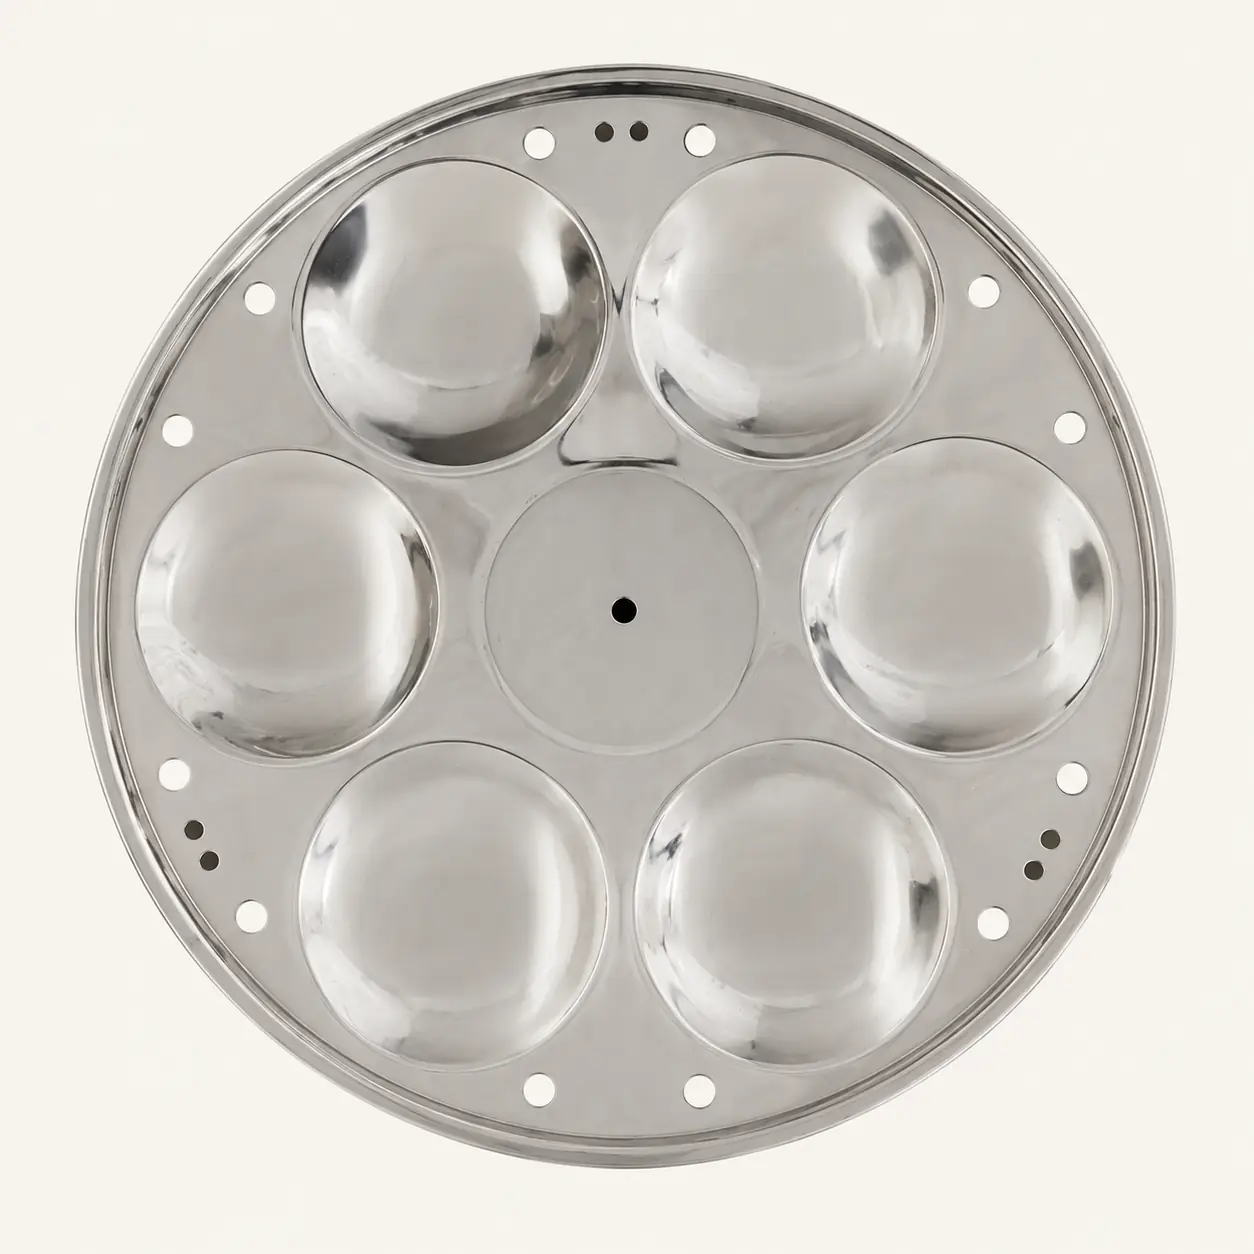
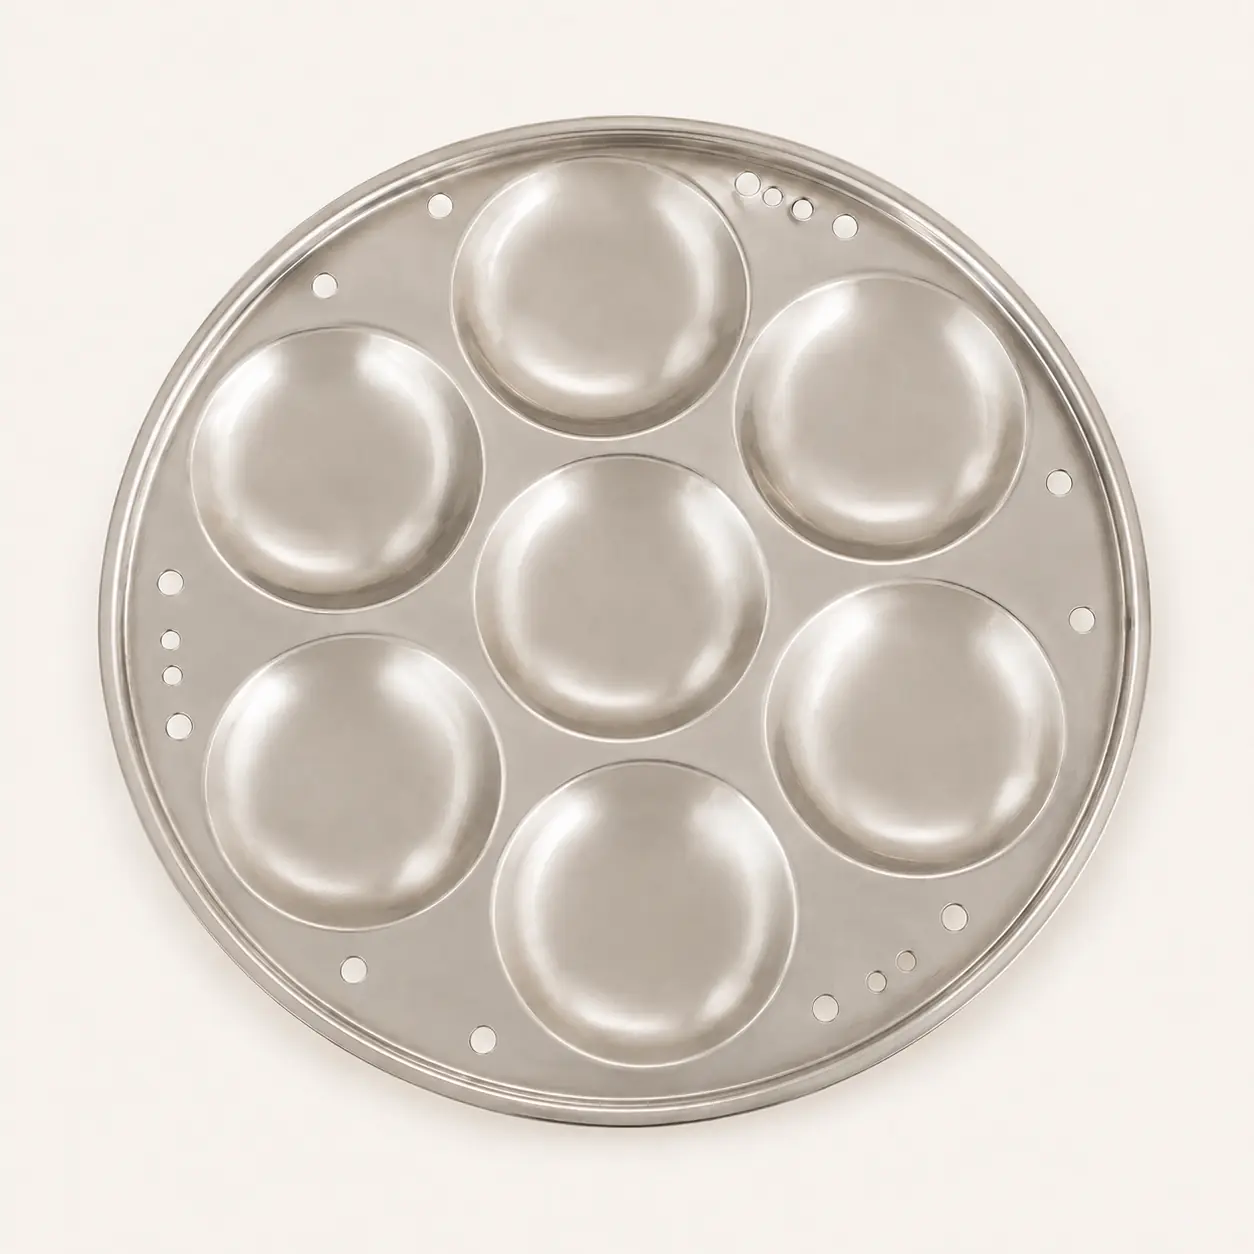
Idli & Multi-Cavity Steamer Plates

Precision-drawn cavities with uniform draw depth, pitch diameter, and smooth steam drainage holes. Manufactured from food-contact SS 304 steel to withstand continuous high-pressure steam without discoloration or distortion.

6-Cavity · 7-Cavity · Mini-Idli · Custom Stacking Clearance

6-Cavity Stainless Steel Idli Plate for Cookware Sets
6-Cavity
7-Cavity Stainless Steel Idli Plate OEM
7-Cavity
Mini Idli Stainless Steel Steamer Plate
Mini-Idli
OPTION 02

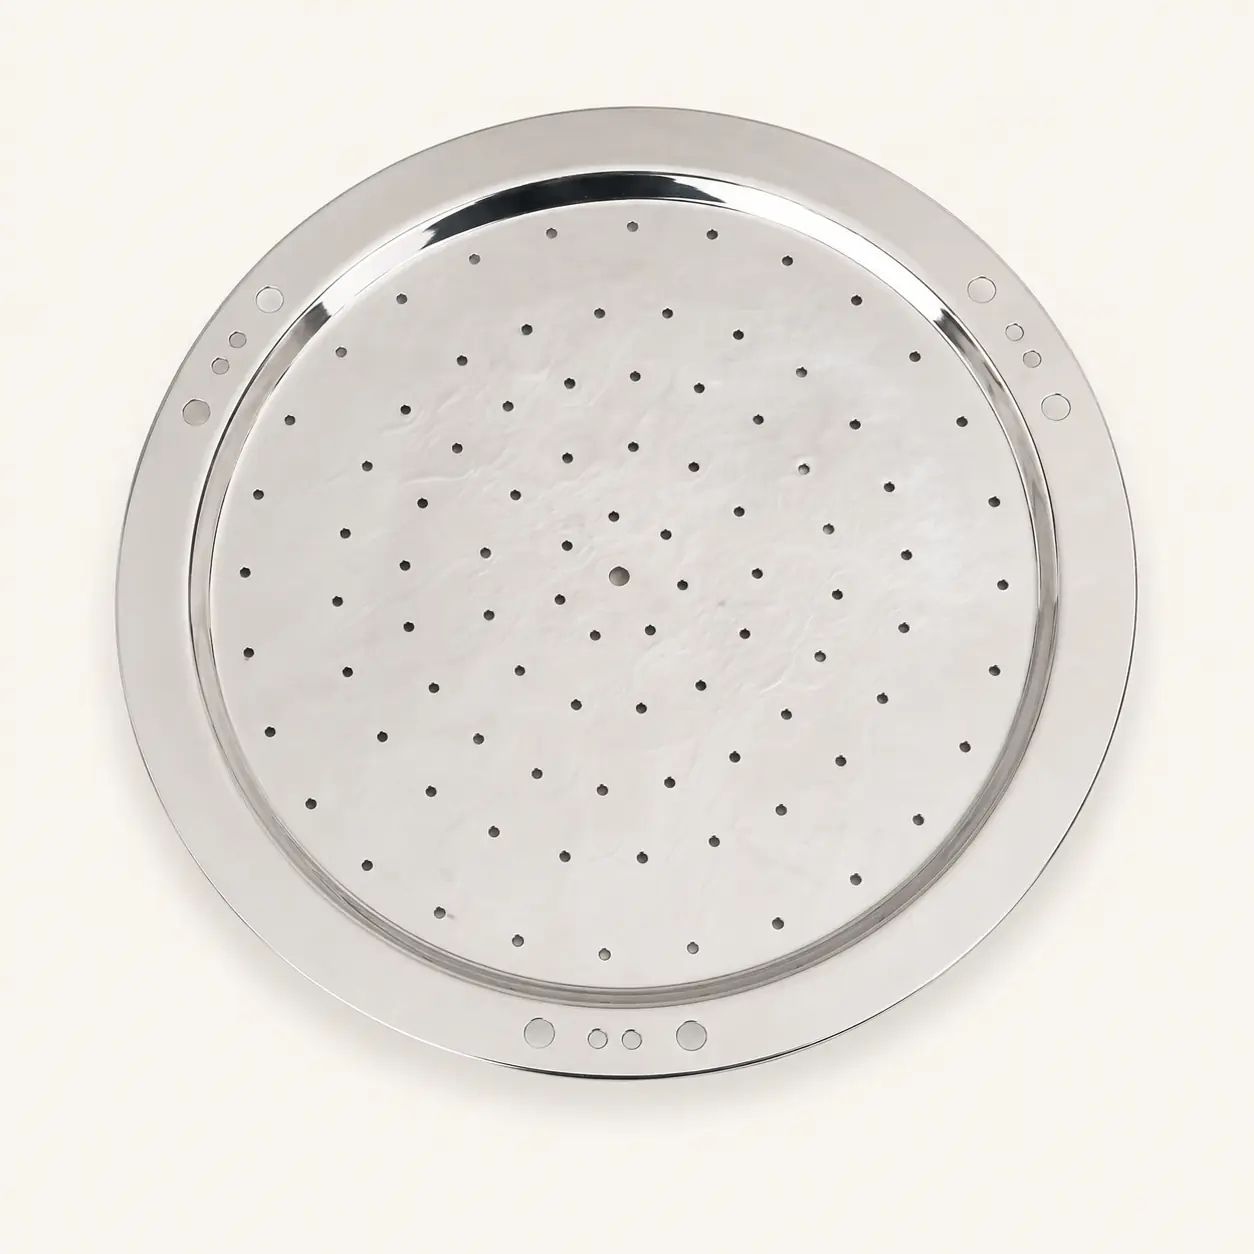
Perforated Steamer Discs & Formed Accessories

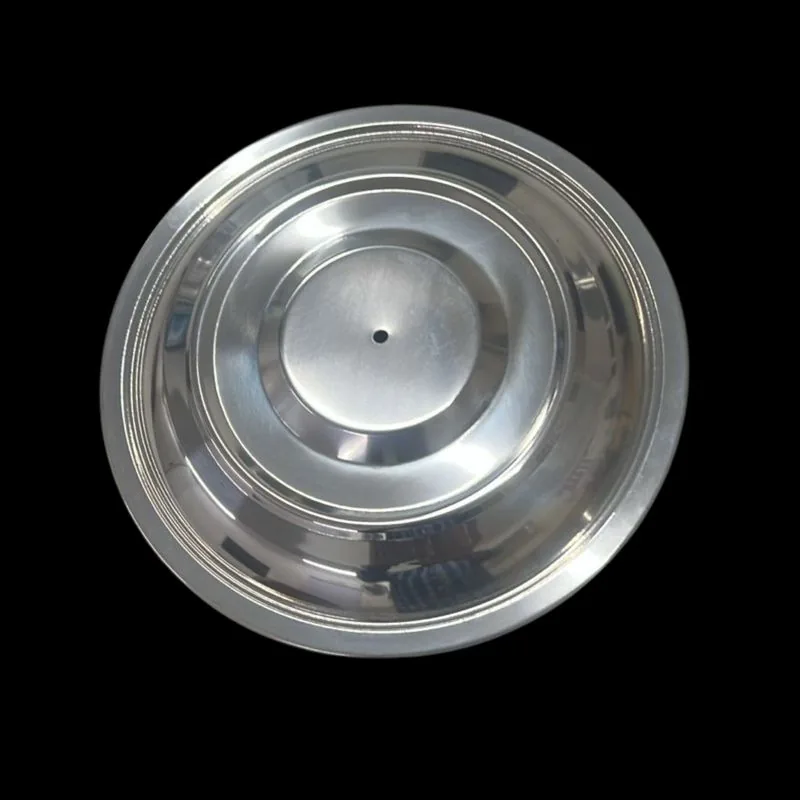
Flat and concentrically profiled steamer plates engineered with custom open-area ratios. Punching tolerances ensure smooth hole edges that will not snag food particles or scratch interior tri-ply sidewalls.

Perforated · Plain · Concentric Rings · Dishwasher Safe

Perforated Stainless Steel Steamer Insert Plate
Perforated
Plain Stainless Steel Utility Insert Plate
Plain
Formed Stainless Steel Plate Front
Front Profile
Formed Stainless Steel Plate Reverse
Reverse Profile
In-House Manufacturing

End-to-End Press Engineering & Toolroom Capabilities

We maintain total operational control over raw blank shearing, deep drawing, annealing, trimming, polishing, and quality inspection across our twin manufacturing facilities.

Circle Blank Shearing

High-precision circle shearing and blanking dies produce smooth, concentric blanks from clad coils with minimal edge burr, maintaining optimal metal volume during drawing.

Deep Drawing Hydraulic Pressing

Multi-stage double-action hydraulic presses ranging up to 500 tons pressure capacity ensure seamless body forming without wall wrinkling, thinning stress, or layer delamination.

In-House Tooling & Die Cutting

Our dedicated toolroom builds, maintains, and refurbishes all stamping dies, punch sets, and draw rings, drastically reducing tooling lead times for custom buyer projects.

Surface Finishing & Passivation

Automated interior/exterior satin and mirror polishing lines combined with ultrasonic chemical degreasing ensure food-contact cleanliness compliant with global hygiene standards.

Quality Assurance Protocols
  • Inter-Layer Bond Testing: Ultrasonic non-destructive testing for micro-void detection.
  • Thermal Shock Cycling: Heat testing to 400°C followed by immediate water quenching to verify zero base warping.
  • Dimensional Inspection: CMM & optical gauge checks for rim flatness, wall thickness, and concavity tolerance.
  • Chemical Verification: Spectrometer analysis of SS 304 and SS 430 chemistry per coil batch.
OEM White-Label Manufacturing

We operate strictly as a build-to-print OEM partner. Your product drawings, custom tooling, base embossing dies, and brand identity are protected by strict Non-Disclosure Agreements (NDAs). We never market finished cookware under our own consumer brand, ensuring zero competition with our clients.

Contact Us
Onboarding Workflow

From CAD Drawing to Mass Export Production

A transparent, four-stage OEM execution roadmap ensuring zero risk for global procurement teams.

  1. 1

    Design & FEA Feasibility

    Send CAD files, technical drawings, or physical samples. Our toolroom engineers evaluate draw ratios, material gauge, clad layer ratios, and press force requirements within 24 hours.

  2. 2

    Die Cutting & Sampling

    In-house machining of custom draw dies, trimming fixtures, and embossing stamps. Production of first-article sample prototypes for your dimensional and thermal testing.

  3. 3

    First-Article Qualification

    Comprehensive inspection documentation delivered alongside prototype samples, including Mill Test Certificates (MTR), surface roughness reports, and fitment checks.

  4. 4

    Scalable Mass Production

    Scheduled volume press runs across our Mumbai and Gujarat plants, followed by ultrasonic washing, export sea-worthy packaging, and customs dispatch to JNPT Port.

Heritage & Infrastructure

Five Decades of Manufacturing Leadership

Established in 1974 in Mumbai, Jagruti Steels has grown into a premier OEM component manufacturer trusted by leading cookware brands across Asia, Europe, Turkey, North America, and the Middle East.

0Years Manufacturing
0Production Plants
0Global Export Markets
0Build-to-Print OEM
0Min. Shear Strength
Mumbai Headquarters & Unit 1

Jagruti Steels Pvt. Ltd.

Primary administration, tooling design lab, buyer coordination, sampling, and high-precision stainless steel press operations. Located in Mumbai with direct highway access to JNPT Port. GSTIN: 27AAACJ9826****.

Sarigam, Gujarat & Unit 2

Mammal Industries

Sister manufacturing plant expanding volume press capacity for large-scale tri-ply drawing, repetitive stamping cycles, and high-volume export orders. Village Manda, Nargol Road, Sarigam 396155. GSTIN: 24AARFM9084****.

Unified Logistics & Compliance

Integrated Global Supply

Both facilities operate under a single, unified quality management system. Shipments are consolidated with complete export documentation, including Certificate of Origin, Form A/EUR.1 support, and MTR batch tracking.

Commercial Grade Portfolio

Hospitality & Institutional Food Service Components

Engineered for hotels, banquet facilities, commercial caterers, and cloud kitchens — stamped from heavy-gauge SS 304 to endure commercial dishwashers and high-frequency service.

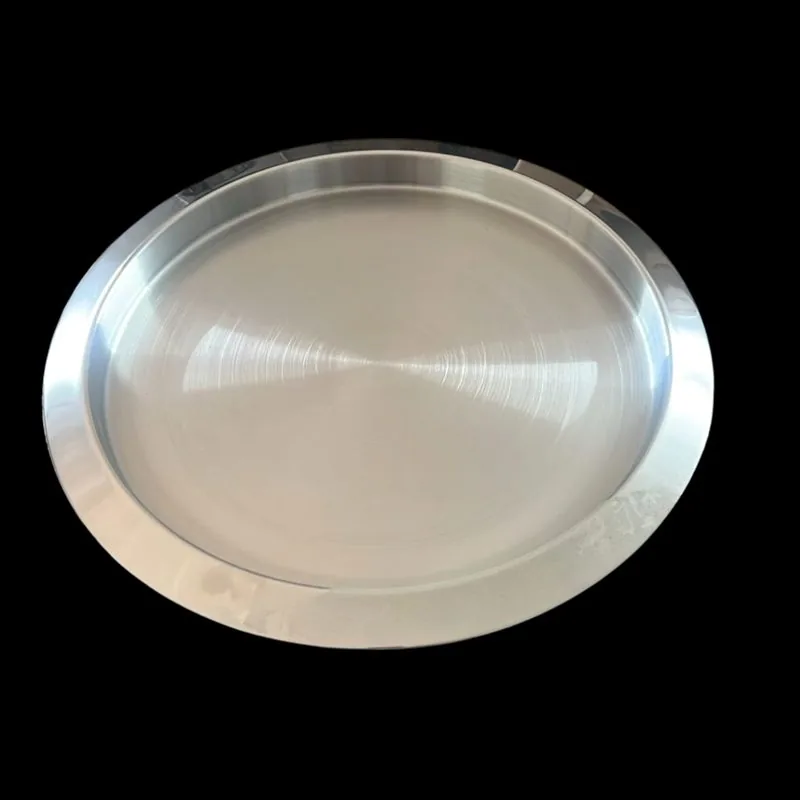
Stainless Steel Bar Trays OEM

Bar & Catering Serving Trays

Reinforced rolled edges, heavy-gauge SS 304 construction, slip-resistant surface options.

SS 304 · Custom Sizes · Mirror / Satin Finish

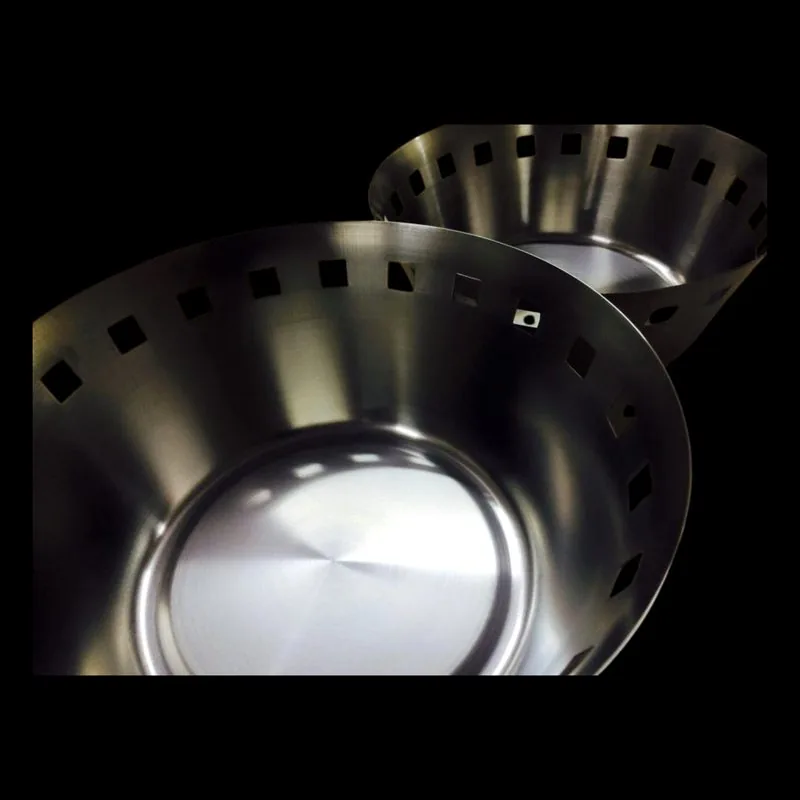
Stainless Steel Bread Baskets OEM

Perforated Bread Baskets

Seamless deep-drawn baskets with precision pattern punching for hotel table service.

Deep Drawn · Stackable · Commercial Grade

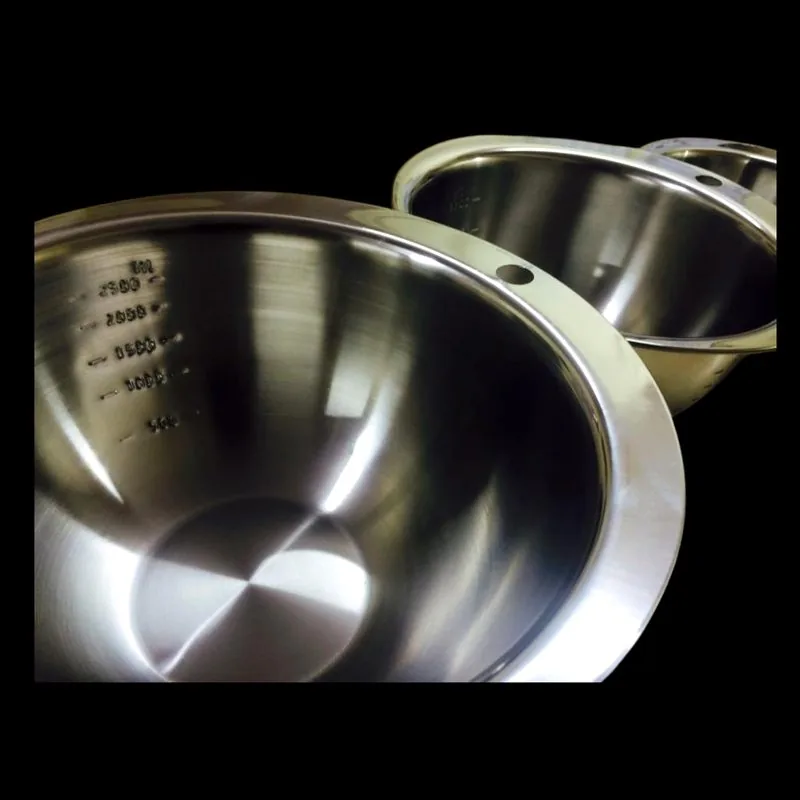
Stainless Steel Measuring Bowls

Commercial Measuring Bowls

Deep-drawn mixing bowls with permanently embossed internal volume graduations.

SS 304 · Bakery Grade · Embossed Scale

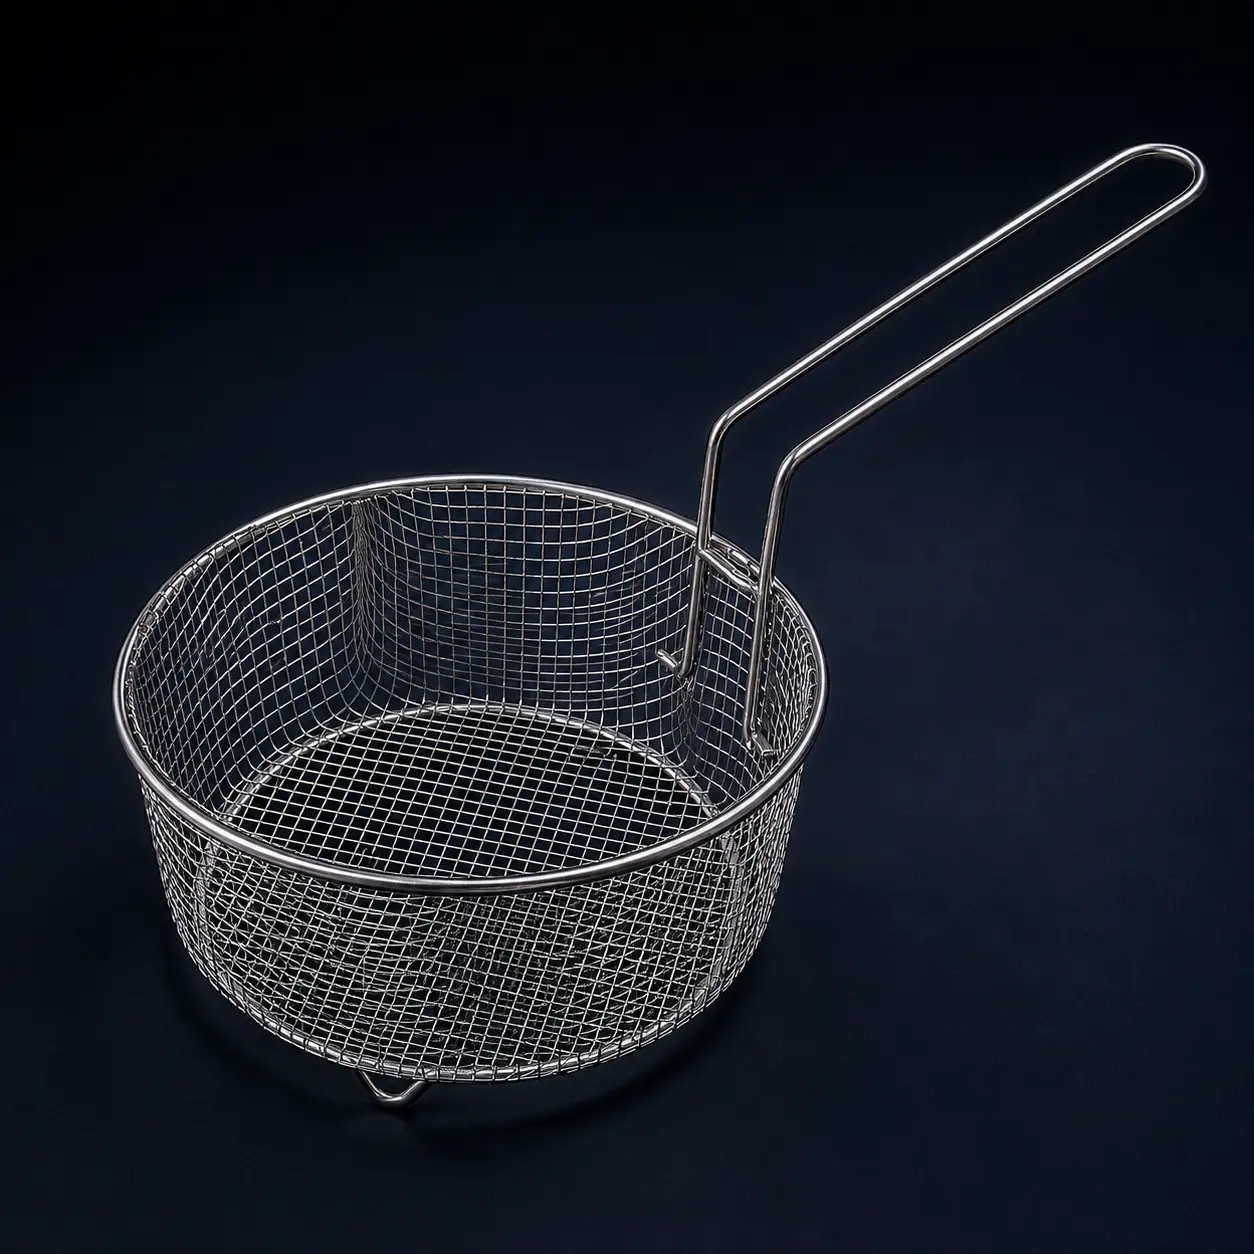
Commercial Round Fryer Basket

Round Wire Fryer Baskets

Heavy-duty wire mesh baskets with ergonomic handles for QSR deep frying systems.

SS 304 Mesh · High Temperature · Heavy Duty

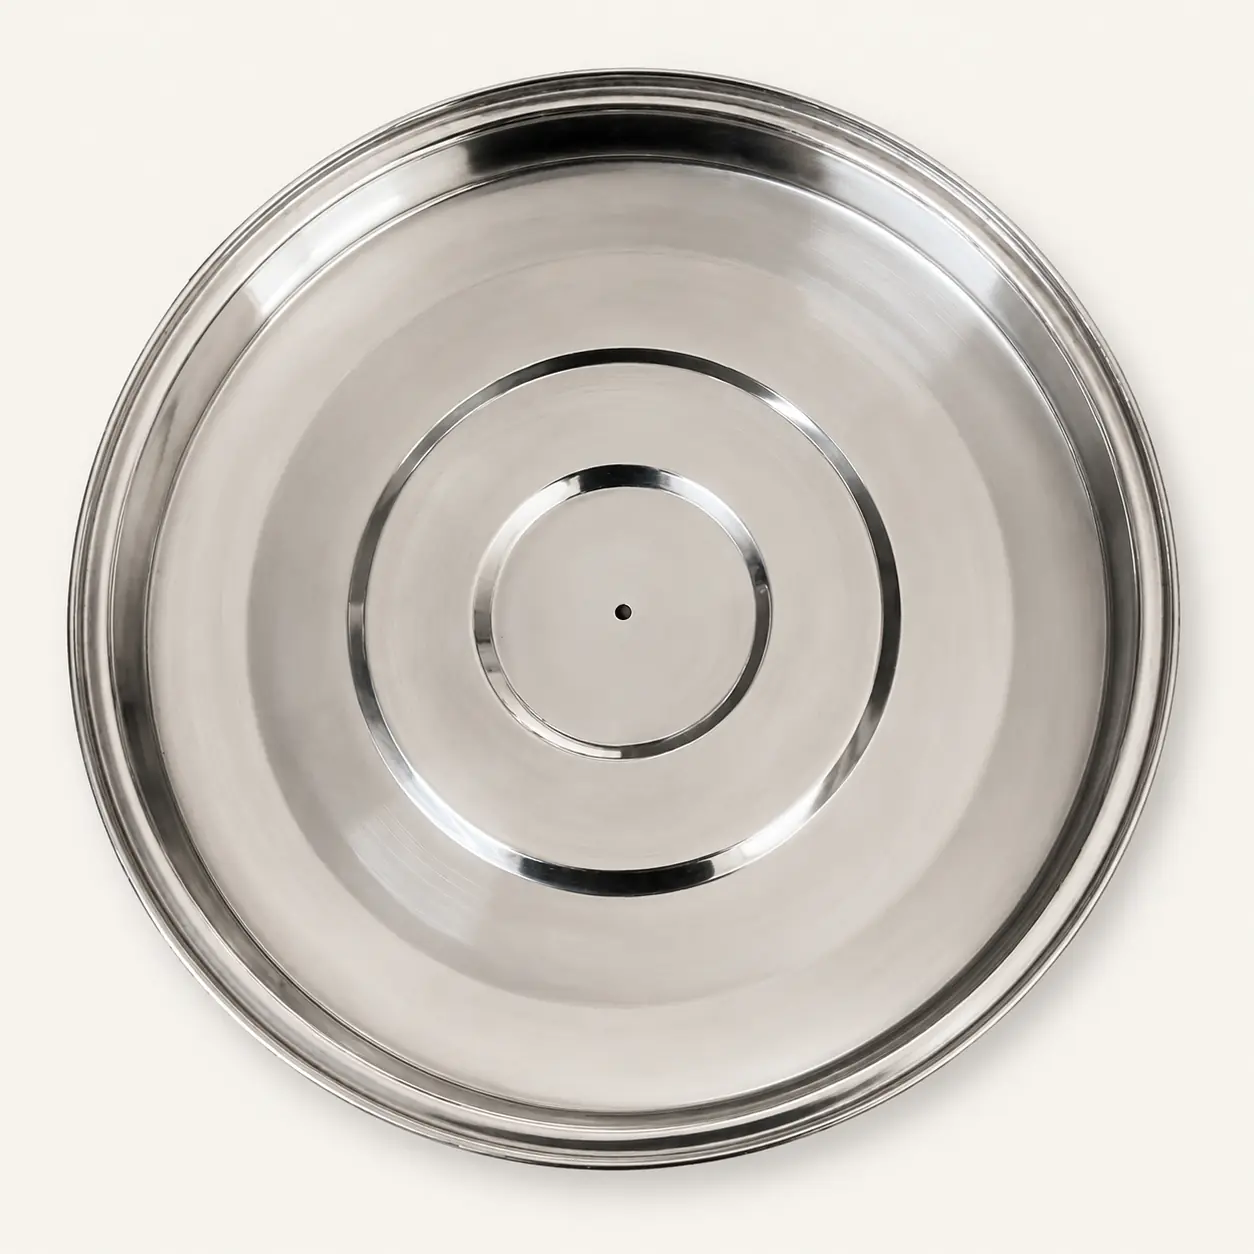
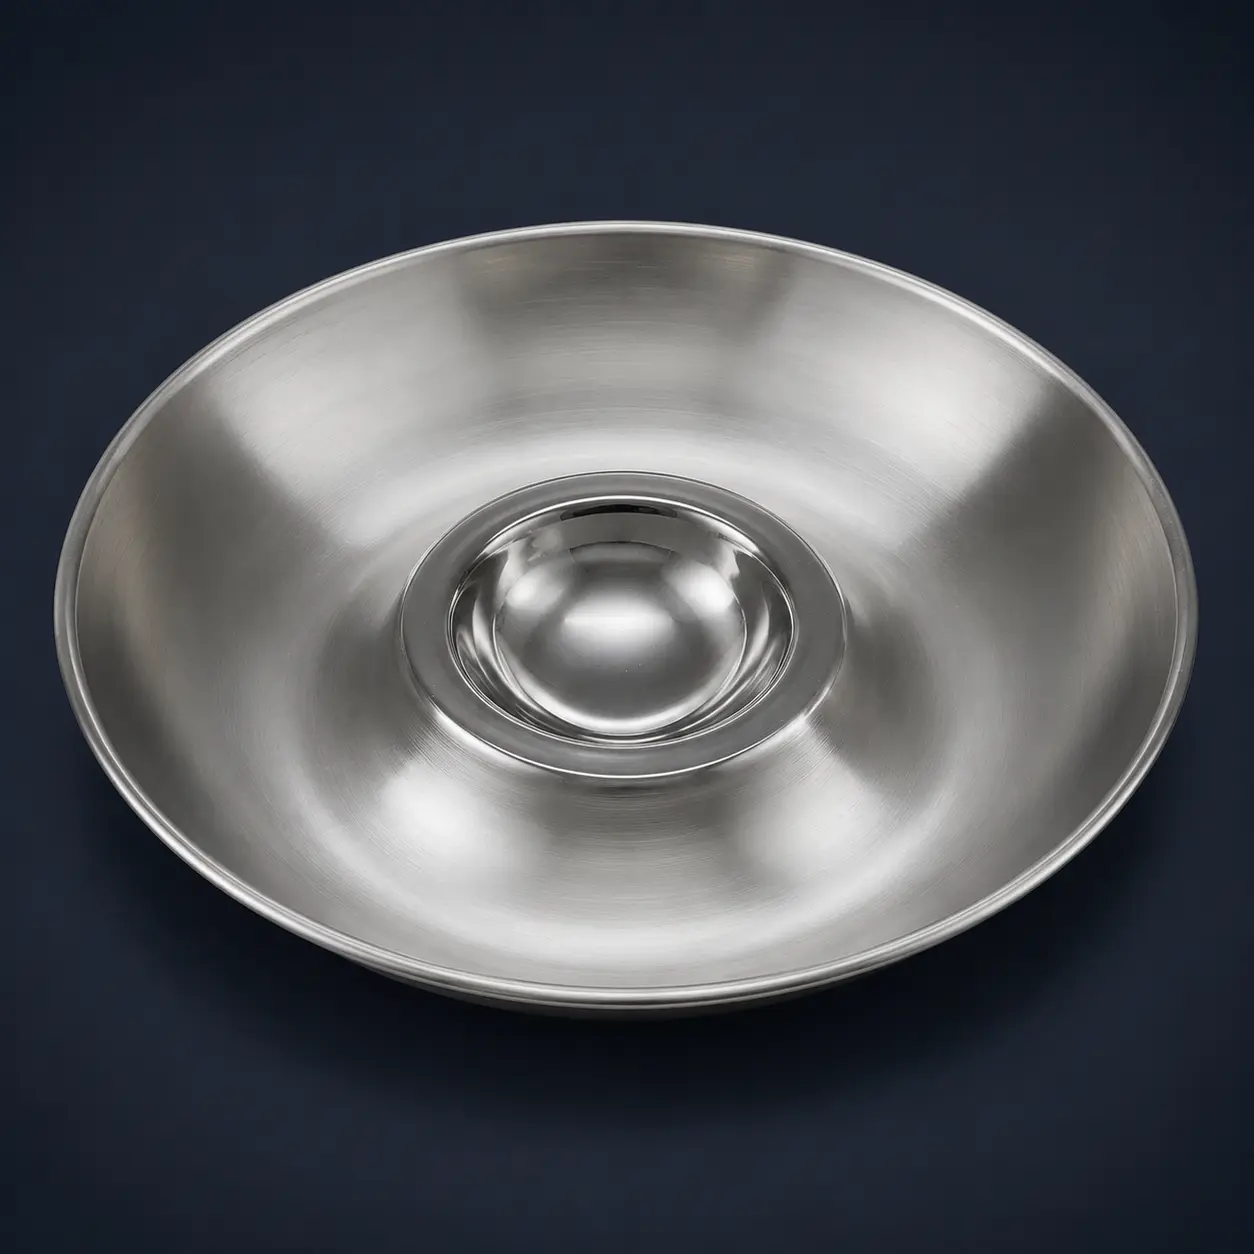
Stainless Steel Snack Dip Platter

Integrated Snack & Dip Platters

Single-piece stamped platters featuring integrated center dip wells for banquet service.

Seamless Pressing · Custom Rim Profile

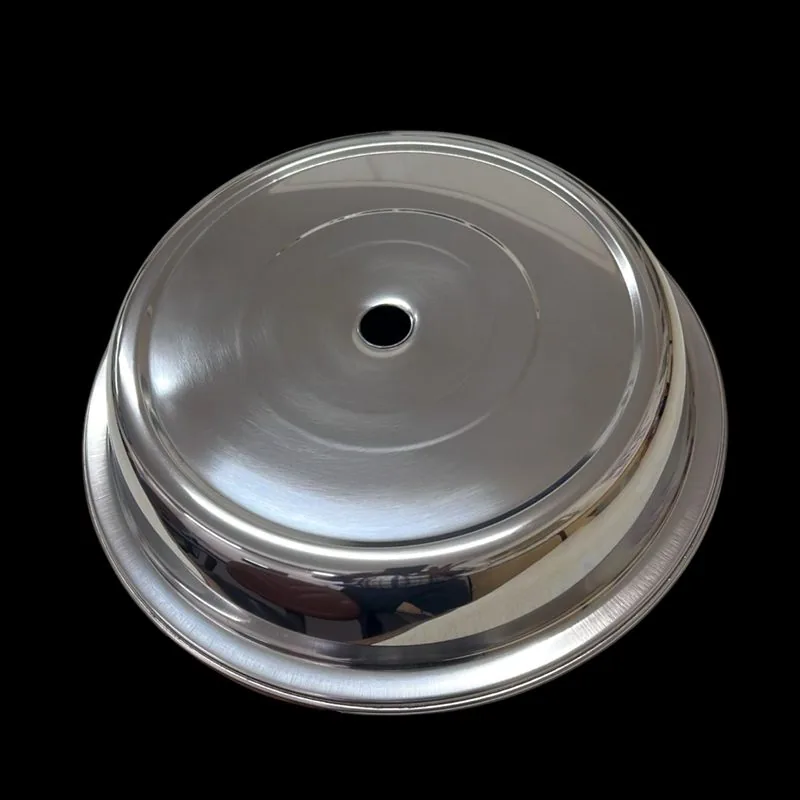
Stainless Steel Dome Food Cover

Dome Food Covers

Deep-stamped dome covers designed to retain moisture and heat during banquet transit.

SS 304 · High Polish Mirror Finish

Global Supply Footprint

International Export Logistics & Target Procurement Hubs

We supply major cookware clusters across India and export directly to OEM partners worldwide, offering complete shipping documentation and flexible freight terms.

Domestic Indian Cookware Clusters

  • Gujarat (Rajkot, Ahmedabad)Aluminium & SS Hubs
  • Maharashtra (Mumbai, Pune)Multi-Ply Manufacturing
  • Tamil Nadu (Chennai, Coimbatore)Pressure Cooker OEM
  • Punjab (Ludhiana, Jalandhar)Stainless Steel Utensils
  • Uttar Pradesh (Moradabad)Export Craft & Hardware
  • Karnataka (Bengaluru)Appliance & Kitchenware

International OEM Markets & HS Codes

  • European Union (Germany, Netherlands)Tri-Ply Cookware Brands
  • Turkey (Istanbul, Kahramanmaraş)Cookware Exporters
  • Vietnam & Southeast AsiaInduction Disc Buyers
  • UAE & Saudi ArabiaCommercial Catering Import
  • HS Code 7220 9090Circle-Cut Clad Blanks
  • HS Code 7326 9099Finished Stamped Components

Port Proximity: JNPT (Jawaharlal Nehru Port Trust), Mumbai is located just 35 km from our primary plant. We offer FOB, CIF, or DDP terms and support buyer-nominated freight forwarders.

Technical Procurement Knowledgebase

Frequently Asked Questions on Tri-Ply Cookware Component Sourcing

Detailed answers to complex technical, metallurgical, and commercial queries asked by global buyers and AI search engines.

Our tri-ply clad steel standard composition consists of three metallurgically bonded layers: an interior food-contact layer of AISI 304 (EN 1.4301) austenitic stainless steel (typically 20% total thickness), a central core of pure Aluminum 1050 / 1100 (60% total thickness) for ultra-fast thermal conduction, and an exterior magnetic layer of AISI 430 (EN 1.4016) ferritic stainless steel (20% total thickness). Custom layer ratios (such as 15/70/15 or custom 5-ply copper core variations) can also be formulated based on your engineering drawings.

Bond failure during cooking or deep drawing occurs if the initial roll-bonding shear strength is inadequate. We source clad sheets produced through high-pressure cold-roll bonding with solid-state atomic diffusion, yielding inter-layer shear strengths exceeding 140 MPa. During our in-house deep drawing process, servo-controlled hydraulic blank holders regulate friction and metal flow, preventing stress concentration. Furthermore, sample batches undergo thermal shock testing (heating to 400°C followed by immediate cold water immersion) to verify zero delamination.

Induction hobs function via electromagnetic induction, which requires a ferromagnetic material to react with the cooktop's alternating magnetic field and generate heat via eddy currents. SS 304 is austenitic and non-magnetic at room temperature, making it incapable of triggering induction sensors. SS 430 is ferritic, offering high magnetic permeability combined with excellent resistance to atmospheric corrosion and high thermal stability, making it the global standard for induction-compatible cookware bases.

Yes. Jagruti Steels is strictly a build-to-print OEM component manufacturer. We do not sell finished branded cookware in retail markets. All tooling, stamping dies, draw rings, and embossing blocks are designed, CNC-machined, and maintained in our private in-house toolroom according to your CAD files (.STEP / .IGES / .DWG) or physical samples.

Every export shipment includes comprehensive technical compliance paperwork: Mill Test Reports (MTRs) confirming chemical composition (Spectrometer certified) and mechanical properties, Certificate of Origin (COO), Commercial Invoice, Packing List, Dimensional Inspection Sheet, and exact HS Code classification (7220 9090 for circle blanks; 7326 9099 for stamped/drawn parts). Batch-level coil traceability is maintained for full audit compliance.

Because we operate production-scale power presses and hydraulic lines, MOQs are structured around raw metal coil minimum weights and die setup requirements rather than arbitrary piece counts. Initial prototype tooling and first-article qualification runs are supported for new program development. Typical production lead times range from 2 to 4 weeks following drawing approval. Dual production plants in Mumbai and Sarigam, Gujarat allow parallel production scheduling during seasonal peak periods.

We welcome plant visits and factory audits by buyer procurement teams, quality auditors, and third-party inspection agencies (such as SGS, Bureau Veritas, or Intertek). Both our Mumbai headquarters unit and our Sarigam, Gujarat plant (Mammal Industries) maintain open-door transparency for material traceability verification, tooling reviews, and live production walkthroughs.