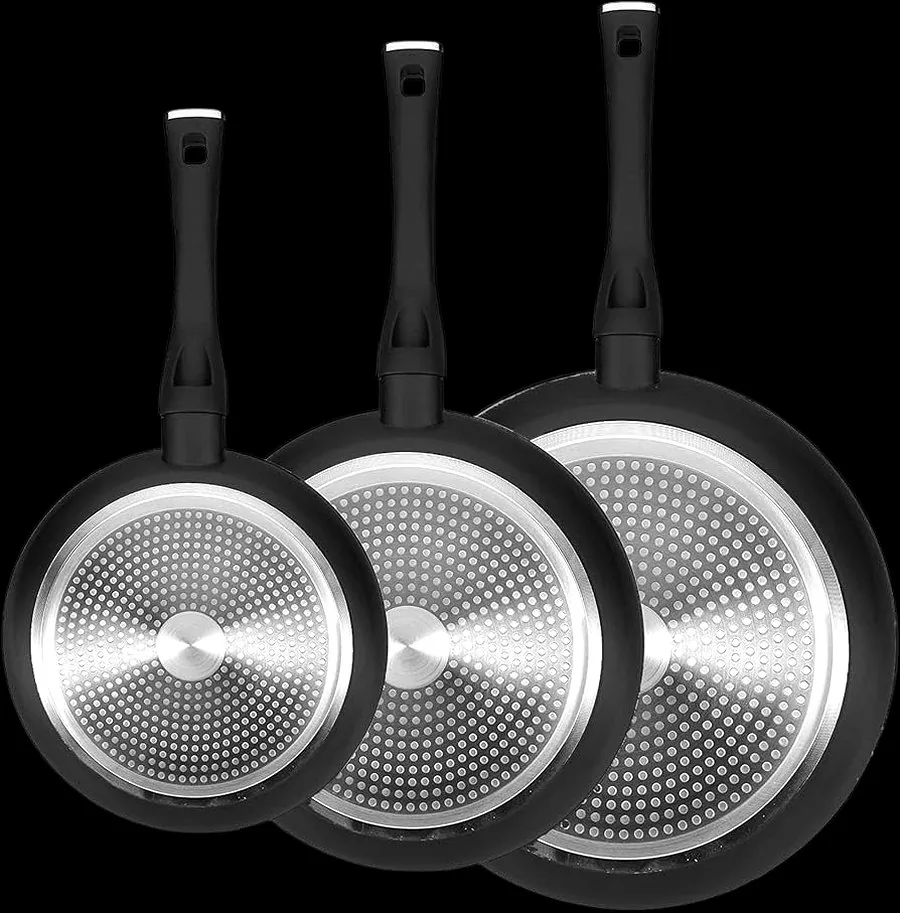
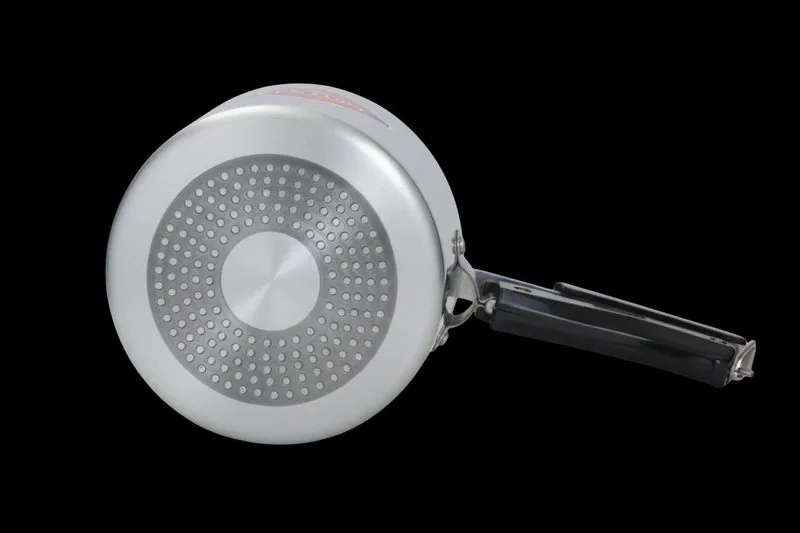
Non-stick fry pans fitted with SS 430 induction base plates manufactured by Jagruti Steels
SS 430 induction base plates bonded to non-stick pan bodies
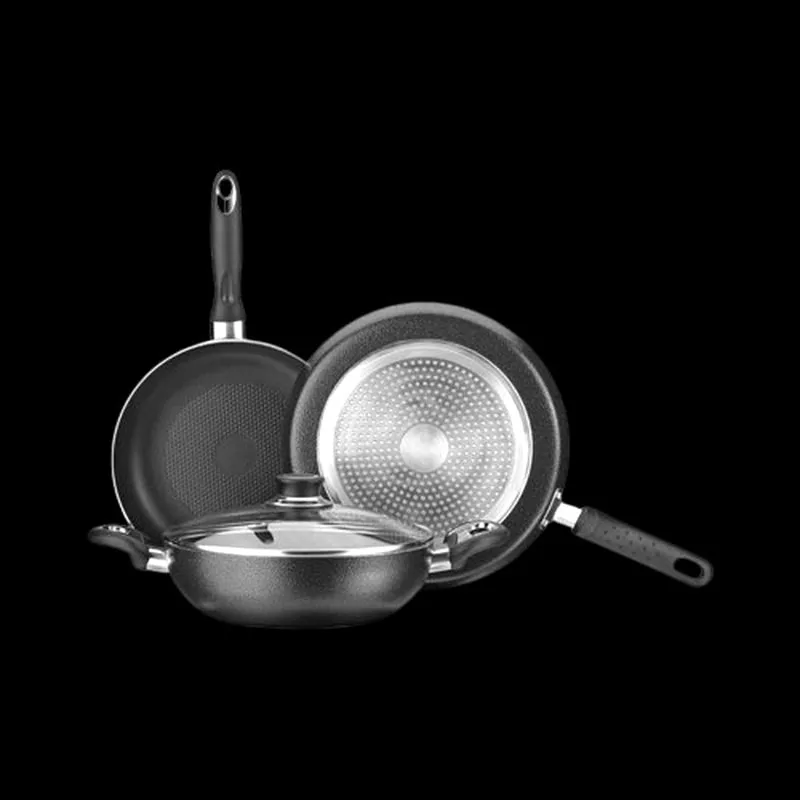
Aluminium pressure cooker body with stamped stainless steel induction base plate
Global B2B Sourcing Guide · OEM Pressing Since 1974

Engineering Precision Non-Stick Cookware Induction Plates: Metallurgy, Bonding Dynamics, and Global Sourcing Trends

High-permeability SS 430 (EN 1.4016) ferritic stainless steel induction base discs engineered for impact-bonding, friction welding, and thermal co-planarity in non-stick aluminium cookware. Manufactured to your custom engineering drawings in Mumbai & Sarigam, Gujarat.

Engineering Insights

Why SS 430 Non-Stick Cookware Induction Plates Decide Product Longevity

In modern non-stick cookware manufacturing, integrating an induction bottom is no longer just a visual feature—it is an intricate metallurgical challenge. Sourcing teams, appliance engineers, and private-label brand managers frequently encounter field failures such as pan warping, base delamination, uneven heating, and hob rejection. Understanding the physics of Non-Stick Cookware Induction Plates is critical to engineering cookware that survives rigorous thermal shocks and heavy commercial dishwasher usage.

01. METALLURGY

Ferromagnetic Permeability of SS 430

Unlike austenitic stainless steels (such as SS 304 or 316) which possess a face-centered cubic (FCC) crystal structure and are non-magnetic, SS 430 (EN 1.4016 / AISI 430) is a ferritic alloy with a body-centered cubic (BCC) structure. This crystal lattice grants SS 430 high magnetic permeability. When placed on an induction hob, the high-frequency alternating magnetic field seamlessly induces eddy currents and magnetic hysteresis within the SS 430 plate, instantly converting electrical energy into rapid, efficient thermal energy.
02. THERMAL DYNAMICS

Managing CTE Mismatch & Warping

Aluminium is the material of choice for non-stick cookware due to its high thermal conductivity (~237 W/m·K). However, Aluminium has a Coefficient of Thermal Expansion (CTE) of approximately 23 × 10-6 /K, whereas SS 430 has a CTE of roughly 10.4 × 10⁻⁶ /K. During intense heating and cooling cycles, this massive CTE mismatch generates extreme shear stress at the interface. Without engineered perforation patterns and controlled co-planarity tolerances, cookware bottoms buckle, bulge, or detach entirely.

03. BONDING INTEGRITY

Impact Bonding Mechanical Anchoring

During high-tonnage impact bonding (often executed at pressures exceeding 2,500 to 3,500 tons), the base of the forged or cast aluminium pan is forced into plastic deformation. The heated aluminium flows dynamically into the precision-punched holes and embossing grooves of the SS 430 induction plate. This mechanical anchoring mechanism forms a permanent, airtight interlock that prevents moisture ingress, corrosion, and acoustic vibration during induction operation.

Procurement Expertise Direct from the Press Floor

At Jagruti Steels Pvt. Ltd., our press operations have been refined over five decades since 1974. We produce high-precision SS 430 induction plates, engineered specifically to eliminate thermal fatigue and maximize electromagnetic induction efficiency. By utilizing prime coil sourced from accredited steel mills, every single disc conforms strictly to international EN 1.4016 and ASTM A240 standards, complete with batch-level chemical and mechanical certification.

Contact Us
Component Engineering

Recommended Non-Stick Cookware Induction Plates Solutions

Explore our OEM-grade induction base plate configurations designed for forged aluminium fry pans, die-cast saucepans, hard-anodized kadhai, and commercial cookware lines.

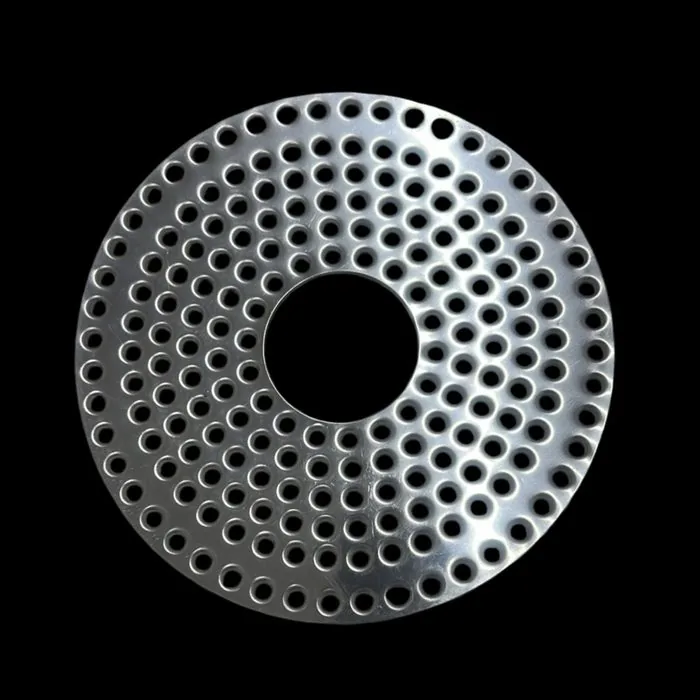
Standard Perforated SS 430 Induction Plates for Fry Pans
MODEL IP-STD-01

Standard Perforated Induction Discs

Engineered for high-volume non-stick aluminium cookware production. Features a balanced hole-to-surface open area ratio that optimizes heat transfer while allowing optimal aluminium flow during friction and impact bonding presses.

Diameters: 120mm – 220mm | Thickness: 0.4mm – 0.5mm | Grade: SS 430 EN 1.4016

Full-Cover Impact Bonding Base Discs
MODEL IP-FULL-02

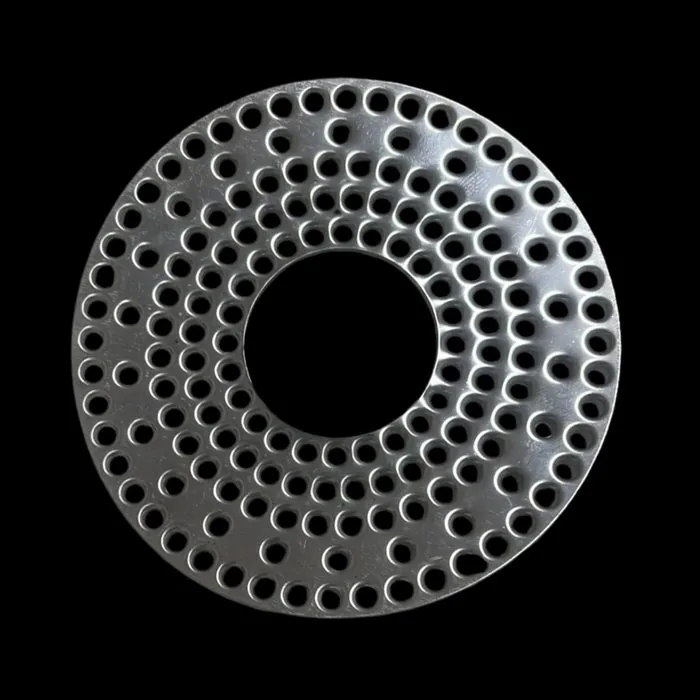
Full-Cover Rim-to-Rim Induction Base Plates

Designed for premium non-stick fry pans, tawas, and skillets. This design extends near the outer diameter edge, protecting the pan base against edge deformation and delivering edge-to-edge heat uniformity across all glass-top induction cooktops.

Diameters: 140mm – 240mm+ | Thickness: 0.5mm – 0.6mm | Edge chamfered

Heavy-Duty Pressure Cooker & Kadhai Induction Discs
MODEL IP-HD-03

Heavy-Duty Pressure Cooker Induction Discs

Built to endure thermal expansion forces and high internal pressure cycles (1.2 to 2.0 bar). Incorporates reinforced center alignment cutouts and heavy-gauge stamping to prevent pan bottom bowing under sustained heat.

Heavy Gauge 0.5mm – 0.6mm | Anti-Warp Structural Embossing | High Permeability

Deep Drawn Vessel Base Plates
MODEL IP-DD-04

Deep Drawn Vessel & Saucepan Induction Plates

Custom perforated blanks tailored for deep-drawn aluminium pots, stockpots, and milk pans. Formulated with controlled ductility to prevent micro-cracking during severe secondary forming or high-pressure press bonding.

Custom Blank Diameters | Deep-Draw Formable | Mill Certified SS 430 Coil

Precision Stamped Custom Embossed Base Plates
MODEL IP-OEM-05

Custom Embossed Brand Logo Base Plates

Integrate your brand identity directly onto the exterior induction base. Our in-house toolroom cuts custom embossing dies to press crisp brand logos, patent numbers, and heat distribution lines into the SS 430 disc during stamping.

Custom Toolroom Dies | OEM Logo Embossing | Proprietary Perforation Layouts

Multi-Cooker & Specialty Cookware Base Discs
MODEL IP-MC-06

Multi-Cooker & Electric Appliance Plates

SS 430 induction heating discs designed for electric non-stick multi-cookers, rice cookers, and heating plate assemblies. Optimized for precise thermistor fitment and uniform heat transfer to electric sensors.

Appliance Grade | Precise Tolerance Control | Electrical Appliance Compatible

Die Tooling Library

Perforation & Embossing Pattern Formats

Dynamic fluid flow during impact bonding depends directly on pattern geometry. Select from proven engineering patterns or cut custom dies in our in-house toolroom.

Concentric Circular Perforation Pattern 01
Pattern 01 · Concentric Radial125 · 140 · 165 · 180 mm
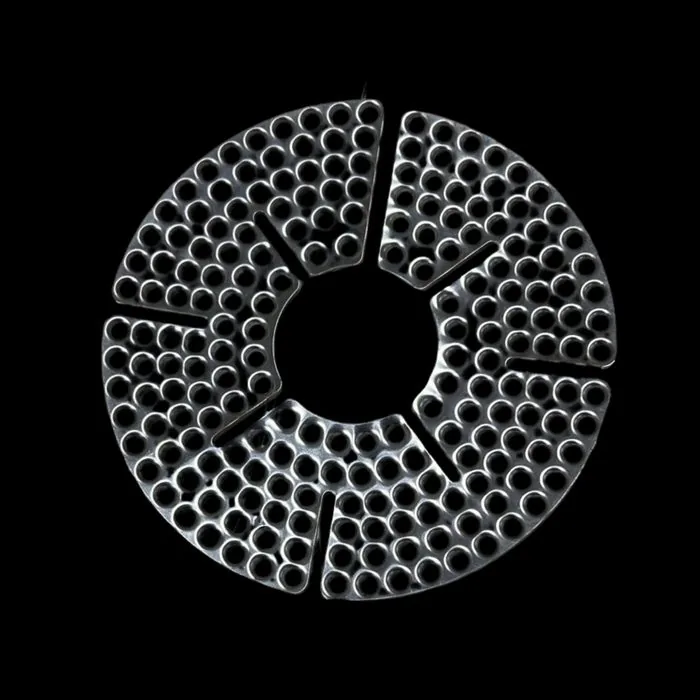
Hexagonal Honeycomb Matrix Pattern 02
Pattern 02 · Hexagonal Mesh125 · 140 · 165 · 180 mm
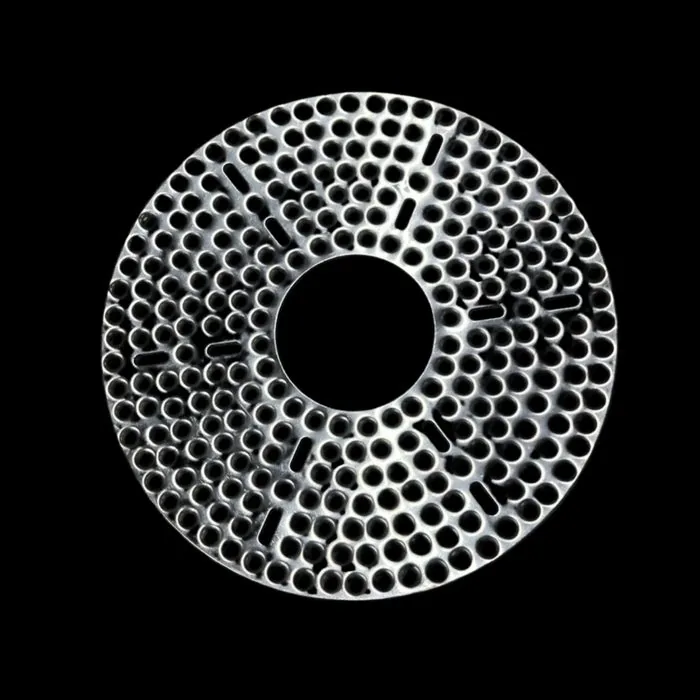
Starburst Anchor Perforation Pattern 03
Pattern 03 · Starburst Anchor100 – 190 mm range
Linear Slotted Perforation Pattern 04
Pattern 04 · Linear Thermal Slot100 – 190 mm range
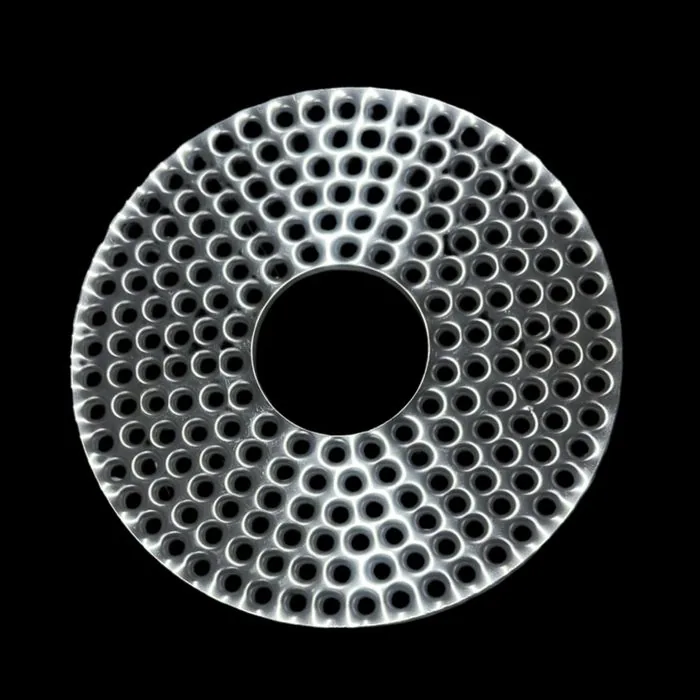
Dense Micro-Dot Perforation Pattern 05
Pattern 05 · Micro-Dot High Contact100 – 190 mm range
Proprietary OEM Pattern In-house CNC toolroom cuts custom tooling to your exact drawing. Submit Your Drawing →
Technical Comparison

Material Comparison Matrix: SS 430 vs SS 304 vs Mild Steel

Understanding the physical, chemical, and magnetic divergence between raw material grades used in cookware manufacturing.

Comprehensive technical specification table comparing SS 430, SS 304, and Mild Steel for cookware base plates
Engineering Parameter SS 430 (Ferritic Induction Grade) SS 304 (Austenitic Standard Grade) Mild Steel (Carbon Steel)
International Standards EN 1.4016 / AISI 430 / UNS S43000 EN 1.4301 / AISI 304 / UNS S30400 IS 2062 / ASTM A36 / Q235
Crystal Structure BCC (Body-Centered Cubic) FCC (Face-Centered Cubic) BCC (Body-Centered Cubic)
Ferromagnetic Response Strong (High Permeability μr > 500) Non-Magnetic (μr ≈ 1.02) Strong (μr > 1000)
Induction Hob Compatibility 100% Compatible (Instant Heating) Incompatible (Hob Rejection) Compatible (RUST PRONE)
Chemical Composition (Cr %) 16.0% – 18.0% Chromium 18.0% – 20.0% Chromium < 0.3% Chromium
Chemical Composition (Ni %) 0.0% – 0.75% (Nickel Free) 8.0% – 10.5% Nickel 0.0% Nickel
Atmospheric & Wash Corrosion High Corrosion Resistance Superior Corrosion Resistance Very Low (Severe Rusting)
Thermal Conductivity (20°C) ~26.0 W/m·K ~16.2 W/m·K ~50.0 W/m·K
Coefficient of Thermal Expansion ~10.4 × 10⁻⁶ /K (Close to Al balance) ~17.3 × 10⁻⁶ /K ~12.0 × 10⁻⁶ /K
Deep-Draw Stamping Formability Excellent (Yield Strength ≥ 260 MPa) Superior (Elongation ≥ 40%) Good (Prone to oxidized scale)

Crucial Takeaway for Sourcing Engineers

Attempting to use SS 304 for induction base plates results in catastrophic hob rejection—the induction cooktop's internal frequency sensor will detect no magnetic load and refuse to ignite. Conversely, using mild carbon steel creates severe rust stains under dishwasher exposure. SS 430 (EN 1.4016) remains the singular globally accepted standard for non-stick cookware induction bottom discs, combining optimal magnetic efficiency with long-term dishwasher rust immunity.

Why Leading Brands Choose Us

Jagruti Steels Pvt. Ltd. — 50 Years of Manufacturing Excellence

We operate strictly as a build-to-print B2B OEM component manufacturer. We never market finished cookware under our own name, guaranteeing zero brand conflict for our global clients.

0Years Pressing Steel
0State-of-the-Art Units
0Global Export Destinations
0Mill Test Traceability
0Brand Conflict (100% B2B)
Mumbai Facility · Headquarters

Jagruti Steels Pvt. Ltd.

Located in Mumbai’s industrial core, handling central engineering, master toolroom CNC milling, rapid sampling, buyer logistics, and high-speed precision stamping. Direct administration for international contracts. GSTIN: 27AAACJ9826****.

Sarigam Facility · Gujarat Unit

Mammal Industries

Our sister concern operating out of Sarigam, Gujarat (Manda Village). Dedicated to high-volume continuous coil blanking, heavy-tonnage hydraulic drawing, and multi-line progressive pressing for long-term export programs. GSTIN: 24AARFM9084****.

Integrated Global Network

Single Point of Accountable Supply

Both manufacturing facilities operate under unified Quality Assurance (QA) protocols. From tool steel selection to final export container stuffing, your procurement schedule is managed with single-source accountability.

Procurement FAQ

Frequently Asked Questions by Global Purchasing Officers

Clear, technical, and operational answers addressing the exact questions buyer teams ask during supplier evaluation.

Induction cooktop hobs generate high-frequency electromagnetic fields (typically 20 to 50 kHz). To convert this energy into thermal heat, the base material must exhibit strong ferromagnetic properties (high magnetic permeability). SS 430 features a ferritic body-centered cubic (BCC) crystal lattice that responds strongly to magnetic fields, creating resistive eddy currents and magnetic hysteresis that generate rapid heat.

SS 304, in contrast, is austenitic (face-centered cubic) and effectively non-magnetic. If a pan is built with an SS 304 base, the induction cooktop's electronic sensors will register no magnetic mass and automatically shut off. Furthermore, SS 430 matches the thermal expansion co-efficient required for impact bonding to die-cast and forged aluminium cookware, making it the globally accepted engineering standard.

During high-tonnage impact bonding (executed under 2,500+ tons of pressure), the heated aluminium vessel body undergoes plastic deformation. The softening aluminium flows directly into the precision-punched perforations and micro-grooves of the SS 430 induction plate, creating thousands of mechanical anchor locks.

Because Aluminium and Stainless Steel expand at different rates when heated (Aluminium CTE ~23×10-6/K vs SS 430 CTE ~10.4×10⁻⁶/K), a solid non-perforated disc would shear off or bow outward. The perforated pattern acts as a stress-relief matrix, absorbing mechanical shear during thermal shock and preventing bottom warping, bulging, or base separation over years of daily cooking.

Yes. Jagruti Steels operates as a full build-to-print OEM partner. We do not restrict buyers to standard catalogue items. All progressive stamping dies, blanking tools, and embossing punches are designed in 3D CAD/CAM and cut in our in-house CNC toolroom.

You can define the exact outer diameter (from 100 mm to over 240 mm), sheet gauge (0.4 mm, 0.5 mm, 0.6 mm), hole diameter, open-area ratio, perimeter chamfering, and brand logo embossing. We also work from physical samples provided by prospective clients.

Quality reliability is central to our E-E-A-T commitment. Every production run of SS 430 induction base plates is matched to traceable coil master batches. Upon dispatch, we provide official Mill Test Reports (MTRs) detailing exact chemical spectroscopy (Chromium %, Carbon %, Manganese %, Silicon %, Phosphorus %, Sulfur %) and mechanical yield strength testing.

For international customs compliance, every shipment includes a Certificate of Origin (COO), Packing List, Commercial Invoice, and precise Harmonized System tariff codes (HS Code 7220 9090 for circle blanks, HS Code 7326 9099 for finished stamped components).

MOQ is structured around geometry, raw material coil width, and tooling status rather than an arbitrary figure. For existing tooling patterns, pilot qualification runs are supported; for custom OEM dies, MOQs are aligned with standard coil slit volumes. Lead times for first-article tooling and initial samples typically range from 10 to 18 business days.

Our primary plant in Mumbai is located just 35 km from Jawaharlal Nehru Port Trust (JNPT / Nhava Sheva Port), enabling direct ocean container shipping to major ports in Europe, Turkey, Vietnam, the Middle East, and North America. We support FOB, CIF, CFR, and buyer-nominated freight forwarders.

We maintain an absolute B2B component focus. Jagruti Steels Pvt. Ltd. does not manufacture finished cookware, nor do we operate any direct-to-consumer retail brand. Your custom tooling is catalogued, stored securely in our toolroom, and reserved exclusively for your production contracts.

Our name never appears on your packaging, shipping cartons, or finished product. We routinely sign Non-Disclosure Agreements (NDAs) with global cookware brands to safeguard proprietary pan geometry and industrial designs.

Direct Factory Procurement

Partner with India's Premier SS 430 Induction Base Plate Manufacturer

Send us your technical drawings, target specifications, or sample requests today. Our engineering team responds within 2 business hours (IST) with technical feasibility assessment and factory pricing.

Contact Us Download Technical Datasheet