
01
Strict Tooling Tolerances
In-house progressive and hydraulic press tooling eliminates rim ovality, ensuring airtight gasket seating and smooth lid-locking rotation every single time.
Zero Rim Distortion · Consistent Pitch
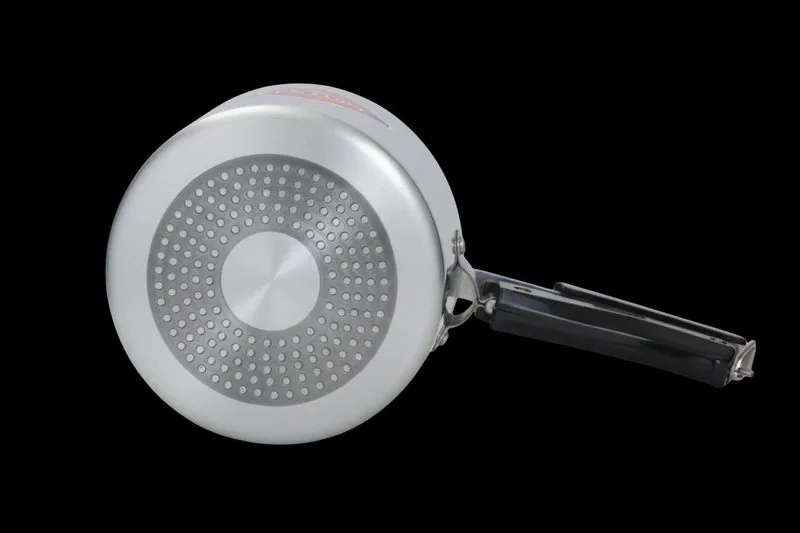
Precision-stamped lids, gasket support rings, sealing collars, and deep-drawn pressure bodies engineered to drawing in SS 304 and SS 430 for global cookware brands.
Pressure cookers operate under continuous thermal shock and internal working pressure (1.0 to 2.0 bar). Component failure is never cosmetic—it affects sealing integrity and structural safety. Jagruti Steels produces custom pressure cooker stampings backed by 50 years of metal-forming expertise, serving Tier-1 cookware brands across India, Europe, Turkey, Vietnam, and the Middle East.
In-house progressive and hydraulic press tooling eliminates rim ovality, ensuring airtight gasket seating and smooth lid-locking rotation every single time.
Zero Rim Distortion · Consistent Pitch
We source prime, certified SS 304 and SS 430 coil exclusively from prime mills. Every production lot includes full chemical and mechanical Mill Test Reports (EN 10204 3.1).
100% Tested Coil · Certified Food Grade
Dual production units in Mumbai, Maharashtra and Sarigam, Gujarat allow parallel production scheduling for large seasonal retail rollouts and contract buyer orders.
Dual Plant Operations · High Capacity
Every part is manufactured strictly to buyer technical specifications, 3D models, or physical samples. We supply unbranded OEM parts to protect your brand identity.
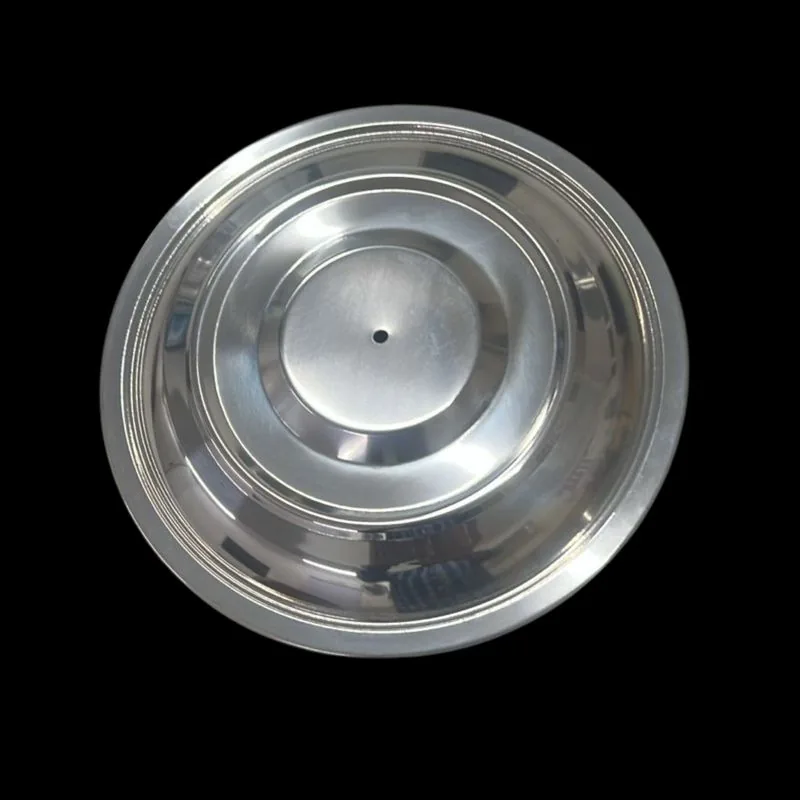
Deep-drawn and stamped lids in SS 304 or SS 430. Custom locking lug spacing, precise center hole punching for steam vent tubes, and formed safety valve recesses.
SS 304 / SS 430 · Flat or Dome · Polished Finish
Precision-rolled profile rings engineered to maintain uniform radial pressure on rubber/silicone gaskets, preventing pressure leakage under prolonged cooking cycles.
Tight Diameter Tolerance · Bur-Free Edge
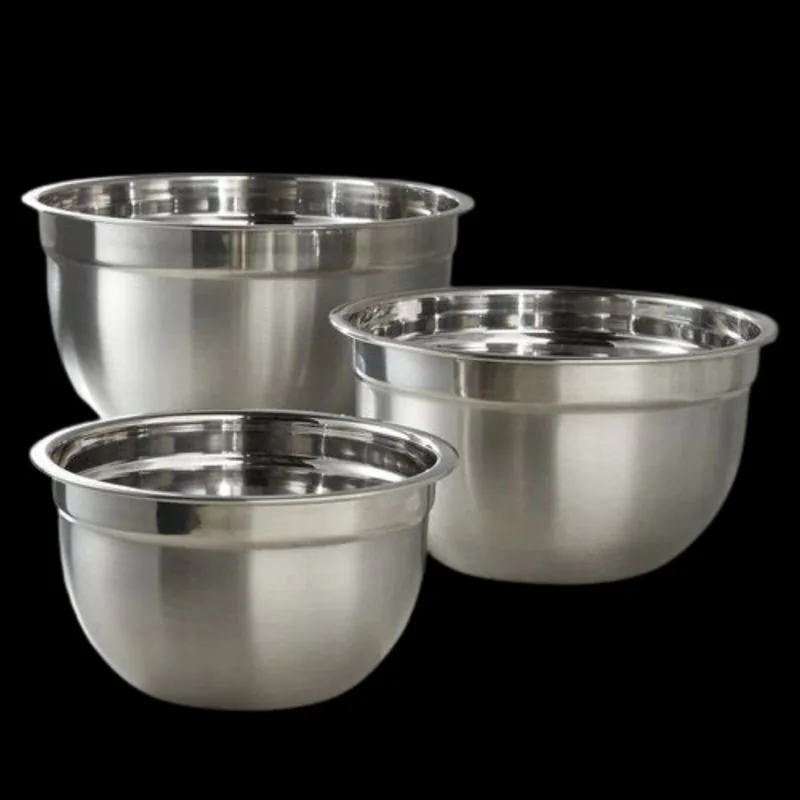
Seamless vessel bodies formed on multi-stage hydraulic press lines. Optimized wall-thickness distribution prevents fatigue under cyclic pressurization.
High Draw Ratio · Uniform Wall Thickness
Structural rim rings stamped from heavy-gauge stainless steel to reinforce outer-fitting lid perimeters against deformation during transit and daily handling.
Heavy Gauge · High Tensile Strength
Custom-punched stainless steel plates designed to securely fasten bakelite handles, side ears, and counter-handles to pressure cooker bodies and lids.
Custom Hole Pattern · Embossed Indexing
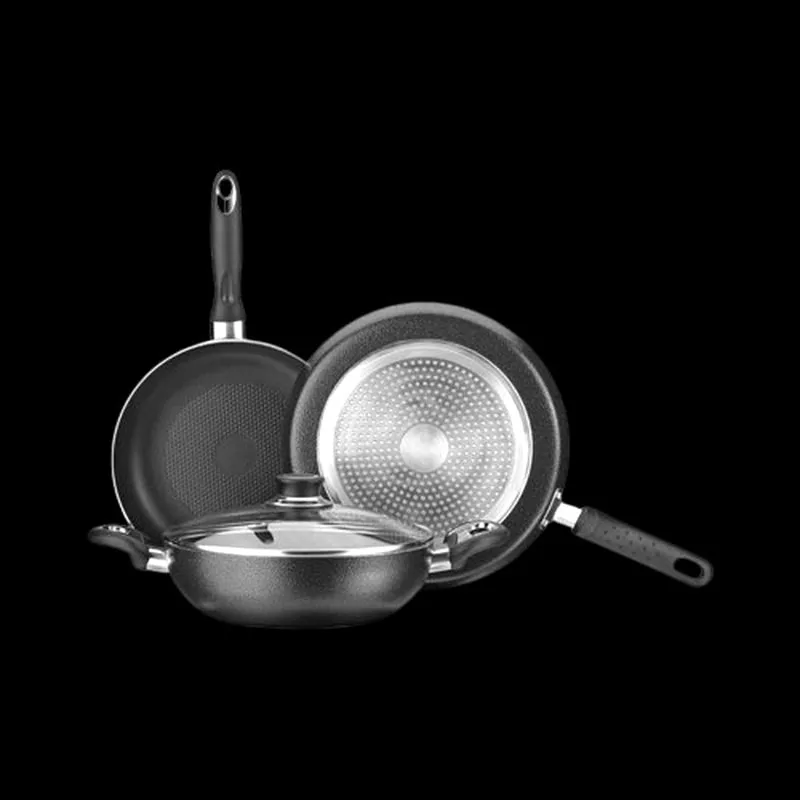
Perforated and embossed SS 430 discs designed for impact-bonding to aluminum pressure cooker bases, enabling rapid induction heating efficiency.
EN 1.4016 · Custom Embossing · Impact Ready
Matching the correct steel chemistry to the structural function ensures long-term reliability and compliance with international food-contact laws.
| Component Application | Recommended Grade | Key Mechanical Property | Primary Technical Benefit |
|---|---|---|---|
| Cooker Lids & Steam Inserts | SS 304 (EN 1.4301) | Elongation ≥ 40% | High corrosion resistance, deep-draw ductility, non-reactive food contact. |
| Induction Base Plates | SS 430 (EN 1.4016) | High Ferromagnetic Response | Enables magnetic coil coupling on induction hobs for aluminum cooker bodies. |
| Gasket Support Rings | SS 304 / SS 430 | Yield Strength ≥ 250 MPa | Dimensional stability under spring tension; resists steam degradation. |
| Reinforcement Brackets | SS 430 / Mild Steel | High Tensile Load Capacity | Prevents mechanical flex at handle fastening and hinge points. |
Our structured quality gate system ensures zero dimensional deviation between approved prototype and container-load shipments.
Our engineers evaluate your 2D/3D CAD drawings, material specs, and draw ratio to optimize press tool layout and minimize material yield scrap.
Dies, punches, and trimming tools are cut in our Mumbai facility, ensuring total IP protection and fast iteration without reliance on third-party toolmakers.
We supply sample batches along with full CMM dimensional inspection reports and raw material Mill Test Certificates for buyer laboratory sign-off.
Controlled power press production with inline gauge checks, protective export packaging, and freight consolidation via Mumbai's JNPT seaport.
We simplify global sourcing with transparent documentation, reliable lead times, and flexible shipping options tailored to overseas buyers.
Raw coil is sourced against strict metallurgical parameters. Batch numbers are linked from raw coil reception through to final component packing.
Shipments arrive complete with Certificate of Origin, Form A/FTA documentation where applicable, commercial packing lists, and correct HS codes.
Located 35 km from Jawaharlal Nehru Port Trust (JNPT, Nhava Sheva), enabling rapid container stuffing and reliable ocean freight vessel schedules.
Answers to common questions from sourcing managers, quality auditors, and product engineers.
Pressure cooker lids and food-contact sealing surfaces are primarily manufactured from austenitic SS 304 (EN 1.4301) due to its high corrosion resistance, ductility, and food-contact safety compliance. Support rings, reinforcement collars, and induction-ready cooker base discs are stamped from ferritic SS 430 (EN 1.4016) or high-tensile structural grades specified by the buyer.
Yes. We operate a full in-house press toolroom where dies and punches are designed and cut to match your exact lid diameter, locking lug geometry, steam vent interface, gasket groove profile, and handle bracket mount points.
We supply precision components manufactured under strict dimensional tolerances and material certification (EN 10204 3.1 Mill Test Reports). Our press tooling maintains uniform wall thickness and structural stability required to pass pressure retention, burst, and thermal deformation tests specified by IS 2347, EN 12778, and global quality audits.
All export consignments include Mill Test Certificates (MTRs), Certificate of Origin, Commercial Invoice, Packing List, and customs HS code documentation (HS 7326 9099 for finished stampings). Direct container loading is available from our Mumbai plant, located 35 km from JNPT Port.
New press tool development and first-article sample production typically take between 2 to 4 weeks depending on part geometry and drawing complexity. Once sample sign-off is achieved, volume production cycles run on standard 15-to-25-day delivery windows.
Send your component drawing, CAD file, or target material specifications to our OEM engineering team in Mumbai for a comprehensive feasibility evaluation.