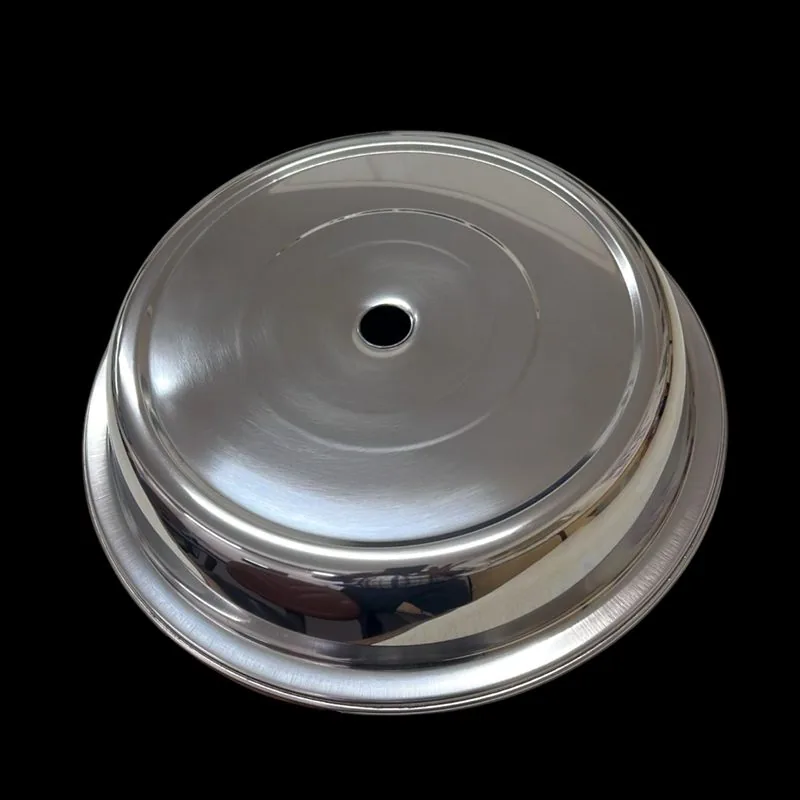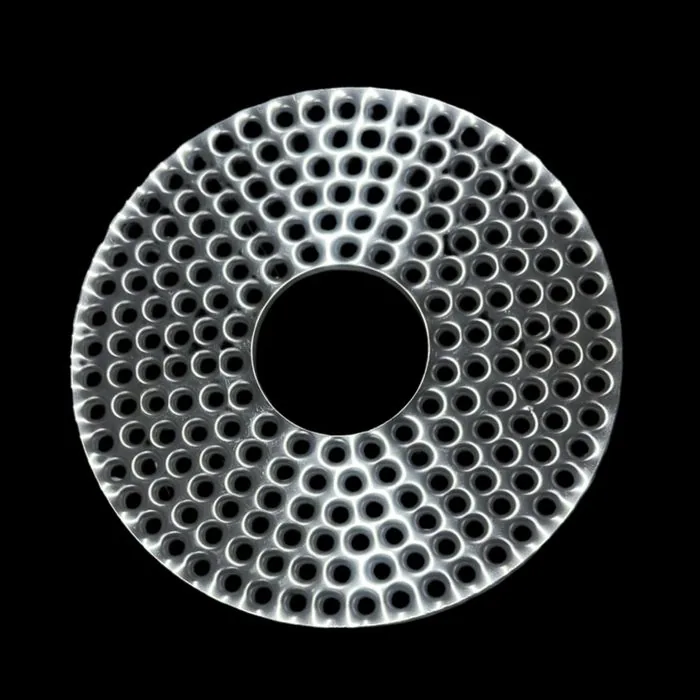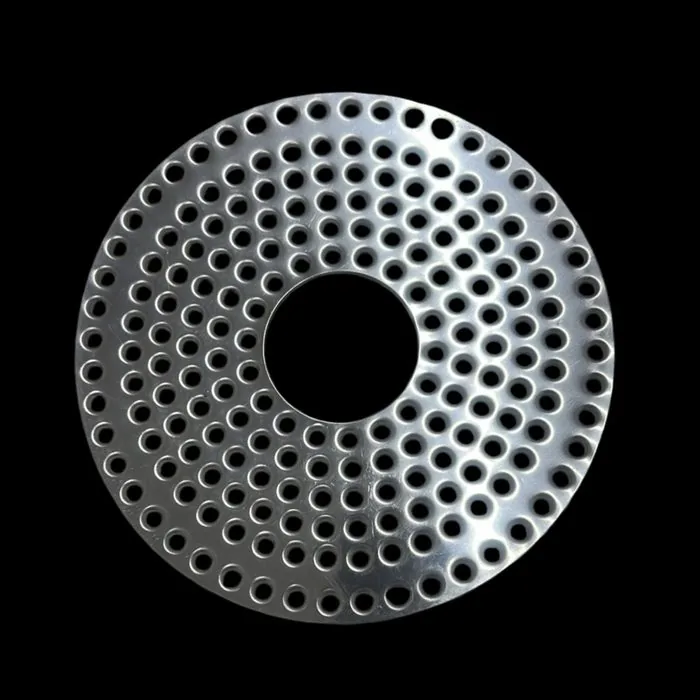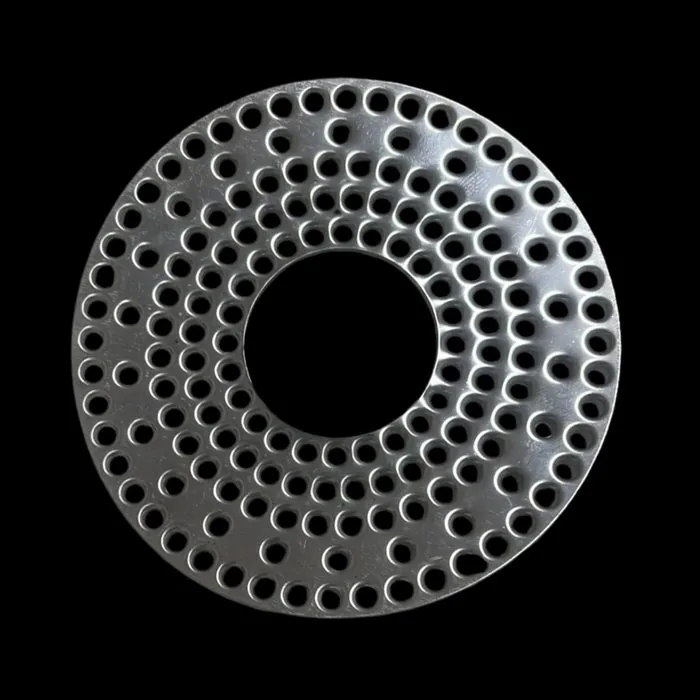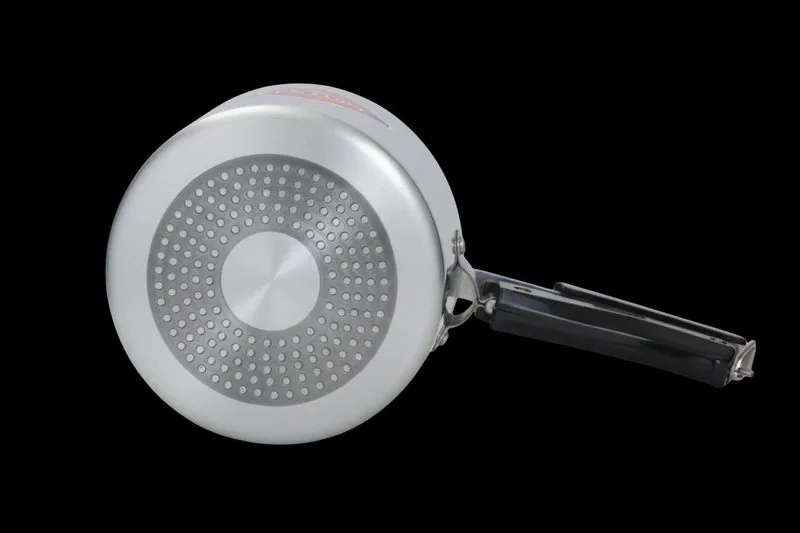
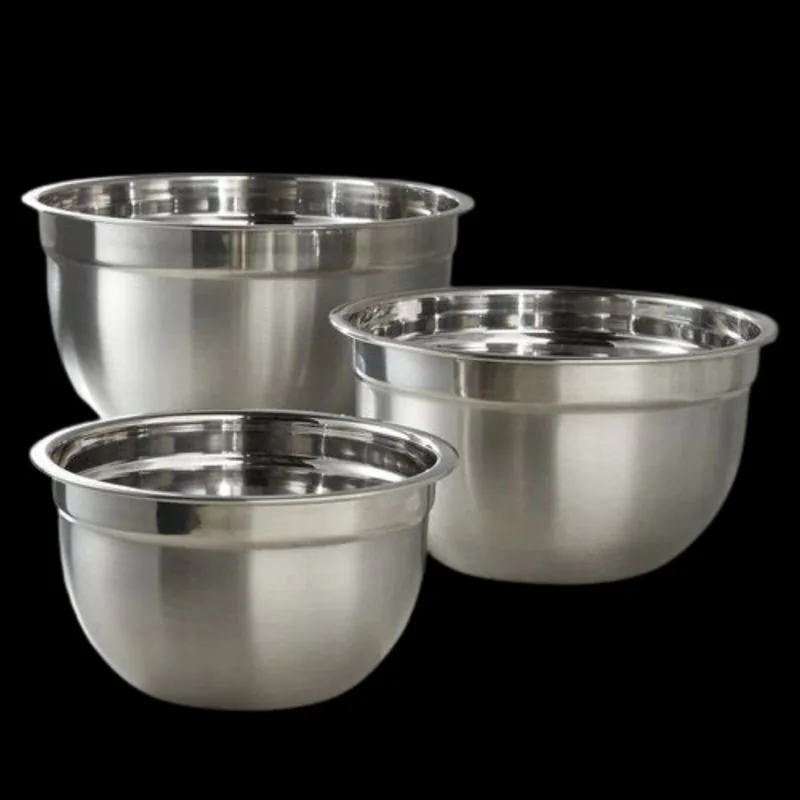
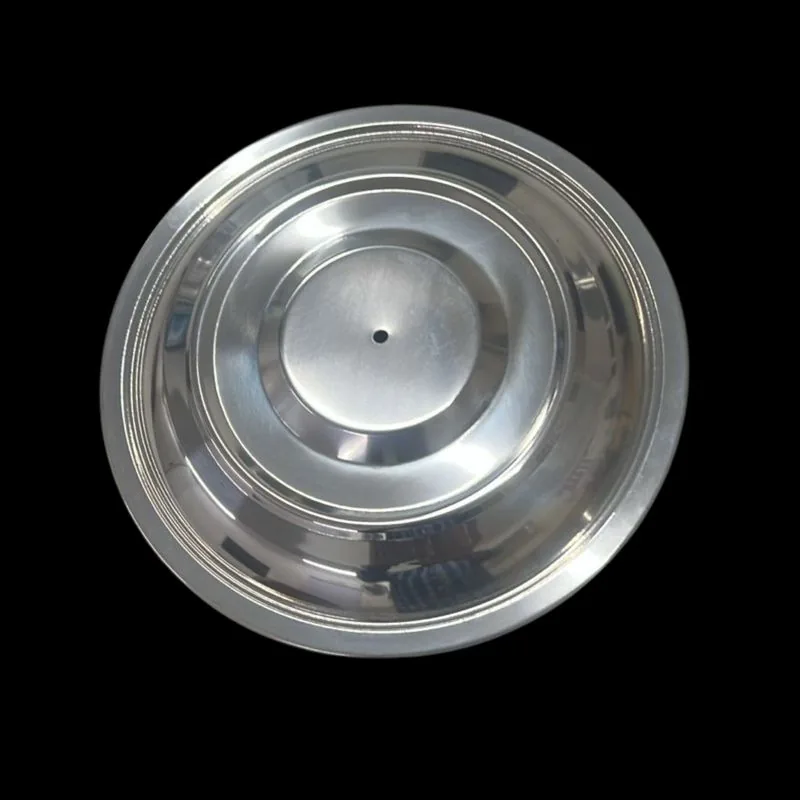
Precision stamped stainless steel pressure cooker lid manufactured by Jagruti Steels
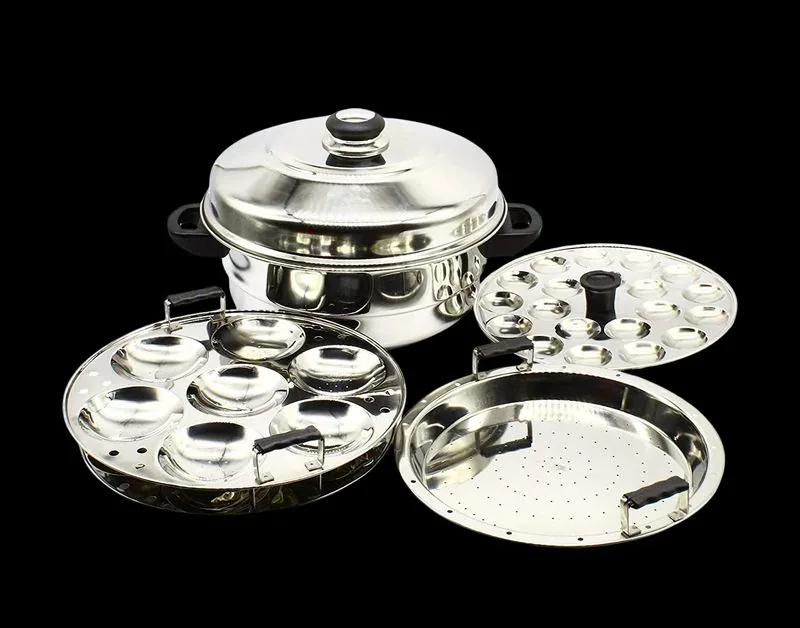
Aluminium and stainless steel pressure cooker assembly showing precision lid dynamic fit
Deep drawn stainless steel vessel components and lids engineered in Mumbai plant
Engineering Authority · OEM Manufacturing Since 1974

OEM Pressure Cooker Lids & Support Rings: Global Procurement & Technical Manual

High-precision SS 304 & SS 430 deep-drawn pressure cooker lids, gasket support rings, and safety seating components — engineered to zero-defect tolerances for leading appliance brands across Europe, Middle East, Asia, and the Americas.

  • Material GradesSS 304 · SS 430 · Tri-Ply
  • Lid Diameters140 mm – 320 mm+
  • Gauge Range0.6 mm – 1.2 mm
  • Pressure Tolerance1.2 to 2.0 Bar
Strategic Sourcing Guide

The Physics of Pressure Containment: Why Precision Lids & Support Rings Determine Brand Integrity

In high-pressure cooking appliances, the closure mechanism is the primary failure surface. Precision deep-drawing, stress distribution, and rim parallelism govern whether a pressure cooker passes global safety compliance or suffers structural fatigue.

CRITICAL ANALYSIS

Semantic Intent & Engineering Demand in Modern Sourcing

Global procurement teams searching for Pressure Cooker Lids & Support Rings do not merely buy stamped metal discs — they invest in systemic containment safety, hermetic sealing reliability, and fatigue-resistant ergonomics. A pressure cooker operates under cyclic internal thermal expansion, enduring working hydrostatic pressures between 80 kPa and 150 kPa (1.2 to 2.0 bar). Under these extreme cyclic loads, micro-deficiencies in rim gauge or uneven support ring spring tension result in gasket blowout, steam blow-by, and field warranty claims.

At Jagruti Steels Pvt. Ltd., we bridge metallurgical science with high-tonnage progressive press operations. Having supplied OEM pressure cooker parts since 1974, our dual facilities in Mumbai and Sarigam, Gujarat produce build-to-print lids and support rings that maintain absolute structural concentricity under high pressure cycles, protecting your consumer reputation worldwide.

Precision stamped pressure cooker lid with smooth rim profile
Precision Stamped Lid
Cooker assembly with custom fitted pressure cooker lid and gasket ring
Fitted Assembly
Deep drawn stainless steel components manufactured in Mumbai
Deep-Drawn Geometry
Product Catalog & Technical Lineup

OEM Product Recommendations: Pressure Cooker Lids & Support Rings

Engineered to exact buyer blueprints. We manufacture outer-lid systems, inner-lid systems, gasket support rings, and multi-cooker locking mechanisms with certified stainless steel alloys.

SS 304 Outer-Lid Dome Cover for Commercial Pressure Cookers
RECOMMENDED LINE 01

Outer-Lid Bayonet Dome Covers

Deep-drawn from premium SS 304 (EN 1.4301), designed for bayonet-style external locking pressure cookers. Features precision stamped lug recesses, anti-bulge structural crowns, and multi-port punches for vent tubes and safety valves.

SS 304 · Gauge 0.8–1.2 mm · Zero-warp Crown

View Technical Specs →
Inner-Lid Stainless Steel Pressure Cooker Lid Assembly
RECOMMENDED LINE 02

Inner-Lid Self-Sealing Flexible Covers

Specifically engineered for traditional inner-sealing pressure cookers where spring elasticity and edge perimeter geometry dictate safety. Formed with controlled spring-back temper to ensure effortless insertion and leak-proof internal seating.

High-Tensile SS 304 · Controlled Temper · Inner Sealing

Explore Inner-Lid Variants →
Precision Gasket Support Rings & Retaining Assemblies
RECOMMENDED LINE 03

Precision Gasket Support Rings

Stamped support and retaining rings designed to lock food-grade silicone or rubber gaskets tightly against the lid wall. Engineered with continuous uniform curvature to eliminate gasket twisting, roll-out, and lateral vapor bleed.

SS 304 / SS 430 · Rolled Rim · Burr-Free Edge

Custom Ring Dimensions →
Induction Encapsulated Multi-Layer Pressure Cooker Lids
RECOMMENDED LINE 04

SS 430 Magnetic Base & Cap Rings

Ferritic SS 430 (EN 1.4016) component rings for modern hybrid pressure cookers and induction multi-cooker tops. Delivers magnetic responsiveness required for smart top-heating sensor arrays while offering superior mechanical rigidity.

Ferritic SS 430 · Magnetic Permeability · EN 1.4016

SS 430 Data Sheet →
Multi-Cooker Steamer Inserts and Lid System Assemblies
RECOMMENDED LINE 05

Multi-Cooker Interlocking Rim Assemblies

Complex stamped rims and support components designed for modern electric pressure cookers and instant multi-cookers. Integrates twist-lock alignment tabs, seal seats, and steam release channel collars.

Complex Stamping · Multi-Stage Tooling · Tight Tolerance

Multi-Cooker Parts →
Commercial Duty Stainless Steel Pressure Cooker Heavy Lids
RECOMMENDED LINE 06

Commercial Heavy-Duty Pressure Lids

Heavy-gauge (1.2 mm to 1.5 mm) deep-drawn lids for institutional, hotel, and restaurant pressure cookers ranging from 10L to 40L capacity. Designed for extreme pressure cycling and aggressive commercial scrubbing.

SS 304 · 1.2–1.5 mm Gauge · Commercial Grade

Hospitality Range →
Information Gain & Material Intelligence

Metallurgical Analysis: SS 304 vs SS 430 vs Substandard SS 201 in Pressure Containment

Choosing the right material grade directly impacts burst pressure margin, intergranular corrosion resistance, and compliance with global food-contact directives (FDA, LFGB, EU 1935/2004).

Metallurgical Property Comparison for Pressure Cooker Lids & Support Rings
Property / Specification SS 304 (EN 1.4301) — Recommended for Lids SS 430 (EN 1.4016) — Recommended for Rings Substandard SS 201 (High Mn) — Avoid
Chemical Structure 18% Cr / 8% Ni (Austenitic) 16-18% Cr / 0% Ni (Ferritic) 13-15% Cr / 1% Ni / 5.5-7.5% Mn
Corrosion Resistance (Acidic Steam) Exceptional (Pitting Resistance Equivalent > 18) Moderate to High (Good in dry/mild steam) Poor (Prone to rust at weld/punched ports)
Cyclic Pressure Fatigue Limit High (> 50,000 pressure cycles) Moderate (> 30,000 pressure cycles) Low (Work-hardens quickly; micro-cracks)
Deep-Drawing Ratio (L/D) Superior (Allows deep dome draws without thinning) Good (Ideal for ring stamping & moderate draws) Poor (Requires multiple intermediate anneals)
Magnetic Permeability Non-Magnetic (Ideal for main body covers) Ferromagnetic (Ideal for induction top sensors) Slightly Magnetic (Inconsistent permeability)
Food Contact Safety (LFGB/FDA) 100% Certified Food Grade 100% Certified Food Grade Risk of Heavy Metal / Manganese Leaching

Engineering Warning on Material Thinning During Deep Draw

When drawing a pressure cooker lid from a flat circular blank, the material at the apex of the dome can thin by up to 18-22% if die clearances and blank-holder hydraulic pressure are not calibrated perfectly. Substandard SS 201 work-hardens rapidly under deep draw, creating localized strain hardening and invisible micro-fissures around safety valve ports. Jagruti Steels utilizes certified 304 and 430 prime coil with guaranteed elongation (>40% for SS 304) to ensure uniform wall thickness across every deep-drawn contour.

Contact Us
Why Jagruti Steels

50+ Years of Manufacturing Mastery: Built for Global OEM Brands

We do not market finished consumer cookware under our own name — we dedicate 100% of our production capacity and toolroom engineering to private-label and OEM partners worldwide.

Dual Manufacturing Infrastructure

Two specialized plants in Mumbai (Maharashtra) and Sarigam (Gujarat) offer redundant production lines, ensuring zero supply disruption even during peak international sourcing seasons.

In-House Tooling & Die Making

From 3D CAD modeling to CNC die machining, our toolroom builds progressive drawing and blanking dies in-house, significantly lowering NDT development costs and tooling lead times.

Rigorous Quality & Burst Testing

Every lid design undergoes dimensional CMM checks, rim flatness laser scanning, and hydrostatic burst testing up to 5.0 bar to ensure safety margins far exceed standard working pressure.

100% IP Protection & Confidentiality

Your custom lid geometries, lug designs, and tooling remain 100% proprietary under formal non-disclosure agreements (NDAs). We never re-use buyer dies for competing brands.

Plant Capabilities
  • Hydraulic Deep Draw Presses — Up to 500-ton capacity for seamless dome forming
  • Progressive Blanking Presses — High-speed circle cutting & support ring stamping
  • Surface Finishing — Automatic mirror polishing, satin brushed, or electropolished finish
  • Secondary Operations — Multi-boss punching, vent tube welding, rim curling
Export & Logistics Assurance
  • Location: Mumbai & Sarigam (35 km to JNPT Port, Mumbai)
  • Documentation: MTR EN 10204 3.1, Form A, Certificate of Origin
  • Packaging: VCI anti-rust wrapping, custom export palletization
Procurement Intelligence

Frequently Asked Questions: Sourcing Pressure Cooker Lids & Support Rings

Addressing key technical, metallurgical, quality assurance, and commercial queries raised by global sourcing directors and engineering teams.

Steam tightness is primarily controlled by three critical engineering parameters: flat seat parallelism across the perimeter sealing flange, gasket canal radius consistency, and thermal expansion matching between the support ring and the lid body. At Jagruti Steels, our deep-draw dies maintain concentricity within ±0.08 mm, preventing gasket distortion or micro-channel steam leaks under 1.2 to 2.0 bar operating pressure.

SS 304 (EN 1.4301) contains 18% Chromium and 8% Nickel, providing superior intergranular corrosion resistance against high-temperature organic acid vapors released during cooking. SS 201 relies on manganese substitution, making it prone to stress corrosion cracking under cyclical hydrostatic pressure and acidic attack, leading to structural fatigue over time.

We custom-tool support rings based on exact bayonet lug placement and rim rolled geometries specified in buyer technical drawings. Using progressive press tooling, we eliminate burrs and achieve precise tension fit for rubber or silicone gaskets, ensuring seamless locking for both inner-sealing and outer-sealing pressure cookers.

Yes. Our in-house toolroom designs dual-action punching and embossing dies that stamp buyer logos, safety valve ports, vent tube bosses, and pressure indicator recesses in a single automated press stroke, ensuring 100% position accuracy across high-volume production runs.

Every shipment of Pressure Cooker Lids & Support Rings includes EN 10204 Type 3.1 Mill Test Certificates (MTR) detailing chemical analysis and mechanical testing, Certificate of Origin, commercial packing slip, and correct HS tariff classification (7326 9099 for stamped components).

Tooling development and initial first-article sample inspection reports (FAIR) are completed within 15 to 21 working days from drawing sign-off. Once samples are approved, standard mass production lead times range from 3 to 4 weeks depending on batch volume and surface finish requirements.

Our quality management system enforces statistical process control (SPC) at every stage: incoming raw material coil spectroscopy, hourly dimensional checking of drawn profiles, 100% visual inspection of gasket tracks, and batch hydrostatic burst testing up to failure threshold.

Start Your OEM Partnership

Ready to Engineer Precision Pressure Cooker Lids & Support Rings?

Send us your CAD drawings, 3D models, or physical samples. Our senior engineering team will evaluate draw ratios, material selection, and provide a competitive OEM quotation within 24 hours.

Contact Us