Explore our core export-grade deep-drawn inner vessels, induction base discs, and industrial rotary shearing equipment engineered for commercial kitchenware manufacturers and appliance OEMs.
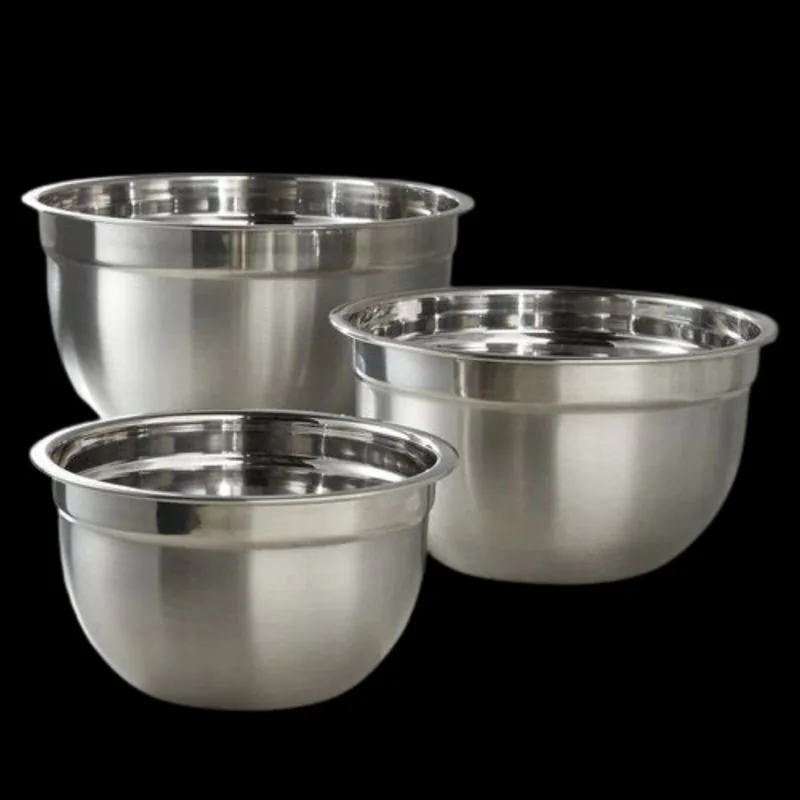
Seamlessly deep-drawn inner pot liners tailored for high-pressure electric multi-cookers and rice cookers. Features uniform wall thickness, mirror finish, and crack-resistant radii.
Contact Us
Precision-stamped SS 430 magnetic stainless steel discs engineered for thermal impact bonding onto aluminium or multi-ply inner pot bottoms for commercial NY kitchens.
Contact Us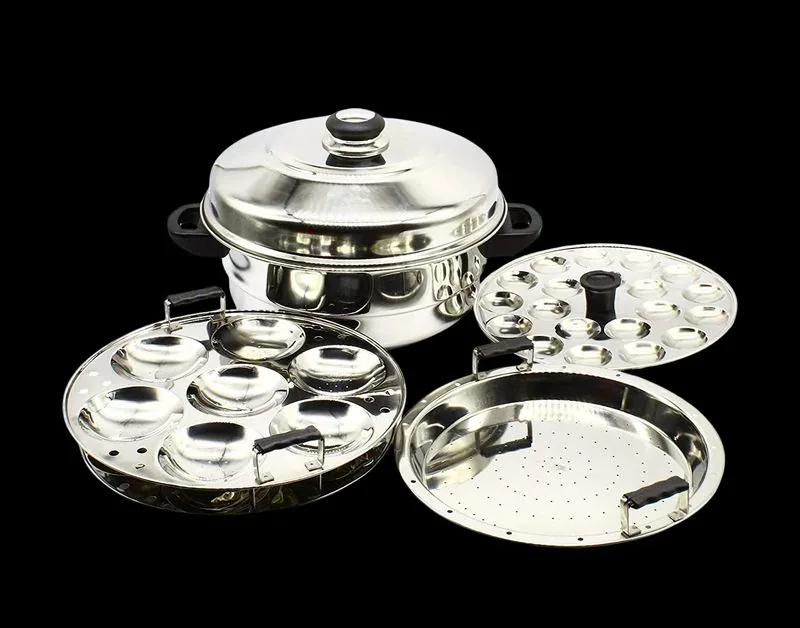
Custom perforated food-grade stainless steel inserts designed for multi-tier cooking in commercial rice cauldrons and institutional steam pots.
Contact Us
Precision rotary slitting knives and circular trimming blades designed for automated sheet metal trimming during deep-drawn inner pot rim fabrication.
Contact Us
Industrial punch press tooling and precision circle die components for high-speed cutting of stainless steel circles used in inner pot manufacturing.
Contact Us
Ultra-thin hot pressed diamond cutting saw blades engineered for high-precision edge deburring, ceramic coating scoring, and rim finishing on commercial inner pots.
Contact Us
Factory-grade motorized round circle cutting machine for shearing metal blanks into precise circular discs prior to deep draw inner pot pressing.
Contact Us
High-speed diamond grooving discs used for preparing thermal contact channels and bonding surfaces on heavy industrial inner pot bases.
Contact UsThe global commercial food service sector and home appliance market in New York demand exceptional reliability, structural integrity, and rigorous hygiene compliance from cookware components. As a premier OEM manufacturer with over five decades of metal stamping, deep-drawing, and metallurgical expertise, Jagruti Steels Pvt. Ltd. provides a critical bridge between international material excellence and the precise engineering requirements of North American distributors, appliance brands, and commercial kitchen suppliers.
Information Gain Insight: Unlike standard superficial trading suppliers, true factory-direct OEM manufacturing of inner pots requires precise metallurgical control over grain size (ASTM 7 to 8), yield strength, and deep-drawing anisotropy (r-value > 1.2). This prevents micro-fissuring, thinning, and thermal warping during high-temperature pressure cooking cycles in high-turnover NYC commercial kitchens.
When engineering inner pots for electric multi-cookers, rice cookers, and commercial soup kettles, material selection directly governs heat distribution, corrosion resistance, and induction hob responsiveness. We specialize in three core material configurations:
Deep drawing an inner pot involves drawing a flat sheet metal blank into a cylindrical hollow body using multi-tonnage hydraulic presses without thinning or tearing the metal. Our manufacturing process maintains strict control over three key mechanical parameters:
First, the Limiting Draw Ratio (LDR) is carefully calculated based on blank diameter versus punch diameter. For deep vessel pots, multi-stage sequential drawing with intermediate stress-relieving annealing is utilized to eliminate work-hardening brittleness. Second, Die Radius & Clearance Calibration is maintained within ±0.03 mm to ensure that corner radii do not experience excessive localized stress, preventing wall collapse under internal steam pressure (up to 2.0 bar in commercial cookers). Third, automated lubricants are applied uniformly to maintain surface smoothness, eliminating microscopic drag lines that could trap bacteria or compromise non-stick coatings.
From high-volume commercial kitchens in Manhattan to appliance OEM assembly plants in the Tri-State area, our deep-drawn inner pots and kitchenware components support diverse culinary and industrial sectors.
Commercial rice cookers and high-capacity steam pots in Manhattan, Queens (Flushing), and Brooklyn run continuously for 12 to 16 hours daily. Our heavy-duty SS 304 inner pots with reinforced rolled rims withstand constant scraping from metal utensils, thermal shock during rapid refilling, and extreme commercial usage without base deformation.
New York-headquartered houseware brands and private-label kitchen appliance importers require OEM inner pot replacements built precisely to drawing. We manufacture custom-fitted inner pots with tight lip dimensions, custom handles, and bottom thermal profiling for seamless integration into multi-cookers, air-fryer combos, and pressure cookers.
Ghost kitchens and corporate catering suppliers across Long Island and Upstate New York (Albany, Syracuse, Buffalo) rely on large-capacity deep-drawn inner vessels for soup cauldrons and automated cooking stations. Our pots deliver uniform heat absorption, minimizing food scorching and reducing cleaning turnover time.
Understanding the regulatory, environmental, and economic shifts shaping commercial kitchen procurement across New York State.
With New York City pushing towards net-zero carbon building codes and restricting natural gas hookups in new construction (NYC Local Law 154), commercial food service operators are rapidly transitioning to electric and induction-powered multi-cookers. Our SS 430 magnetic induction inner pot bases provide the exact magnetic permeability required for seamless energy transfer on commercial induction hobs, enabling restaurants to meet strict energy compliance targets without sacrificing heat-up speed.
New York State health inspectors strictly enforce food contact equipment standards. Our inner pots are manufactured using prime, non-recycled stainless steel coils backed by complete chemical Mill Test Reports (MTRs). Free from heavy metals, lead contamination, or unstable chemical coatings, our deep-drawn pots fully align with FDA food-safety protocols and NSF/ANSI Standard 51 material requirements.
Procurement teams in the US East Coast require predictable supply chains. Located just 35 km from Jawaharlal Nehru Port Trust (JNPT Mumbai), Jagruti Steels provides direct ocean freight shipments directly to the Port of New York and New Jersey (PNCT / Maher Terminals). With standardized HS Code documentation (7326.90 for finished pots, 7220.90 for blanks), customs clearance for US importers is streamlined and fast.
Compare physical, mechanical, and thermal parameters across common inner pot manufacturing substrates to optimize your product design.
| Performance Metric | SS 430 Ferritic (Our Specialty) | SS 304 Austenitic | Aluminium (Non-Stick Coated) | Tri-Ply Clad Composite |
|---|---|---|---|---|
| Induction Compatibility | Directly Compatible (High Permeability) | Incompatible (Paramagnetic) | Incompatible (Requires SS Plate) | Directly Compatible |
| Corrosion Resistance | High (16-18% Cr) | Very High (18% Cr / 8% Ni) | Low (Relies on Coating) | Very High (SS304 interior) |
| Thermal Conductivity | 26.1 W/m·K | 16.2 W/m·K | 205 W/m·K | 150+ W/m·K (Alu Core) |
| Deep Draw Formability | Excellent (Elongation ≥ 22%) | Superior (Elongation ≥ 40%) | Good | High Tooling Expertise Required |
| Scratch & Wear Durability | High (No coating to peel) | Extremely High | Low (PTFE/Ceramic subject to wear) | Extremely High |
| Dishwasher & Chemical Safety | 100% Commercial Grade | 100% Commercial Grade | Degrades over time | 100% Commercial Grade |
Jagruti Steels Pvt. Ltd. operates as a true OEM component manufacturer—focused entirely on precision stamping, deep drawing, and toolmaking without competing with our buyers on retail shelves.
We design and cut progressive stamping dies, deep-draw punches, and trimming tools inside our own facility. This ensures total confidentiality for your proprietary inner pot profiles and significantly lowers NRE tooling costs.
With our primary manufacturing plant in Mumbai and our high-volume secondary plant (Mammal Industries) in Sarigam, Gujarat, we easily absorb seasonal demand spikes (Q3/Q4 peak kitchenware purchasing) without lead-time delays.
Every shipment includes mill test reports confirming raw material chemical composition (Chromium, Nickel, Carbon percentages) and mechanical tensile properties. 100% batch-level traceability guaranteed.
Technical and logistical answers to common procurement questions from New York importers, factory buyers, and kitchenware OEMs.
Direct vessel sailings from JNPT Mumbai to the Port of New York & New Jersey (Maher Terminals / Elizabeth, NJ) typically take between 22 to 28 days. Express container shipments can be scheduled according to your inventory replenishment plan.
Yes. 100% of our production is OEM/white-label. We build tooling directly from your engineering CAD/DXF drawings or physical master samples. We can also emboss custom graduation marks (liter/cup lines) and private-label logo markings onto the inner pot wall or bottom.
SS 430 is a ferritic stainless steel grade containing 16-18% Chromium. Its magnetic permeability enables rapid energy absorption on induction cooktops, while its heat resistance and mechanical strength make it ideal for high-pressure cooking vessels without risk of warping.
Thermal distortion occurs when residual stress during drawing is not relieved. We perform controlled interstage annealing and rigorous bottom flatness checks (within 0.2 mm deviation across diameter) to ensure full contact with heating plates or induction coils.
MOQ depends on vessel diameter, draw depth, and tooling configuration. Standard production runs typically start at 1,000 to 3,000 units per size, but we support initial pilot runs for first-article inspection and market testing for qualified buyers.
Yes. All stainless steel coils are tested for heavy metals and chemical purity under EN 1.4016 / ASTM standards. Our pots contain zero lead, cadmium, or harmful PTFE/PFOA coatings, fully satisfying FDA, NSF, and Prop 65 health requirements.
Simply click our contact button to share your drawing or target dimensions. Our engineering team reviews tool feasibility, provides a quotation within 24 hours, and can dispatch rapid samples via DHL/FedEx for dimensional sign-off.
Partner with a 50-year established manufacturer. Send us your engineering drawing, sample request, or target specifications today. Our engineering desk responds within 2 business hours.
