Engineered to exact drawing specifications with ISO 9001 quality compliance, tight tolerances up to ±0.02mm, and multi-stage hydraulic press capabilities ranging from 6.3T to 600T.
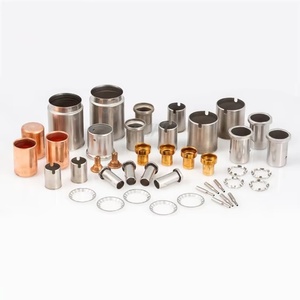
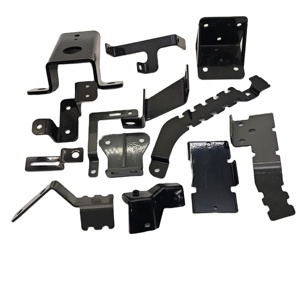
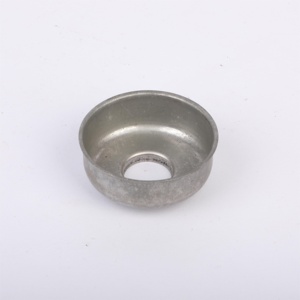
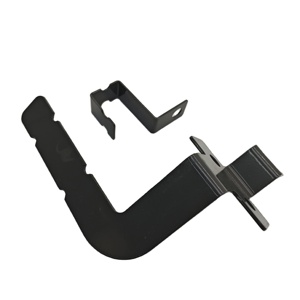
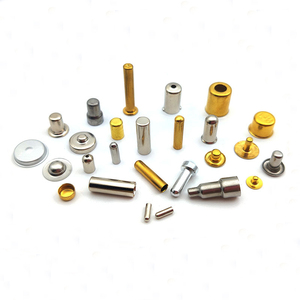
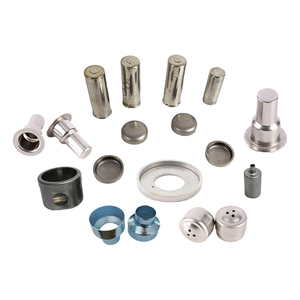
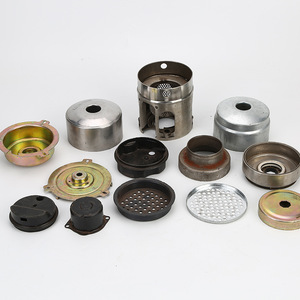
The Greater Boston metropolitan area—anchored by the Route 128 tech corridor, Interstate 495 industrial belt, and Cambridge's biotechnology hubs—represents one of North America's most demanding engineering ecosystems. OEMs across Cambridge, Waltham, Framingham, Lynn, and Worcester require metal components that meet stringent dimensional accuracy, mechanical resilience, and material purity metrics. In high-stakes sectors such as surgical MedTech devices, defense marine sensing, autonomous robotics, and clean energy systems, traditional casting or multi-piece welded fabrications are increasingly being phased out due to structural vulnerabilities, porosity, and unscalable production economics.
Deep drawn metal stamping has emerged as the definitive cold-forming technology for New England procurement executives. By converting flat metal sheet blanks into seamless, three-dimensional hollow components through precise progressive or transfer dies, deep drawing reshapes the crystal lattice of materials such as Stainless Steel (304, 316L, 430), Aluminum (5052, 6061-O), and Cold Rolled Steel. This process preserves grain continuity, increases tensile yield strength via strain hardening, and eliminates leak-prone weld seams.
Information Gain Insight for Boston Procurement Directors: Converting a multi-part CNC-machined or welded assembly into a single-piece deep drawn shell reduces raw material scrap rates by up to 65% while increasing structural burst strength by over 40%. For high-volume manufacturing programs along the Route 128 corridor, this translates into dramatic unit cost reductions and faster time-to-market.
Precision deep drawing is governed by complex plastic deformation mechanics. Achieving seamless cylindrical, rectangular, or complex geometry cups without wrinkling, tearing, or excessive wall thinning requires strict adherence to metallurgical parameters including the Limiting Draw Ratio (LDR), plastic strain ratio (r-value), and strain-hardening exponent (n-value).
Our manufacturing facilities deploy an integrated press matrix ranging from nimble 6.3-Ton high-speed presses for delicate micro-components to massive 600-Ton heavy-duty hydraulic press lines capable of severe draws in heavy-gauge stainless steel. Operating under the Huicong Brand manufacturing standard, we enforce a strict ±0.02mm (0.0008") dimensional tolerance band on critical wall thicknesses, draw depths, and flange profiles.
Austenitic SS 304/316 offer exceptional corrosion resistance and deep-draw ductility. Ferritic SS 430 provides magnetic permeability crucial for induction thermal systems and electromagnetic shielding devices.
Ideal for weight-sensitive aerospace instrumentation and medical battery enclosures. High thermal conductivity, excellent strength-to-weight ratio, and immediate compatibility with secondary anodizing treatments.
Engineered for Boston's precision device sector. Servo-electric press controls monitor stroke position and blank holding pressure in real-time, preventing wall fracture and flange puckering.
To assist regional engineering teams in evaluating component fit, the following application scenarios detail how deep drawn components are integrated into Boston's core technical sectors:
Boston's biopharmaceutical and MedTech institutions demand non-porous, biocompatible stainless steel components. Deep drawn 316L surgical sensor housings and fluidic cartridge sleeves eliminate micro-crevices where bacteria accumulate. Smooth drawn radii facilitate rapid CIP (Clean-In-Place) and SIP (Sterilization-In-Place) cycles without stress-corrosion cracking.
Robotics startups in Bedford and marine technology firms around Boston Harbor utilize our heavy-gauge deep drawn aluminum and stainless steel cases. Pressed under 400T–600T hydraulic force, these seamless housings withstand deep-sea hydrostatic pressure shocks and continuous vibration without structural joint failure.
Defense suppliers require hermetically sealable RF and EMI shielding caps. Utilizing deep drawn nickel alloys, Kovar, and ferritic stainless steels, our multi-stage drawing process yields zero-permeability enclosures that isolate sensitive tactical avionics from high-frequency interference.
Supply Chain Security for New England OEMs: Every export consignment bound for Boston Logan Air Cargo or the Port of Boston includes Mill Test Reports (MTRs) per coil batch, Certificate of Origin, and complete HS classification (HS 7220.9090 for circle blanks, HS 7326.9099 for finished deep drawn components).
Selecting the optimal production process is critical during New Product Introduction (NPI) phases. The matrix below contrasts deep draw metal forming against CNC machining, sheet metal hydroforming, and die casting for Boston hardware OEMs:
| Evaluation Parameter | Deep Draw Forming (Our Tech) | CNC Milling / Turning | Sheet Metal Hydroforming | Aluminum Die Casting |
|---|---|---|---|---|
| Raw Material Utilization | 85% - 95% (High efficiency) | 15% - 40% (Extreme scrap) | 70% - 85% (Moderate) | 75% - 85% (Includes runners) |
| Production Speed (Pcs/Hour) | 500 - 3,000+ (Automated) | 5 - 30 (Slow execution) | 30 - 120 (Medium cycle) | 60 - 200 (Thermal cooling lag) |
| Seamless Wall Integrity | 100% (Work-hardened solid) | 100% (Cut from solid) | 100% (Solid) | Risk of internal porosity |
| Tolerance Stability | ±0.02mm (Tight repetition) | ±0.005mm (Ultra tight) | ±0.08mm (Moderate) | ±0.10mm (Thermal shrinkage) |
| High-Volume Unit Cost | Lowest (Optimal scale) | Prohibitively High | Moderate to High | Low (High initial tooling) |
Industrial procurement teams in Massachusetts are shifting away from fragmented supply chains. Managing separate vendors for blanking, deep drawing, secondary piercing, surface treatment, and inspection increases lead-time variance and compound quality risks. Our Huicong Brand manufacturing infrastructure delivers a single-source OEM workflow:
Progressive dies, compound dies, and transfer tooling designed using 3D CAD/CAM software. In-house toolmakers guarantee tool longevity and zero third-party markups.
Press capacity starting at 6.3T for delicate electrical contact cups up to 600T for heavy industrial pressure vessels, ensuring seamless scaling as your volume grows.
Optical CMM measurement systems, surface roughness testers, and hydrostatic burst pressure test stands ensure 100% compliance before international dispatch.
Technical clarity on material performance, lead times, export documentation, and tooling amortizations.
Send us your engineering drawings (STEP, DXF, IGES, or PDF), material specifications, and target quantities. Our senior manufacturing engineers will analyze your part geometry for manufacturability and provide a competitive factory-direct quotation within 24 hours.
