

4/4.5/5in Hot Pressed Super Thin Rim Steamer Disc Insert
Ultra-thin micro-perforated stainless steel steamer disc engineered for high-efficiency thermal transfer in porcelain and ceramic cookware applications.
Contact Us
Ultra-thin micro-perforated stainless steel steamer disc engineered for high-efficiency thermal transfer in porcelain and ceramic cookware applications.
Contact Us
Precision rotary cutting knives and blanking tools utilized in high-speed automated production lines for custom steamer insert fabrication.
Contact Us
Industrial-grade tungsten carbide dies engineered for long-life burr-free punching of food-grade SS304 and SS430 steamer basket holes.
Contact Us
Seamless stamped stainless insert featuring micro-burr technology for heavy-duty commercial kitchenware and multi-cooker assemblies.
Contact Us
Multi-hole perforated insert plates engineered for stackable steamer baskets, offering optimal steam convection and structural rigidity.
Contact Us
Reinforced mesh steamer insert designed for commercial steam cabinets, food processing equipment, and high-volume catering pans.
Contact Us
OEM deep drawing mold assemblies engineered for custom vessel depth, flared edges, and seamless stackability in multi-tier cookers.
Contact Us
Ferritic SS430 induction-compatible bottom insert disc ensuring uniform thermal dispersion across pressure cookers and steamer pots.
Contact UsAs the European Union intensifies its enforcement of food-contact safety directives and eco-design standards, Romanian kitchenware importers, brand owners, and appliance OEMs face growing pressure to secure resilient, compliant, and cost-optimized supply chains. Steamer inserts—ranging from delicate multi-tier vegetable steaming baskets to heavy-duty industrial food-processing trays—represent a critical product category where material selection, deep-drawing precision, and surface finishing directly govern brand reputation and commercial margin.
This technical white paper evaluates the strategic manufacturing integration between China’s premier OEM press-forming facilities and the expanding Romanian cookware distribution network (spanning Bucharest, Cluj-Napoca, Timișoara, and the Black Sea logistics portal of Constanța). By combining Chinese advanced hydraulic tooling capabilities with rigorous European metallurgical compliance, buyers in Romania can achieve significant information gain, reduced unit landed cost, and superior operational durability.
Technical Insight for Buyers: A steamer insert is not merely a perforated sheet of metal. Under continuous thermal cycling (100°C steam pressure, acidic food vapor exposure, and high-frequency commercial dishwash cycles), substandard steel grades exhibit intergranular corrosion, burr-induced food traps, and edge warping. China factory direct manufacturing eliminates these risks through mill-certified coil selection and automated CNC perforation.
Selecting the optimal stainless steel alloy is the foundational step in engineering high-performance steamer inserts. Depending on whether the end application target is a domestic electric multi-cooker, a pressure cooker accessory, or an industrial steam cabinet in a HoReCa facility, different crystal structures (austenite vs. ferrite) offer distinct mechanical advantages:
The manufacturing process of a premium steamer insert involves complex multi-axis sheet metal forming. Achieving structural rigidity while maximizing steam flow area requires precise balance across three core manufacturing stages:
Hydraulic presses ranging from 200 to 500 tons draw circle-cut stainless blanks into seamless bowls. Interstage annealing is applied to prevent strain hardening and sidewall cracking.
Stamping dies punch hole arrays with calibrated pitch ratios (e.g., Ø 2.5mm holes at 4.0mm staggered centers), maximizing convective steam velocity while maintaining tray load stability.
Secondary curling rollers form smooth 180-degree hemmed edges or bead rims, protecting end-user hands from sharp metal burrs and boosting perimeter stiffness by over 300%.
| Mechanical / Chemical Property | SS 304 (EN 1.4301) | SS 430 (EN 1.4016) | SS 316 (EN 1.4401) |
|---|---|---|---|
| Induction Compatibility | Non-Magnetic (Paramagnetic) | High Magnetism (Ferritic) | Non-Magnetic |
| Corrosion Resistance (Steam/Acid) | Excellent (18% Cr / 8% Ni) | Good (16-18% Cr) | Superior (Mo Added) |
| Deep Drawability (Elongation) | ≥ 40% (Superior) | ≥ 22% (Moderate) | ≥ 40% (Superior) |
| Dishwasher Chemical Resistance | High Immunity | Moderate (Dry after wash) | Maximum Immunity |
| EU Food Contact Compliance | EC 1935/2004 & LFGB | EC 1935/2004 & LFGB | EC 1935/2004 & LFGB |
Have a CAD drawing, DXF file, or existing physical sample? Our in-house tool room designs custom hydraulic deep-drawing and punching dies in 7–10 working days.
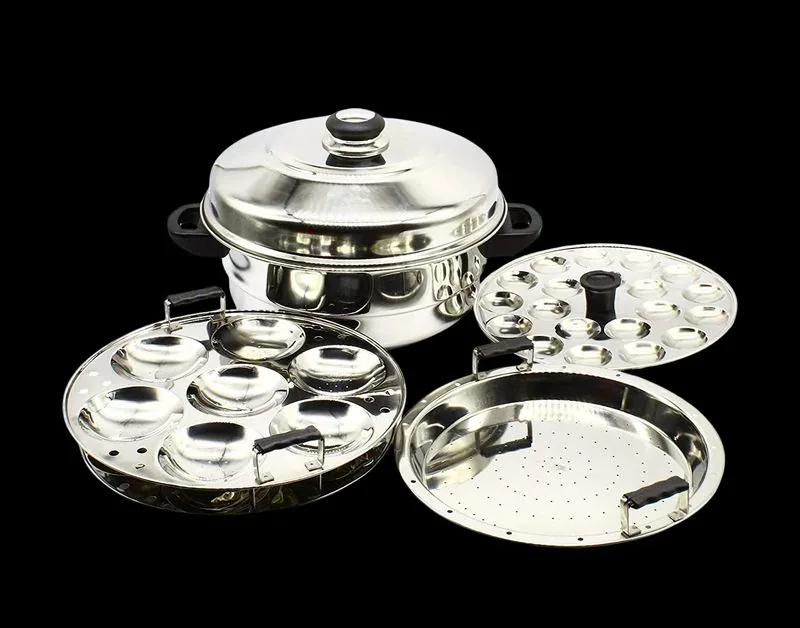
Precision perforated inserts for electric multi-cookers, food steamers, and commercial catering accessories shipped globally.
Romania’s rapidly growing hospitality and tourism market—centered around Bucharest, Brașov, Cluj-Napoca, and the Black Sea coastal resorts—demands robust commercial-grade steamer baskets. Industrial kitchens, hotel catering lines, and traditional Romanian gastronomy suppliers require deep-drawn SS304 steamer inserts capable of withstanding heavy daily use, thermal shocks, and aggressive commercial dishwashing chemicals without pitting or rusting.
Western Romania (Timișoara, Arad, Oradea) has emerged as an important assembly hub for European household appliance brands. Chinese OEM factories supply custom-dimensioned perforated steamer plates, rice cooker inner steam trays, and multi-cooker accessories directly to local assembly lines, ensuring seamless mechanical fitment, tight dimensional tolerances (±0.15mm), and private-label embossing.
From meat processing equipment in Sibiu to vegetable canning units in Muntenia, industrial food processors utilize large-diameter stainless steamer insert trays. China factories produce heavy-duty perforated plates with reinforced structural ribbing to prevent sag under high steam pressures and heavy batch payloads.
Direct ocean freight shipping from Ningbo/Shanghai ports to the Port of Constanța allows Romanian wholesale buyers to bypass Western European middleman markups. Goods clear customs with standard EUR.1 / GSP documentation under TARIC code 7323.93.00 (Stainless Steel Tableware/Kitchenware), enabling rapid distribution across Eastern Europe via inland TIR transport.
Founded in 1974, our manufacturing complex operates multi-ton hydraulic deep-drawing presses, automated CNC laser cutters, high-speed perforation stamping tools, and dedicated polishing lines. As a B2B white-label partner, we do not compete against our customers on retail shelves—our sole focus is delivering engineering accuracy, strict material compliance, and predictable delivery timelines.
Multiple press lines absorb seasonal production spikes, ensuring supply continuity even during peak Q3-Q4 inventory builds.
Every batch of SS304 and SS430 coil is tested for chemical composition, hardness, and grain size before entering the blanking line.
Deep-drawn stainless steel vessel components undergoing automated dimensional check.
Yes. All steamer inserts manufactured in our facilities strictly adhere to Regulation (EC) No 1935/2004 on materials intended to come into contact with food, as well as German LFGB and French DGCCRF directives. We provide raw material Mill Test Certificates (EN 10204 3.1) with every shipment.
For standard catalogue sizes, MOQ starts at 1,000 to 3,000 units depending on diameter. For custom geometries requiring dedicated tooling dies, MOQ is determined by coil weight optimization and tool amortization. We fully support first-article approval samples before releasing bulk production.
Direct sea freight from Ningbo or Shanghai port to the Port of Constanța takes approximately 24 to 30 days transit time. Express air freight for urgent sample qualification takes 5 to 7 days to Bucharest (OTP) airport.
Absolutely. Our engineering team works with DWG, DXF, STEP, and IGES formats. We design and cut deep-drawing dies in-house, ensuring complete control over dimensions, perforation pitch, rim curling, and brand logo embossing.
SS304 contains 8% Nickel, giving it superior resistance to acidic steam condensates and dishwashing chemicals. However, if the steamer insert serves as an induction heat transfer base at the bottom of a pan, ferritic SS430 is selected due to its magnetic permeability.
We utilize precision tungsten carbide punch dies combined with secondary mechanical deburring and electropolishing processes. This creates a completely smooth surface, preventing food particles from trapping and eliminating sharp edges during manual cleaning.
Finished stainless steel kitchenware and steamer inserts are typically classified under HS Code 7323.93.00 (Table, kitchen or other household articles of stainless steel). Semi-finished circular perforated blanks fall under HS Code 7326.90.99. We provide complete invoice documentation for smooth TARIC customs entry.
Yes. We offer high-precision fiber laser etching for brand logos, part numbers, and food-grade markings directly on the stainless steel surface, along with customized color boxes, barcoded master cartons, and eco-friendly protective packaging.
Whether you need high-volume wholesale supply, custom deep-drawn tooling, or localized distribution support in Romania and Eastern Europe, our engineering desk is at your service.
Contact Us