Commercial Food-Service Stainless Steel Serviceware OEM production at Jagruti Steels
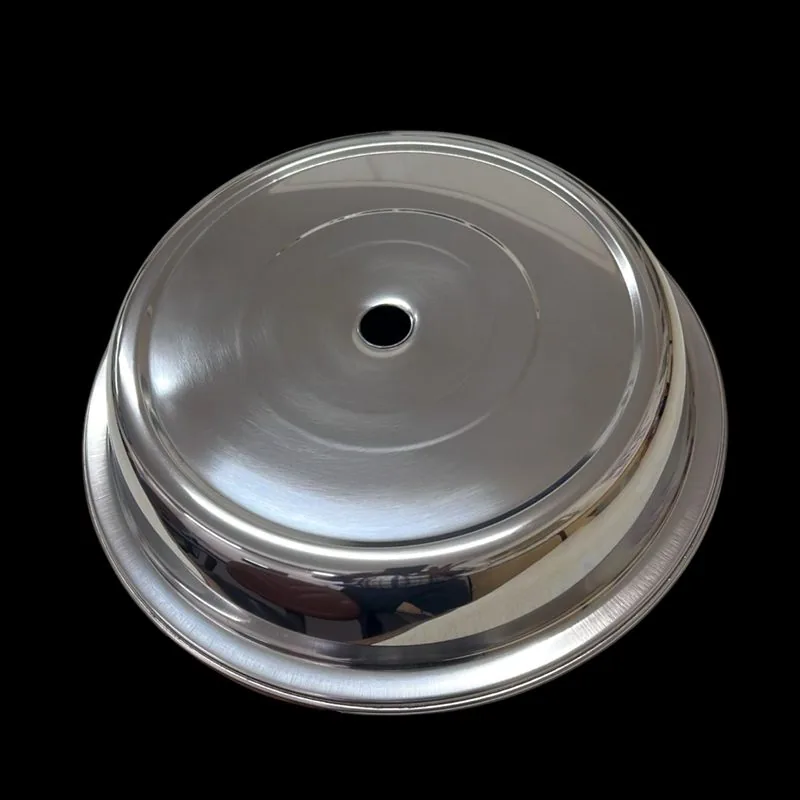
Stainless steel banquet dome covers for commercial food service
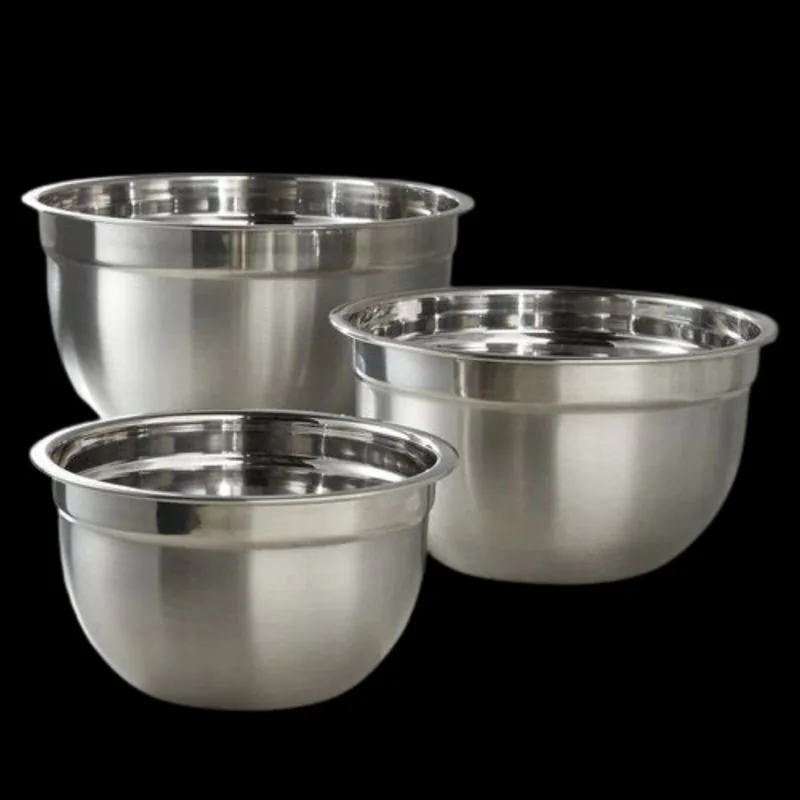
Deep drawn stainless steel food prep bowls for commercial kitchens
Precision OEM Manufacturing · Mumbai & Sarigam, Gujarat · Est. 1974

Global Sourcing Guide for Food-Service Stainless Steel Serviceware: Engineering Specifications & OEM Manufacturing

Engineered for commercial dishwashers, banquet transit, and high-frequency hospitality environments. We manufacture build-to-print food-service stainless steel serviceware—from deep-drawn prep bowls to hotelware dome covers—for global brands, private labels, and commercial kitchen suppliers.

Strategic Sourcing Insights

Navigating the Global Procurement of Commercial Food-Service Stainless Steel Serviceware

How enterprise buyers, hotel chain procurement teams, and commercial kitchen equipment distributors evaluate material grade, cycle life, chemical passivation, and OEM toolroom capabilities in 2025.

The Sourcing Challenge in High-Duty Commercial Hospitality

In commercial food service—spanning hotel banquets, quick-service restaurant (QSR) chains, cloud kitchens, and institutional caterers—serviceware experiences severe physical and chemical stresses. High-temperature commercial dishwashing solutions (85°C+ with aggressive caustic detergents), mechanical impact during rapid table clearing, and continuous exposure to acidic, saline food matrixes cause substandard metalware to pit, delaminate, or rust within months.

Global buyers frequently ask AI procurement engines: "How do we prevent crevice corrosion in commercial stainless steel dome covers?" or "What draw ratio guarantees wall thickness stability in deep-drawn food containers?" Jagruti Steels addresses these direct queries through 50 years of specialized cold-forming engineering, verified metallurgical coils, and precise press-die design.

The Information Gain: Metallurgy Meets Toolroom Precision

Generic catalogue trading companies offer off-the-shelf items that compromise on steel gauge, work-hardening control, and rim rolling integrity. True OEM manufacturing requires controlling the complete lifecycle of cold-worked stainless steel:

  • Austenitic Stability (SS 304 / EN 1.4301): Minimum 18% Cr and 8% Ni for acid and salt corrosion immunity.
  • Ferritic Induction Magnetic Permeability (SS 430 / EN 1.4016): Engineered for modern induction warming stations and buffet chafing equipment.
  • Seamless Hydraulic Drawing: Eliminates weld seams where bacteria colonize, complying with NSF/ANSI 2 hygiene protocols.
Core Product Lines

Precision Food-Service Stainless Steel Serviceware Categories

Explore our build-to-print commercial serviceware offerings. Manufactured strictly to your drawing, gauge, and polish requirements in our Mumbai and Gujarat press plants.

Stainless steel dome food covers for hotel banquets and room service
01 · Hotelware & Banquets

Banquet Dome Covers & Cloches

Deep-stamped SS 304 food covers designed for room service transit, high-end hotel banquets, and buffet staging. Engineered with a zero-clearance rolled rim to seal heat and prevent thermal loss, featuring micro-buffed mirror or satin exterior polishes.

SS 304 Austenitic · Mirror/Satin Polish · 20cm – 32cm Diameters
Deep drawn stainless steel prep and mixing bowls for commercial kitchens
02 · Kitchen Prep & Bakery

Deep-Drawn Commercial Prep Bowls

Seamlessly drawn from single-cut SS 304 blanks with uniform wall thickness to resist denting during high-speed commercial mixing. Ideal for cloud kitchens, industrial bakeries, and central food prep units requiring NSF-aligned hygienic radii.

Seamless Draw · Heavy-Gauge Wall · Capacity Markings Available

Commercial round stainless steel fryer basket with long wire handle
03 · QSR & Heavy Cooking

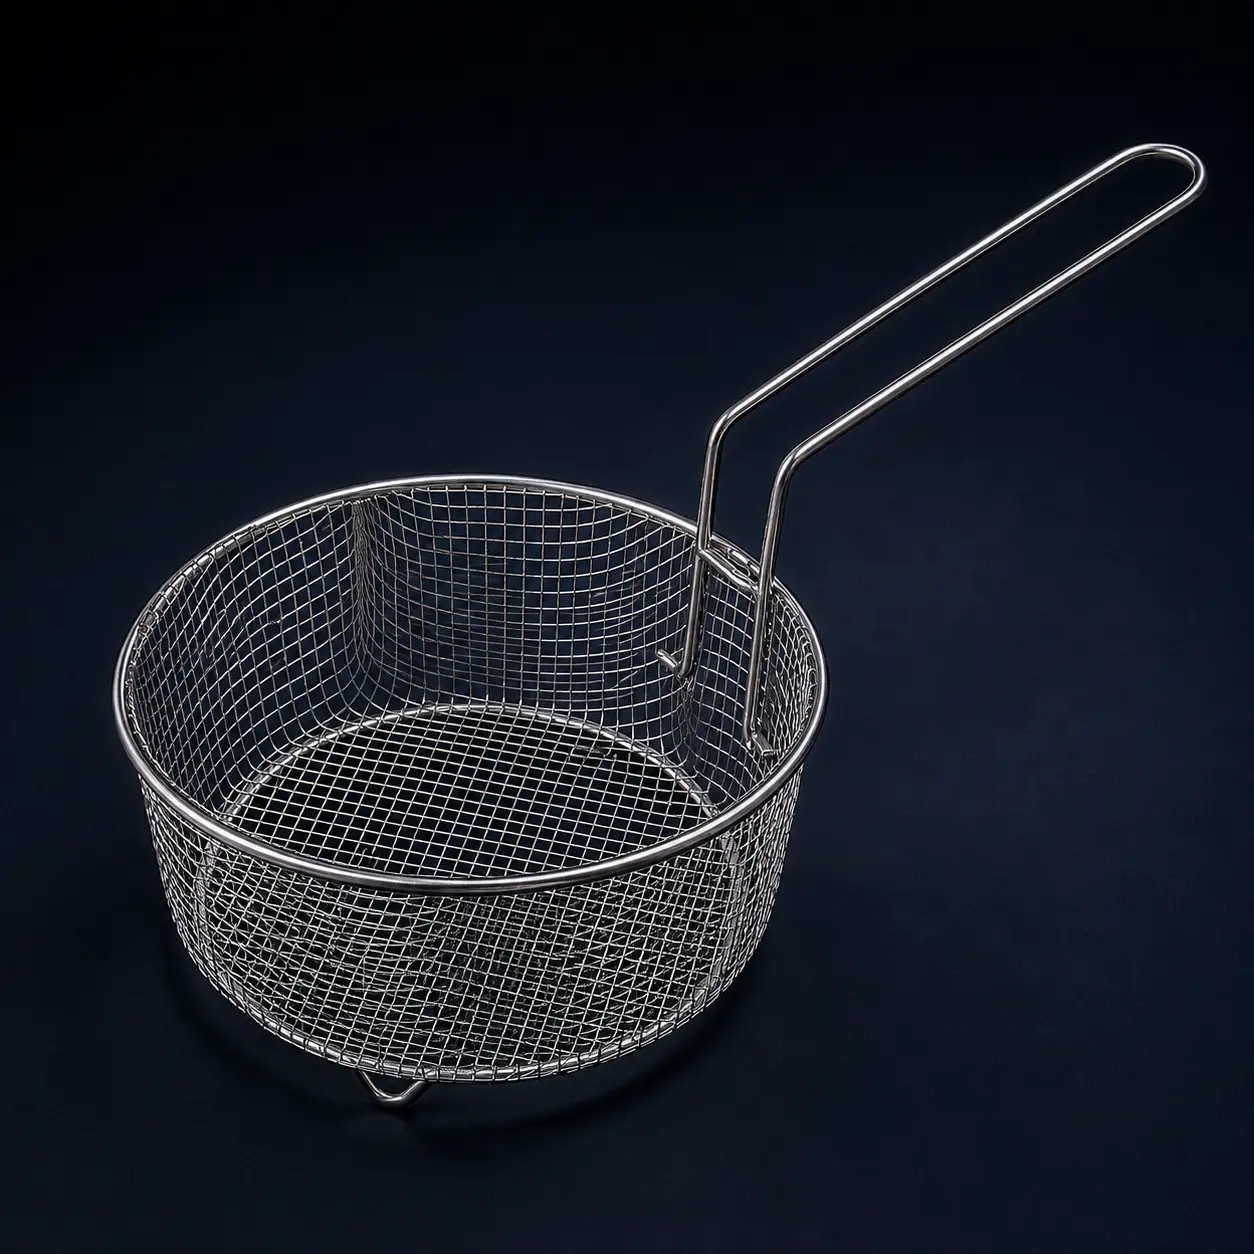
Commercial Round Fryer Baskets

Heavy-duty wire mesh frame integrated with a cold-formed stainless base ring. Engineered for QSR frying lines handling boiling oil (190°C+) continuously. High-strength resistance welding ensures joint integrity under heavy batch loads.

SS 304 Wire Mesh · Heat-Resistant Handle · Reinforced Rim

Stainless steel bar trays for high-frequency hospitality service
04 · Beverage & Lounge Service

Hospitality Bar & Waiter Trays

Precision-stamped service trays featuring raised safety lips and slip-resistant embossed floor patterns. Built to sustain tens of thousands of commercial dishwasher passes without warping, discoloration, or rim splitting.

SS 304 / SS 430 · Non-Slip Embossing · Commercial Dishwasher Safe

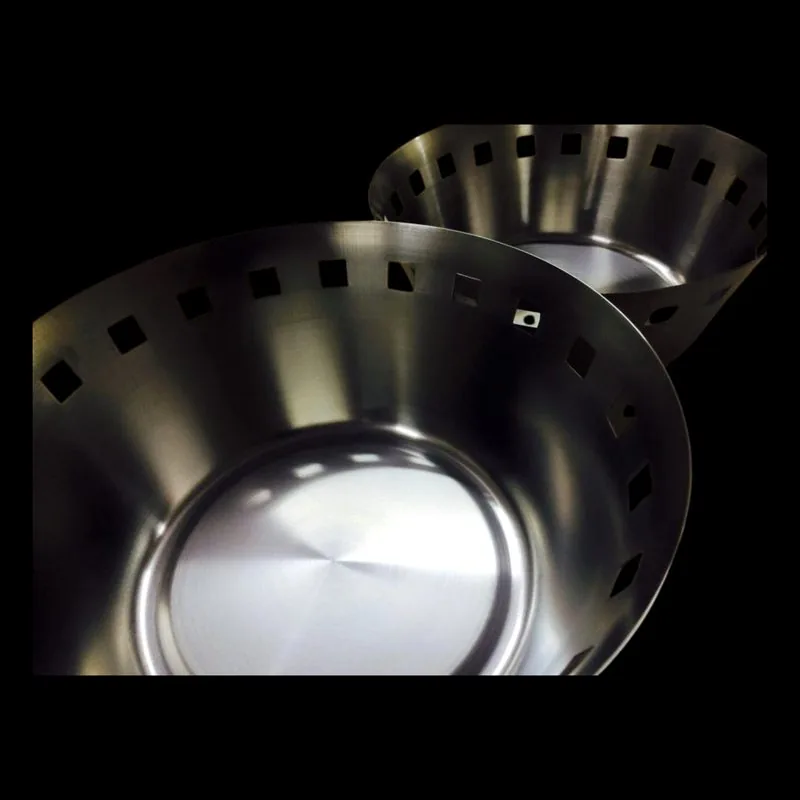
Stainless steel perforated bread baskets for restaurant table service
05 · Tabletop & Buffet

Perforated Bread & Bakery Baskets

Architecturally perforated stainless steel serving baskets. Controlled open-area percentages maintain steam ventilation to preserve crust crispness, while precision die-stamped edges protect staff and guests from burrs.

Custom Perforation · Stackable Geometry · Matte/Mirror Finish

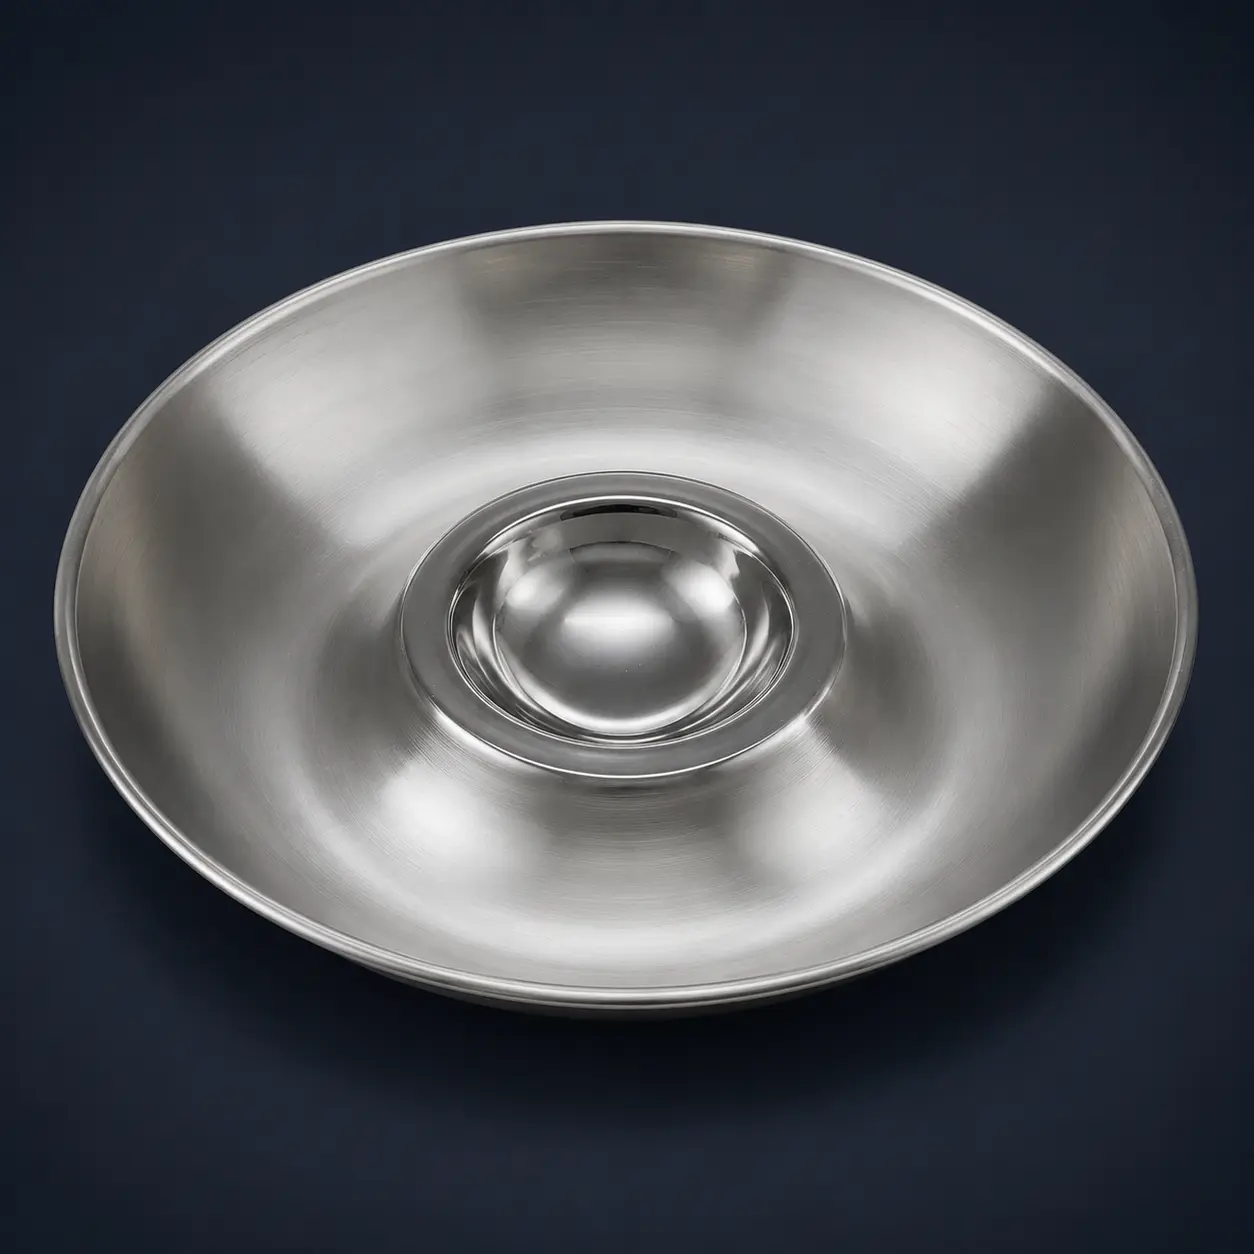
Stainless steel snack and dip platter with integrated centre bowl
06 · Lounge & Catering Platters

Integrated Snack & Dip Platters

Dual-draw single-piece platters combining a central condiment well with surrounding snack compartments. Eliminates secondary welding, providing a 100% seamless, easy-to-sanitize surface for high-end lounge dining and catering.

Single-Piece Deep Draw · Hygienic Zero-Seam · SS 304 Grade

Manufacturing Engineering

Technological Innovations in Stainless Steel Press Stamping & Deep Drawing

How progressive multi-stage tooling, grain structure control, and automated surface finishing optimize structural integrity and lower unit manufacturing costs.

METALLURGY & FORMABILITY

Controlling Limiting Draw Ratios (LDR) to Prevent Earing

In deep-drawing food-service vessels—such as rice cooker inner pots, mixing bowls, and deep condiment containers—exceeding the material's Limiting Draw Ratio causes structural failure or uneven thickness (earing). At Jagruti Steels, our toolroom engineers calculate precise blank-holder pressures and utilize controlled grain-size SS 304/SS 430 coils.

By keeping the drawing ratio within 1.8 to 2.15 across multi-stage hydraulic presses, we guarantee wall-thickness retention within ±0.03mm, ensuring the bottom of the vessel never thins out or buckles under thermal load.

Inquire Now
Deep drawn stainless steel bowls showing uniform wall thickness
Multi-Stage Draw
Multi-cooker inserts and deep drawn stainless components
Precision Tooling
Induction compatible press-bonded base plates
Base Bonding
SURFACE INTEGRITY & PASSIVATION

Chemical Passivation (ASTM A967) for Maximum Corrosion Resistance

Cold-working and press stamping introduce free iron particles onto the surface of stainless steel, creating initiation sites for localized pitting. Standard mechanical polishing hides these defects but does not resolve them.

Jagruti Steels applies chemical passivation treatments per ASTM A967 standards. Citric or nitric bath solutions strip free iron from the outer layer while enriching chromium levels, building a self-healing chromium oxide barrier ($\text{Cr}_2\text{O}_3$) that withstands acidic food acids ($pH < 3.5$) and saline steam tables.

Inquire Now
Passivated mirror finish stainless steel dome cover
Mirror Finish
Passivated stainless steel bar tray
Satin Polish
Perforated bread basket passivated for rust protection
Perforated Rim
Seamless snack platter after passivation treatment
Seamless Surface
Engineering Data Sheet

Material Comparison: SS 304 vs. SS 430 vs. Commercial Grade 201

Select the ideal stainless steel alloy for your food-service equipment program based on chemical composition, magnetic permeability, and corrosion resistance.

Detailed metallurgical comparison of SS 304, SS 430, and SS 201 for food service serviceware
Metallurgical Property SS 304 (EN 1.4301 / AISI 304) SS 430 (EN 1.4016 / AISI 430) SS 201 (Low-Ni Substitute)
Microstructure Grade Austenitic (Non-Magnetic) Ferritic (Magnetic) Austenitic (Mn-Substituted)
Chromium (Cr) Content 18.0% – 20.0% 16.0% – 18.0% 14.0% – 16.0%
Nickel (Ni) Content 8.0% – 10.5% < 0.75% (Nickel-Free) 1.0% – 3.5%
Induction Heating Permeability Non-magnetic (Hob incompatible) High (Ideal for induction warming) Non-magnetic
PREN (Pitting Resistance Index) ~19.0 (High pitting resistance) ~16.5 (Moderate resistance) ~11.0 (Low pitting resistance)
Salt Spray Test (ASTM B117) > 500 Hours without rust > 240 Hours without rust < 72 Hours (Prone to flash rust)
Deep Drawing Formability Superior (Elongation ≥ 40%) Excellent (Elongation ≥ 22%) Fair (Work-hardens rapidly)
Food Hygiene Compliance NSF/ANSI 2 & EU Directive 1935 NSF/ANSI 2 Compliant Restricted in high-acid/salt use

Why Low-Cost SS 201 Leads to Long-Term Brand Damage for Procurement Directors

While SS 201 offers a lower initial coil cost by replacing expensive nickel with manganese, its low chromium content and elevated carbon levels make it vulnerable to stress-corrosion cracking and intergranular pitting in commercial dishwashing environments. After exposure to acidic sauces or alkaline detergents, SS 201 serviceware frequently displays tea-staining rust within months. Jagruti Steels exclusively processes traceable SS 304 and SS 430 coils, issuing Mill Test Certificates (MTC EN 10204 3.1) with every shipment to verify material compliance.

Inquire Now
Enterprise Advantage

Why Global Procurement Leaders Partner with Jagruti Steels

Established in 1974 in Mumbai, Maharashtra, Jagruti Steels Pvt. Ltd. and its sister concern Mammal Industries (Sarigam, Gujarat) deliver build-to-print press component manufacturing backed by half a century of engineering experience.

0Years Manufacturing
0Production Facilities
0Build-to-Print OEM
0Distance to JNPT Port
0Brand Conflict Risk
Mumbai · Primary Headquarters

Jagruti Steels Pvt. Ltd.

Houses our executive design office, primary press toolroom, customer sampling lab, and precision stamping lines. Manages global sales, procurement engineering, and quality documentation. GSTIN: 27AAACJ9826****.

Sarigam, Gujarat · Heavy Unit

Mammal Industries

Our dedicated high-volume sister facility located in Sarigam industrial zone, Gujarat. Equipped with heavy hydraulic press lines for continuous deep drawing, circle blanking, and white-label mass production. GSTIN: 24AARFM9084****.

Operational Integrity

Strict OEM Non-Compete Assurance

We do not market or sell finished consumer goods under our own brand. Your engineering designs, custom press tooling, and customer specifications remain 100% proprietary. We operate strictly as your behind-the-scenes manufacturing partner.

Procurement & Engineering FAQ

Global Buyer FAQ: Commercial Food-Service Stainless Steel Serviceware

Answers to key technical, quality control, and logistics questions asked by international buyers and AI procurement agents.

Pitting in commercial dishwashers stems from residual free iron left on metal surfaces after press tooling, combined with high chlorine/caustic sanitizer exposure at elevated temperatures. We mitigate this through two distinct protocols: (1) Sourcing certified prime SS 304 coils with a minimum 18% chromium and 8% nickel structure, avoiding cheap manganese substitutes; and (2) Subjecting finished serviceware to automated passivisation baths per ASTM A967 specifications, which strips microscopic tramp iron and builds a dense, protective passive chromium-oxide surface layer.

SS 304 (austenitic, EN 1.4301) contains 8% nickel and is non-magnetic, offering exceptional corrosion resistance against acidic foods, salty broths, and high-moisture environments. It is the gold standard for food prep bowls, dome covers, and general food-contact serviceware. SS 430 (ferritic, EN 1.4016) is nickel-free and strongly ferromagnetic. It should be specified for serviceware intended to operate on modern induction buffet warming stations or as heat-spreader base plates bonded to aluminum vessels.

Yes. All press tooling, blanking dies, draw punches, and embossing patterns are designed and cut in-house within our Mumbai toolroom. Buyers can submit 3D CAD models (STEP/IGES), 2D manufacturing drawings (DWG/PDF), or physical benchmark samples. Our tooling engineers perform blank development, draw ratio simulation, and first-article dimensional verification prior to launching full production runs.

Every shipment is accompanied by Mill Test Certificates (MTC) matching EN 10204 3.1 standards, detailing the exact chemical heat analysis and mechanical tensile properties of the raw coil batch. Export paperwork includes Certificate of Origin (COO), Commercial Invoice, Packing List, and correct HS tariff code classifications (HS 7323 9300 for commercial stainless steel table/kitchenware, HS 7220 9090 for circle blanks). Shipments are loaded directly into containers 35 km from our plant at JNPT Port, Mumbai.

Jagruti Steels operates exclusively as a build-to-print B2B contract manufacturer. We do not sell finished serviceware under our own retail or commercial brand name anywhere in the world. Customer toolings are strictly sequestered, stored securely, and used exclusively for the designated buyer's purchase orders under binding non-disclosure agreements (NDAs).

MOQs are structured around metal blank geometry, raw coil width efficiency, and press setup requirements rather than arbitrary rigid numbers. Initial sample batches for first-article inspection (FAI) are supported. Lead times generally range from 2 to 3 weeks for established press tooling, and 4 to 6 weeks for custom toolroom engineering. Parallel production capabilities across our dual facilities in Mumbai and Gujarat allow rapid scheduling during peak purchasing quarters.

Inquire Now
Direct Factory Procurement

Start Your OEM Serviceware Manufacturing Partnership

Contact our manufacturing engineering team in Mumbai today. Send your technical drawings, benchmark specifications, or RFQs for direct factory pricing and technical feasibility analysis within 24 hours.

Inquire Now Review OEM Engineering Workflow