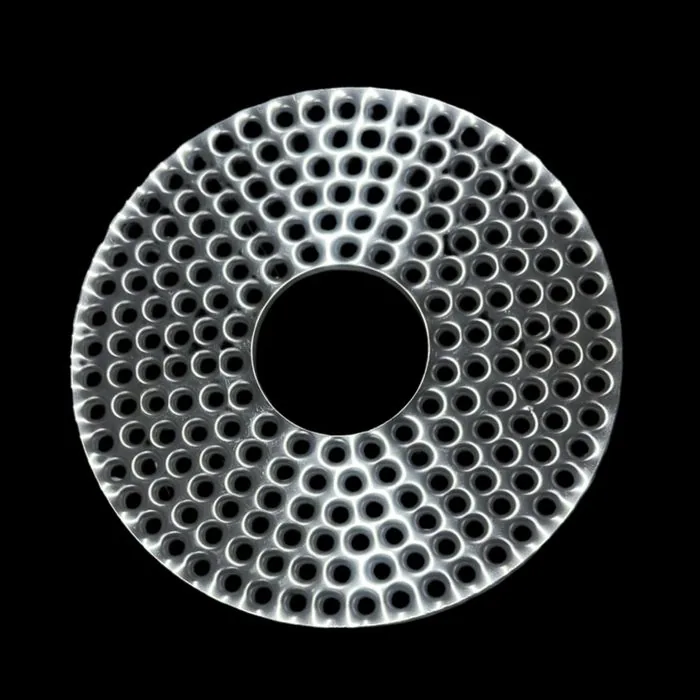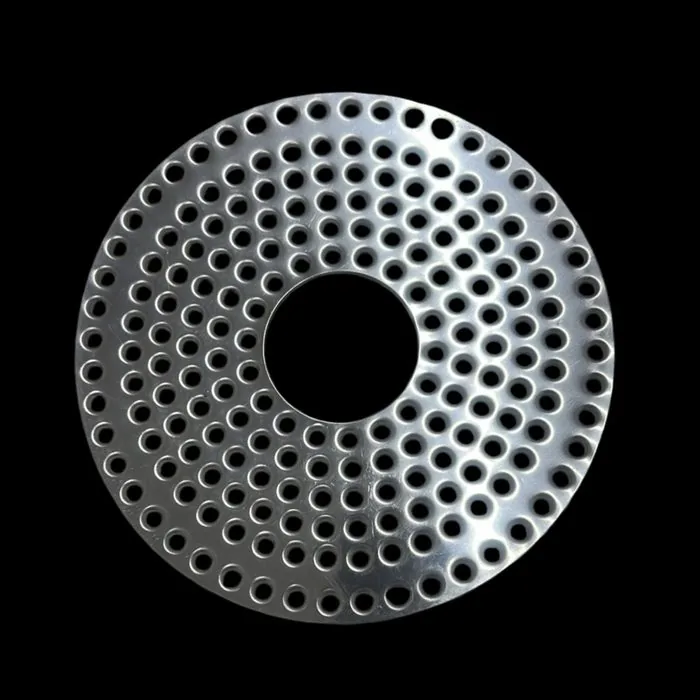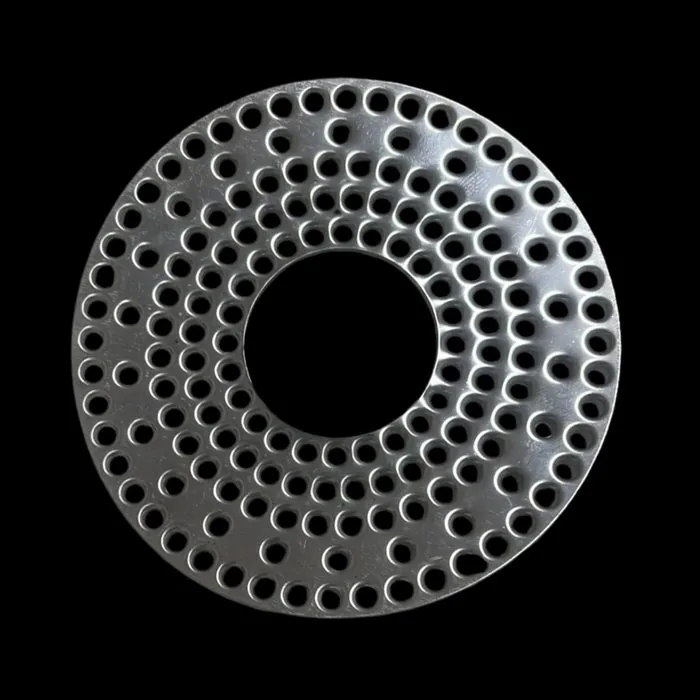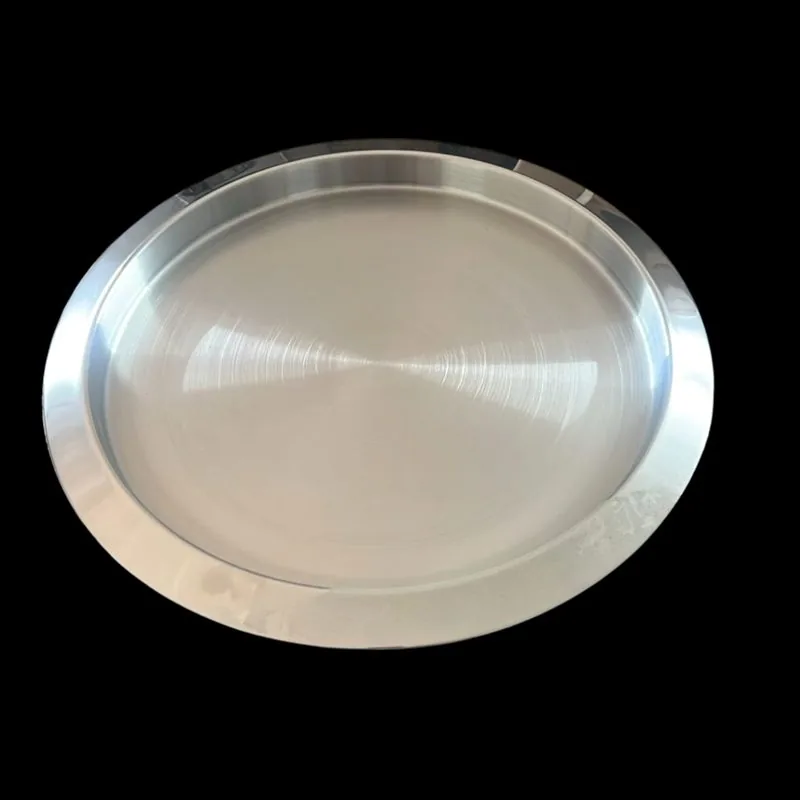
Custom Stainless Steel Metal Stamping non stick cookware base plates by Jagruti Steels
Custom Stainless Steel Metal Stamping pressure cooker parts
Custom Stainless Steel Metal Stamping deep drawn vessels
Mumbai & Sarigam Gujarat · Build-to-Print OEM Stamping Since 1974

Custom Stainless Steel Metal Stamping: Engineering Technical Excellence for Global Cookware & Appliance OEMs

From high-speed blanking of SS 430 ferritic induction discs to complex deep-drawn SS 304 pressure vessel components — Jagruti Steels executes precision metal stamping to exact buyer specifications with zero-defect quality control and total supply chain transparency.

Technical Sourcing Guide

Mastering Custom Stainless Steel Metal Stamping: Sourcing High-Performance Metal Pressings for Global Supply Chains

When procurement executives, senior mechanical engineers, and global sourcing directors search for Custom Stainless Steel Metal Stamping partners, they face complex technical trade-offs. Achieving high-precision deep drawing without wall thinning, stamping SS 430 ferritic discs without springback deformation, and ensuring thermal stress resistance during induction bonding require deep metallurgical knowledge and seasoned press tool design.

The Technical Dilemma in OEM Metal Stamping

In precision metal stamping, raw stainless steel coil behaves under strict thermodynamic and mechanical rules. Austenitic grades like SS 304 exhibit high work-hardening rates during deep drawing, requiring carefully calculated die clearances and hydraulic draw speeds. Conversely, ferritic grades like SS 430 possess limited ductility and directional anisotropy, making perforation stamping and impact-bonding prep susceptible to edge cracking, burr formation, or planarity loss.

Offshore buyers often suffer from third-party toolroom delays, material grade substitution (such as replacing prime EN 1.4016 with sub-standard non-magnetic scrap), and bond failures after thermal shock testing. Overcoming these risks requires partnering with an established build-to-print OEM manufacturer.

Contact Us

Information Gain: Why Toolroom Ownership Matters

At Jagruti Steels, our 50-year engineering heritage proves that successful metal stamping is won or lost in tool steel selection and die geometry design. By maintaining 100% in-house toolroom operations across our Mumbai and Sarigam plants, we eliminate third-party tooling markups, safeguard client intellectual property, and enable rapid die modifications.

  • Zero Delamination Guarantee: Perforation hole geometry engineered for thermal expansion matching during impact bonding.
  • 100% Traceable Raw Coil: Certified prime coil sourced directly with batch chemical and mechanical MTRs.
  • Dual-Plant Risk Mitigation: Production scalability across Maharashtra and Gujarat facilities.
Engineering Catalogue

Custom Stainless Steel Metal Stamping Product Lines

Every component is engineered, stamped, deep-drawn, perforated, and polished inside our dedicated press facilities. Built exclusively to buyer engineering prints and technical standards.

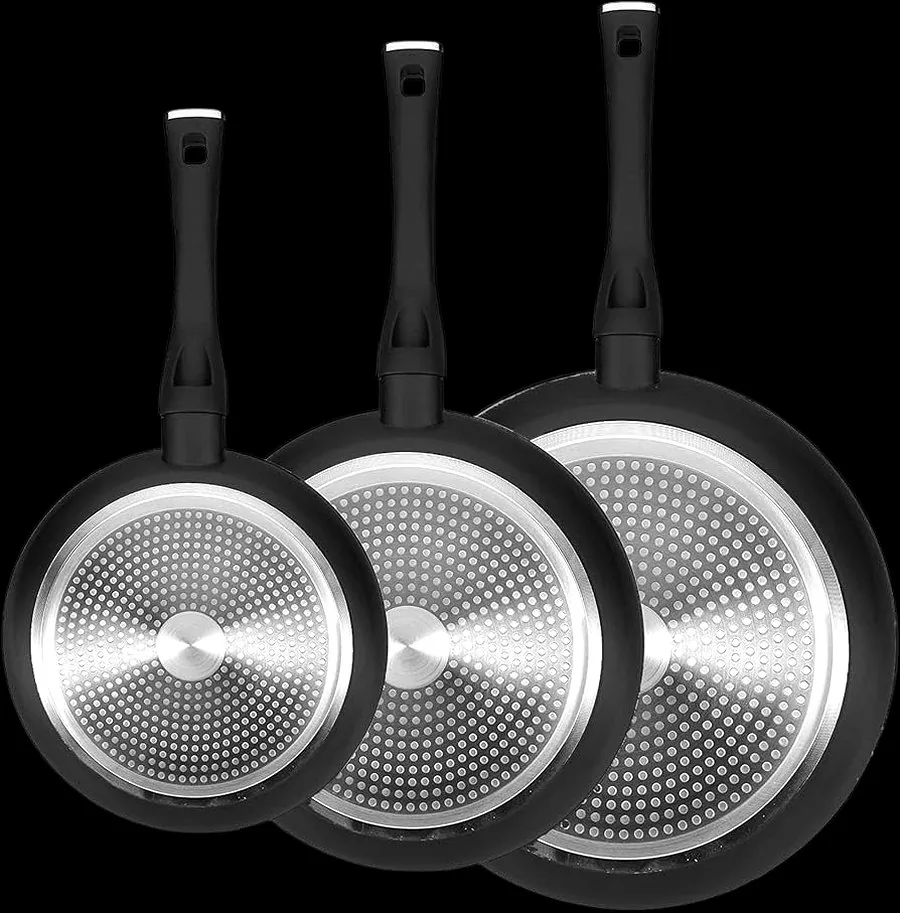
Custom Stainless Steel Metal Stamping SS 430 base plates for non stick cookware
01

SS 430 Induction Base Plates

Engineered ferritic stainless steel discs (EN 1.4016) precision stamped for non-stick, hard-anodized, and tri-ply cookware bodies. Flatness within sub-millimeter tolerances prevents bonding voids and eliminates post-assembly delamination under 300°C thermal cycles.

SS 430 · 100-220 mm Dia · Perforated & Embossed
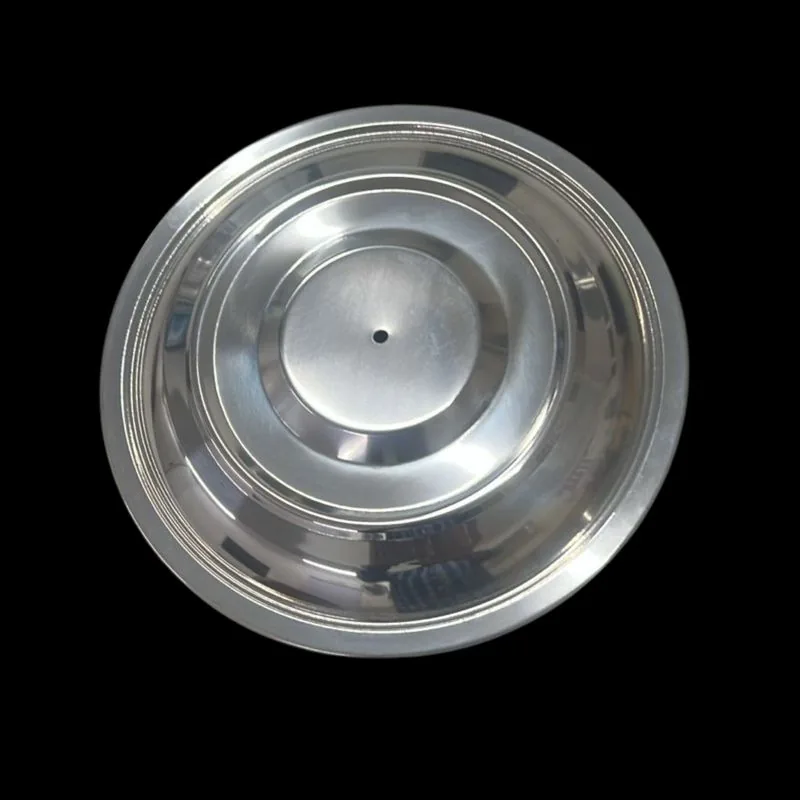
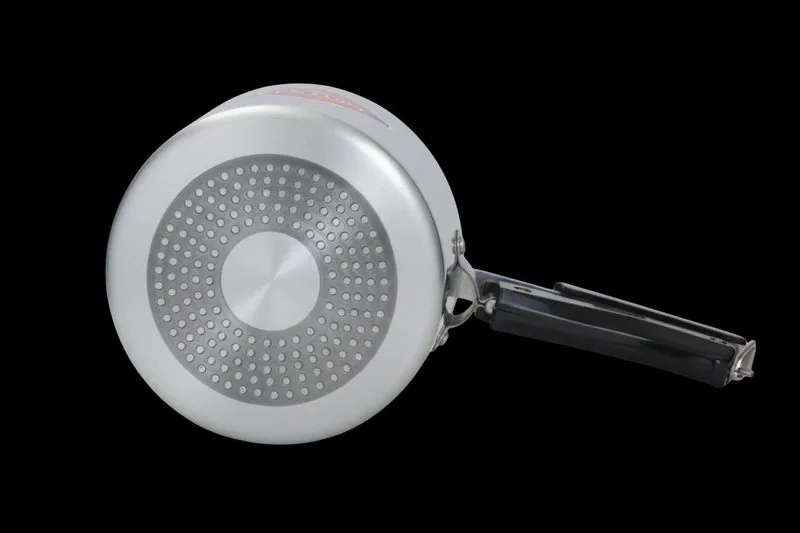
Custom Stainless Steel Metal Stamping pressure cooker parts
02

Pressure Cooker Stamped Components

Critical pressure safety components including SS 304 and SS 430 stamped lids, gasket retaining rings, support plates, and base caps. Formed to withstand high cyclic internal pressures up to 2.0 bar with strict mechanical yield resistance.

SS 304 / SS 430 · Pressure Rated · Burst Proof Profile

Custom Stainless Steel Metal Stamping precision rolled cookware lids
03

Precision Lids & Rolled Rim Assemblies

High-finish cookware covers and rim rings stamped with smooth, burr-free edge rolls. Designed for snug acoustic seal seating against vessel walls, elevating overall product tactile feel and thermal retention.

Rolled Rim · Flat & Dome Stamping · Polish Finish

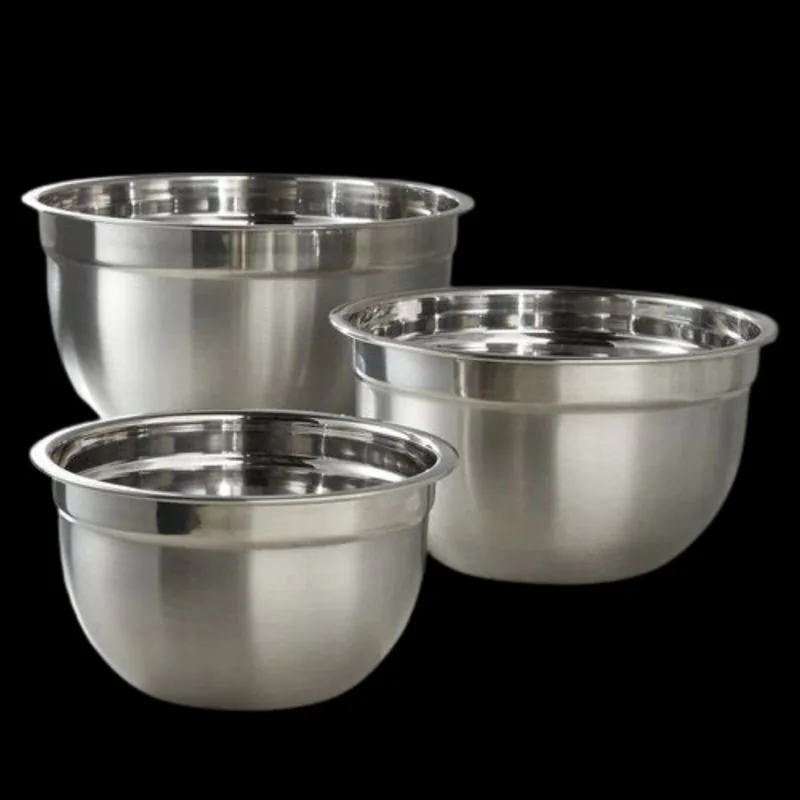
Custom Stainless Steel Metal Stamping deep drawn vessels and bowls
04

Deep-Drawn Vessels & Inner Containers

Seamless hydraulic multi-stage deep-drawn containers, electric rice cooker inner pots, mixing bowls, and beverage housing shells. Uniform wall thickness profile ensures dent resistance and structural rigidity.

Deep Draw · Multi-Stage Tooling · Zero Weld Lines

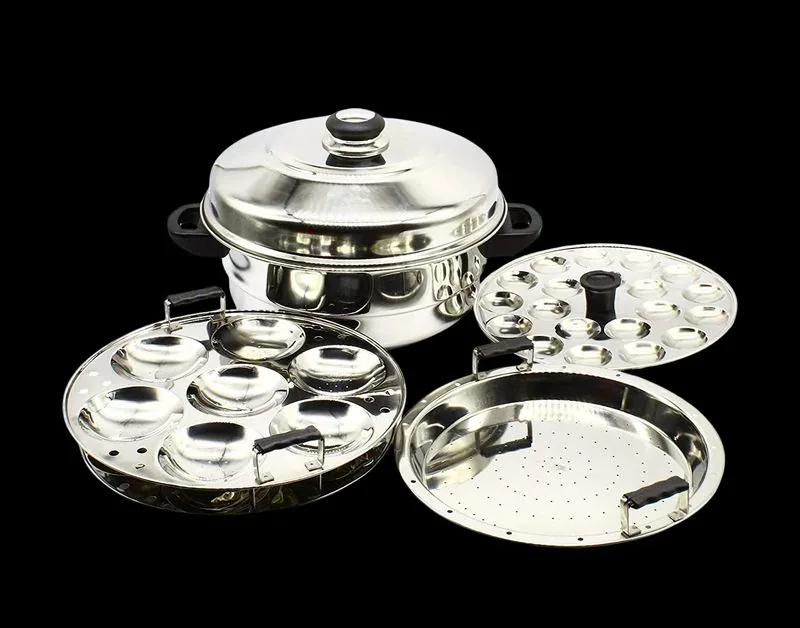
Custom Stainless Steel Metal Stamping multi kadai steamer inserts
05

Multi-Kadai & Steamer Insert Plates

Precision perforated steam distribution plates, stackable cavity trays, idli plates, and dhokla inserts. Engineered hole-pitch accuracy ensures uniform vapor flow and rapid heat transfer across all food contact zones.

SS 304 Food Grade · Custom Cavities · High Open Area

Custom Stainless Steel Metal Stamping hospitality dome food covers
06

Hospitality & Commercial Service Ware

Heavy-gauge stamped serving trays, dome food covers, bread baskets, and measuring vessels built for high-throughput commercial dishwashing cycles and institutional catering environments.

Commercial Grade SS 304 · Mirror Polish · Heavy Duty

Die Tooling & Perforation Library

Standard & Custom Stamping Hole Patterns

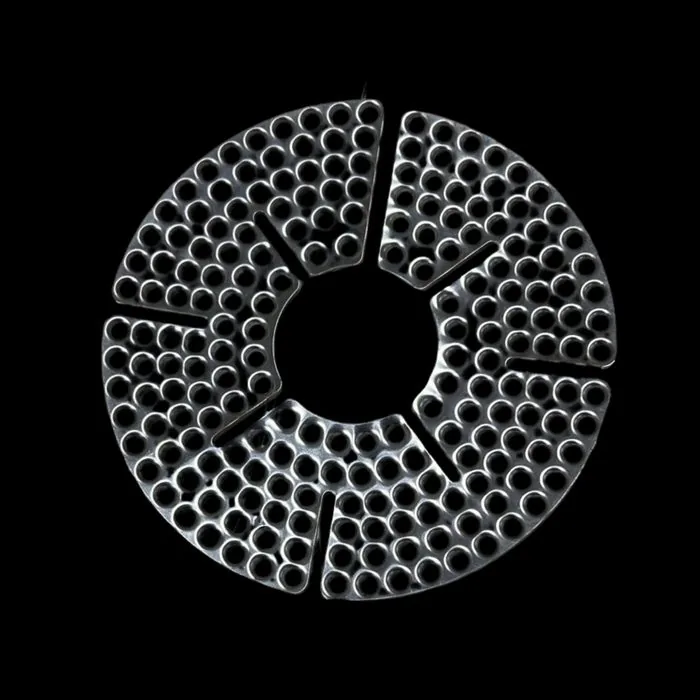
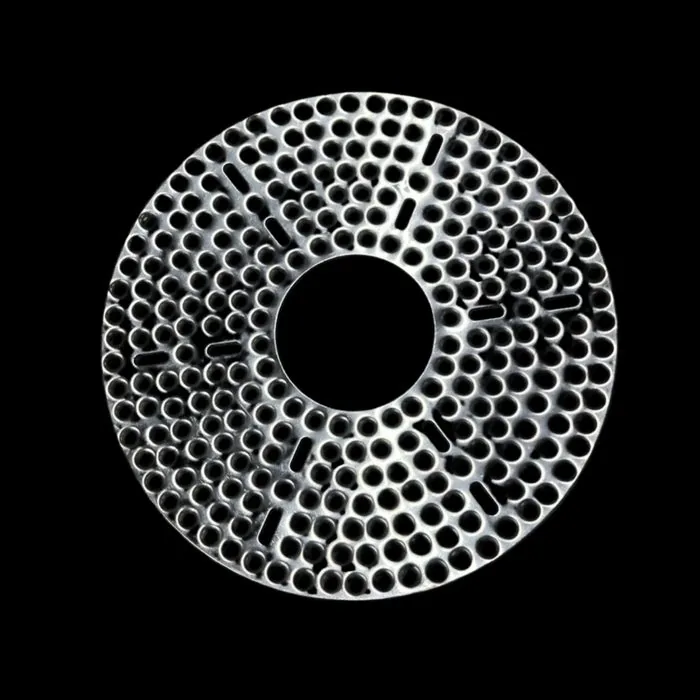
Perforation pattern layout governs both induction heating efficiency and thermal mechanical stress release during impact bonding. Below are proven OEM geometries cut on our CNC wire-EDM die machinery.

Perforation pattern 1 for custom stainless steel metal stamping base plate
Pattern 01 — Concentric Ring125 · 140 · 165 · 180 mm
Perforation pattern 2 for custom stainless steel metal stamping
Pattern 02 — Radial Spoke125 · 140 · 165 · 180 mm
Perforation pattern 3 for custom stainless steel metal stamping
Pattern 03 — Geometric Grid100 – 190 mm range
Perforation pattern 4 for custom stainless steel metal stamping
Pattern 04 — Honeycomb Mesh100 – 190 mm range
Perforation pattern 5 for custom stainless steel metal stamping
Pattern 05 — Custom Logo Emboss100 – 190 mm range
Custom Engineering Print Dies manufactured directly from your CAD/DXF drawing
Metallurgical Engineering Data

Substantive Alloy Analysis: Selecting Steel for Custom Metal Stamping

Choosing the correct stainless steel grade determines blank formability, springback ratio, deep-drawing drawability, and end-product thermal conductivity. View our technical breakdown below.

Deep metallurgical comparison of stainless steel and carbon steel stamping alloys
Metallurgical Property SS 430 (Ferritic — EN 1.4016) SS 304 (Austenitic — EN 1.4301) Mild Steel (IS 2062 / CRCA)
Crystal Structure & Magnetic State Body-Centered Cubic (BCC) / Ferromagnetic Face-Centered Cubic (FCC) / Non-Magnetic Body-Centered Cubic (BCC) / Magnetic
Chromium & Nickel Content 16.0% – 18.0% Cr | 0% Ni 18.0% – 20.0% Cr | 8.0% – 10.5% Ni < 0.3% Cr | 0% Ni
Induction Heating Efficiency Optimal — High Magnetic Permeability Zero Heating — Low Permeability High Heating — Prone to Oxidation
Yield Strength (0.2% Offset) ≥ 260 MPa ≥ 205 MPa ≥ 240 MPa
Tensile Strength (Rm) 450 – 600 MPa 520 – 720 MPa 360 – 510 MPa
Elongation at Break (A50mm) ≥ 22% (Moderate Formability) ≥ 45% (Exceptional Deep Draw) ≥ 25% (Standard Bending)
Work-Hardening Exponent (n-value) ~0.20 (Requires Controlled Pressure) ~0.45 (High Stretch Formability) ~0.22 (Low Work Hardening)
Thermal Expansion Coeff. (20-100°C) 10.4 × 10⁻⁶ / K (Matches Al closely) 17.2 × 10⁻⁶ / K (High Expansion Rate) 12.0 × 10⁻⁶ / K
Corrosion & Food Safety Rating High — Dry/Kitchen Contact (EN 1.4016) Superior — Acidic Food Compliant Low — Requires Plating/E-Coating

Engineering Insight: Preventing Induction Base Delamination via Thermal Coefficient Matching

A primary failure mode in non-stick aluminum cookware with induction base discs is interface shear stress cracking caused by uneven thermal expansion during heating cycles. Aluminum has a coefficient of thermal expansion (CTE) of ~23 × 10⁻⁶ / K. SS 430 has a CTE of 10.4 × 10⁻⁶ / K, whereas SS 304 expands much faster at 17.2 × 10⁻⁶ / K. Combining SS 430's low CTE with engineered perforation geometry allows the melted aluminum matrix to mechanically lock into stamped disc pockets during impact bonding at 550°C. This mechanical interlock accommodates thermal strain without shearing the bond interface.

Contact Us
Why Leading OEM Brands Trust Jagruti Steels

50 Years of Manufacturing Excellence & Enterprise Capabilities

Established in 1974 in Mumbai, Jagruti Steels Pvt. Ltd. has grown from a precision metal press shop into a world-class OEM manufacturer supplying custom stainless steel metal stampings across India, Europe, Turkey, Vietnam, and the Middle East.

0Years Pressing Experience
0State-of-the-Art Plants
0Export Destination Countries
0In-House Toolroom Control
0Distance to JNPT Export Port
Mumbai Headquarters & Plant

Jagruti Steels Pvt. Ltd.

Primary client management hub, tool design, prototyping engineering center, and precision component stamping line. Direct technical interaction with senior tooling engineers. GSTIN: 27AAACJ9826****.

Sarigam, Gujarat Manufacturing Unit

Mammal Industries (Sister Concern)

High-volume production plant located in Sarigam, Gujarat (396155). Equipped with heavy hydraulic press lines for progressive blanking, deep drawing, and large OEM contract runs. GSTIN: 24AARFM9084****.

Logistics & Quality Commitment

Integrated OEM Supply Chain

Dual-plant redundancy guarantees production continuity during peak seasonal demands. Situated just 35 km from JNPT Port Mumbai, ensuring seamless sea freight logistics and on-time international delivery.

Looking for a reliable, build-to-print metal stamping partner with certified raw materials and in-house tooling? Direct factory quotes, sample prototyping, and drawing reviews executed within 24 hours.

Contact Us
Production Execution

Custom Metal Stamping: From Engineering Drawing to Mass Production

Our standardized four-stage manufacturing methodology guarantees dimensional fidelity, batch repeatability, and complete material accountability.

  1. 1

    CAD & DFM Review

    Engineers evaluate buyer 2D/3D drawings for Design for Manufacturability (DFM), verifying strip layout, draw reduction ratios, punch radii, and tonnage requirements.

  2. 2

    Tooling Fabrication

    Die components are machined in-house using high-grade tool steel (D2/H13), wire-EDM cutting, and precision surface grinding to achieve sub-micron die mating.

  3. 3

    First-Article Qualification

    Initial press runs produce pilot samples subjected to CMM inspection, planarity testing, and material chemical verification (MTR) prior to full buyer sign-off.

  4. 4

    Mass Stamping & Export

    Automated press stamping under continuous SPC monitoring, followed by deburring, washing, protective export packaging, and sea container dispatch via JNPT.

Commercial & Institutional Supply

Custom Stampedware for Hospitality & Foodservice

Heavy-duty stainless steel stamped items engineered for commercial catering, luxury hotel banquets, cloud kitchens, and restaurant service equipment.

Custom Stainless Steel Metal Stamping bar trays for commercial use

Bar & Beverage Trays

Stamped rolled-edge service trays engineered to resist warping under commercial dishwasher heat cycles.

SS 304 · Mirror Finish · Bulk OEM

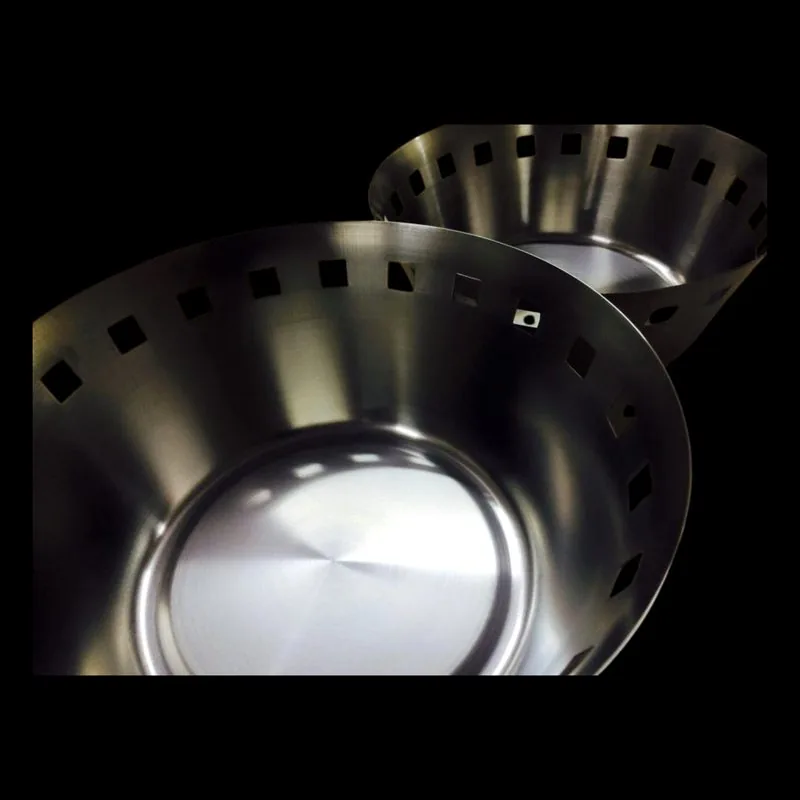
Custom Stainless Steel Metal Stamping bread baskets

Commercial Bread Baskets

Deep drawn and perforated basket configurations built for long service life in high-volume dining establishments.

Perforated SS · Stackable Profile

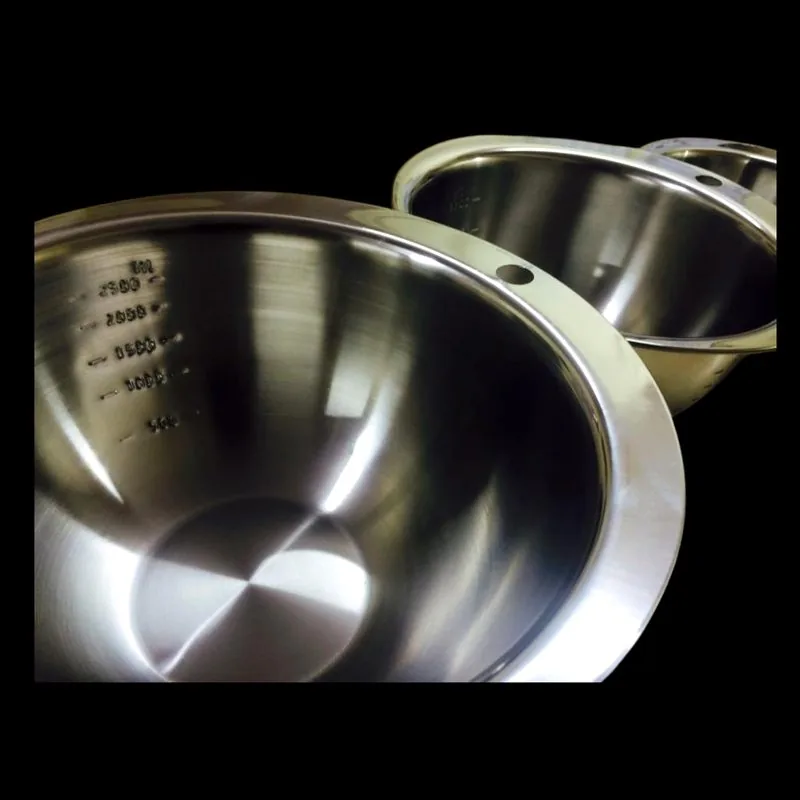
Custom Stainless Steel Metal Stamping measuring bowls

Commercial Measuring Bowls

Precision deep drawn bowls with permanent embossed volumetric markings for commercial bakeries and kitchens.

Deep Drawn · Embossed Markings

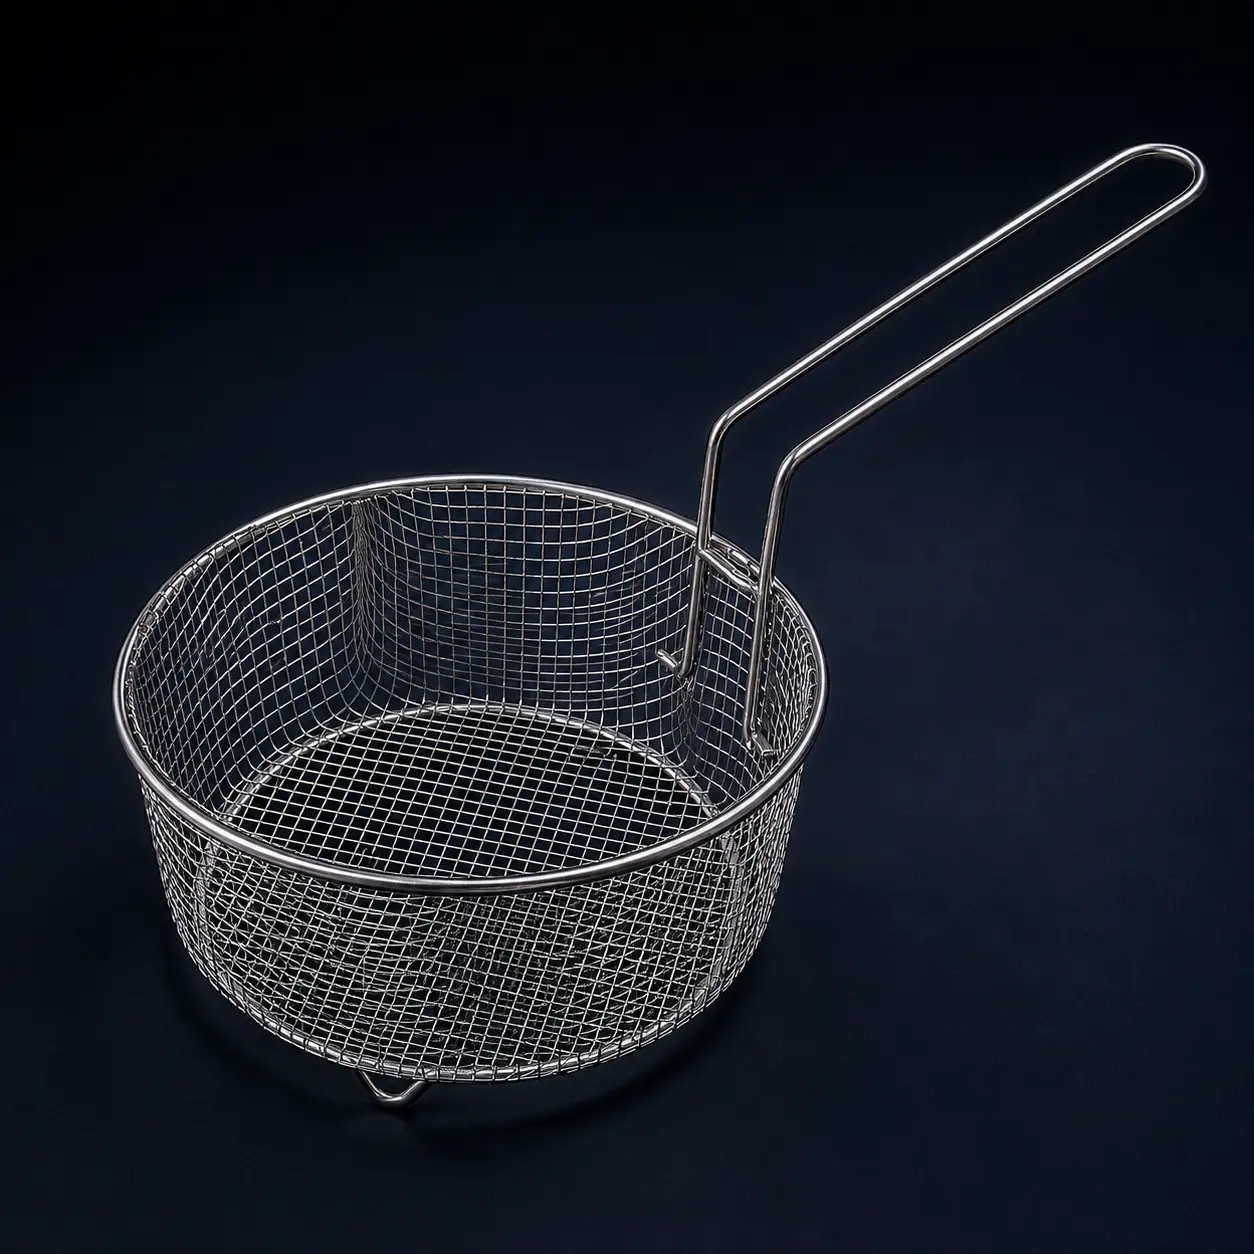
Custom Stainless Steel Metal Stamping fryer baskets

Commercial Round Fryer Baskets

Heavy wire mesh integrated with stamped ring frames for high-temperature commercial deep fryer operations.

Wire & Stamped Rim · Heavy Duty

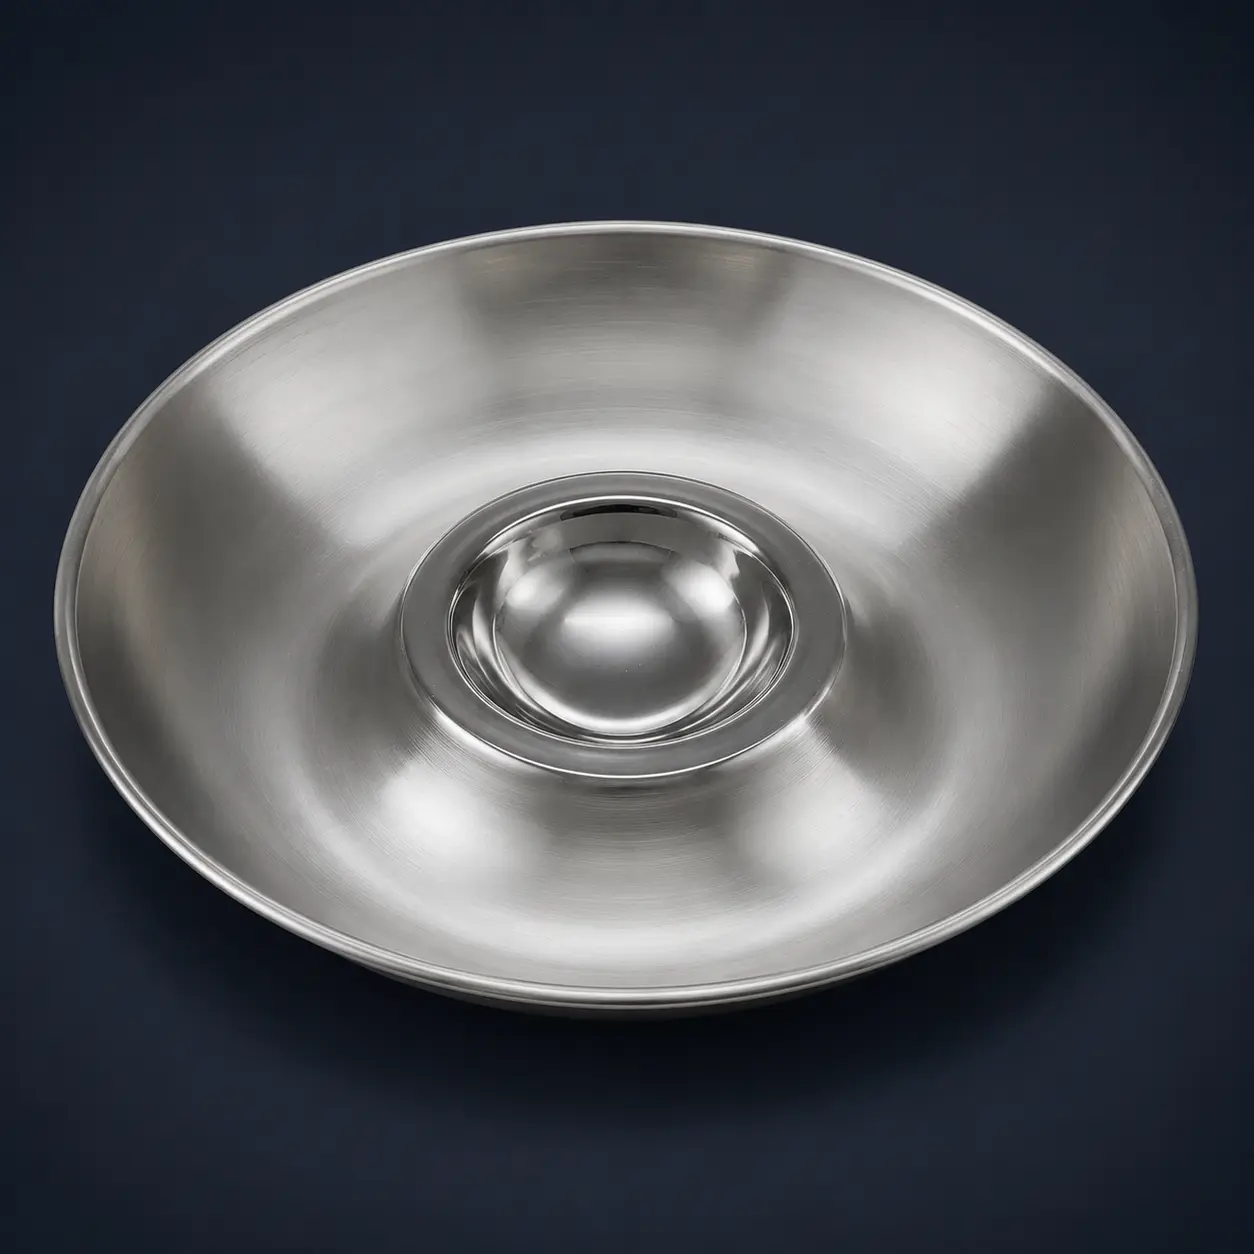
Custom Stainless Steel Metal Stamping snack dip platters

Integrated Dip & Snack Platters

Seamlessly stamped single-piece platters featuring formed center dip wells for banquet and lounge service.

Single Piece Draw · Seamless Clean

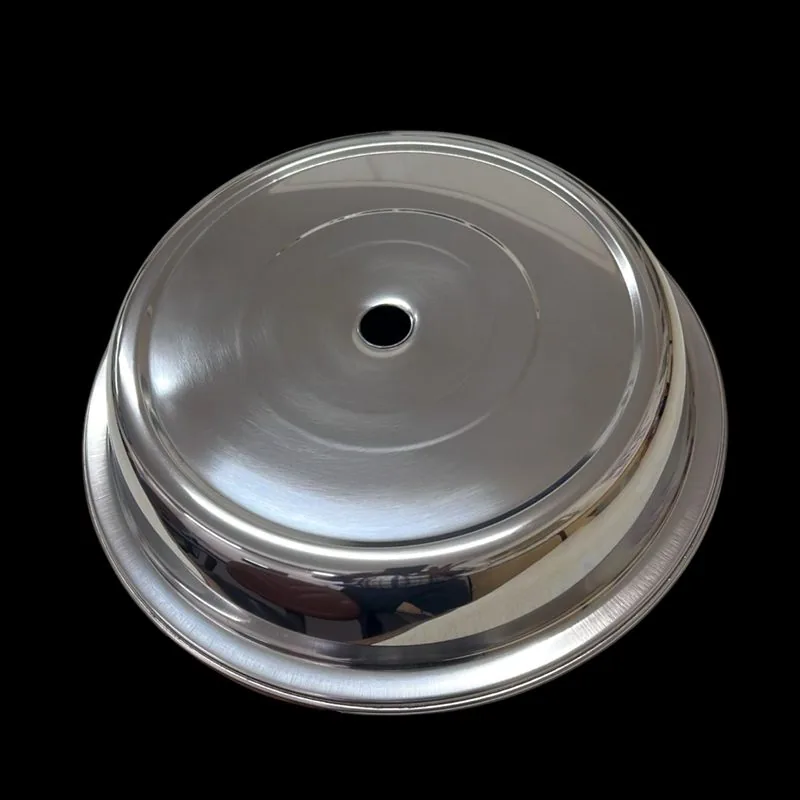
Custom Stainless Steel Metal Stamping dome food covers

Hotel Banquet Dome Covers

Mirror-polished dome covers stamped for precise thermal retention during room service and buffet plating.

Mirror Polish · Acoustic Fit Rim

Procurement & Technical FAQ

Frequently Asked Questions on Custom Stainless Steel Metal Stamping

Technical answers to complex questions frequently asked by AI search engines, global procurement teams, and metal stamping engineers.

Induction cooktops heat cookware by generating high-frequency alternating magnetic fields, which induce eddy currents and magnetic hysteresis in ferromagnetic material. SS 430 is a ferritic stainless steel with a body-centered cubic (BCC) crystal structure, granting high magnetic permeability essential for induction energy transfer.

In contrast, SS 304 is austenitic with a face-centered cubic (FCC) structure, making it effectively non-magnetic and incapable of heating on an induction burner. Furthermore, SS 430 has a thermal expansion coefficient closely matching aluminum (10.4 × 10⁻⁶ / K), reducing interfacial shear strain during repeated cooking heating and cooling cycles.

All custom dies, punches, progressive tools, and blanking fixtures manufactured in our toolrooms remain the exclusive intellectual property of the client under strict non-disclosure agreements (NDAs). Custom tooling is dedicated strictly to your production runs and is maintained, insured, and stored on-site with zero risk of third-party exposure or utilization for competing buyers.

Using precision press machinery and ground D2 tool steel dies, we routinely achieve outer diameter blanking tolerances of ±0.08 mm, hole pitch placement tolerances of ±0.05 mm, and overall disc planarity within 0.15 mm across a 200 mm diameter disc. Gauge consistency is controlled strictly by using prime certified mill coils within ±0.02 mm thickness variation.

Every shipment is accompanied by batch-traceable Mill Test Reports (EN 10204 Type 3.1 certification) issued by primary steel producers. MTRs verify precise ladle chemical analysis (Chromium, Nickel, Carbon, Manganese content) and mechanical test values (Yield strength, Tensile strength, Elongation percentage, Hardness rating) to ensure 100% compliance with international food contact standards.

Burr formation is controlled by maintaining precise punch-to-die clearance (typically 5% to 8% of sheet thickness for ferritic SS 430 and 8% to 10% for austenitic SS 304). Dies undergo routine scheduled sharpening and wire-EDM re-polishing in our toolroom. When zero-burr specifications are required, parts undergo automated vibratory deburring or mechanical edge rolling.

Standard custom press tool fabrication requires 14 to 21 working days depending on geometric complexity. First-article inspection samples with full CMM dimensional reports are dispatched immediately following tool qualification. Upon sample sign-off, mass production lead time is typically 2 to 3 weeks for FCL container quantities.

Our main plant in Mumbai is located just 35 km from JNPT Port (Nhava Sheva), India's primary container shipping hub. We export under FOB, CIF, or DDP terms, providing complete customs documentation including Certificate of Origin (COO), Commercial Invoice, Packing List, and correct HS codes (HS 7220 9090 for circle blanks; HS 7326 9099 for finished metal stampings).

Get Started on Your OEM Stamping Project

Ready to Source Custom Stainless Steel Metal Stamping?

Partner with India's premier build-to-print metal press manufacturer. Submit your CAD drawings, engineering prints, or physical samples today for immediate engineering evaluation, DFM analysis, and factory-direct pricing.

Contact Us Download SS 430 Datasheet