Direct from Huicong OEM/ODM Factory | ISO 9001 Certified Sheet Metal Deep Drawing Showcase
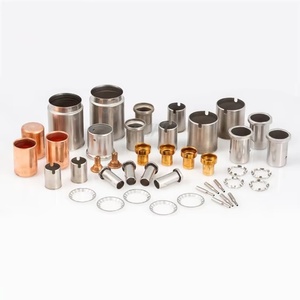
Engineered for seamless structural integrity using ultra-low carbon steel and high-ductility 5052/6061 aluminum alloy formulations.
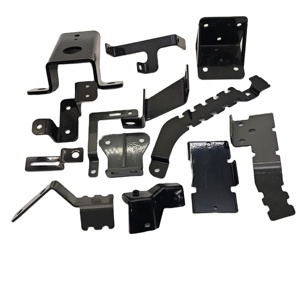
Heavy-duty stainless steel and aluminum deep drawn enclosures built on progressive stamping lines with micro-gap surface finishing.
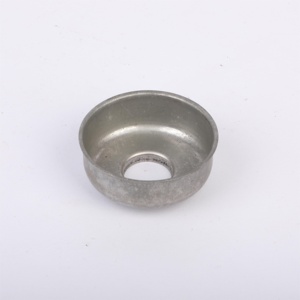
Corrosion-resistant austenitic stainless steel shells engineered for severe industrial fluid control, pneumatic devices, and pressure shielding.
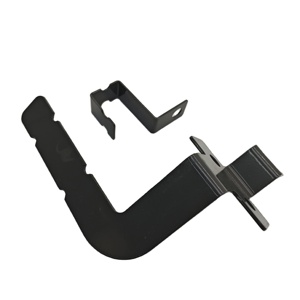
Multi-stage progressive deep drawing with zero-wrinkle wall forming, specialized for automotive sensors and electronic shielding cans.
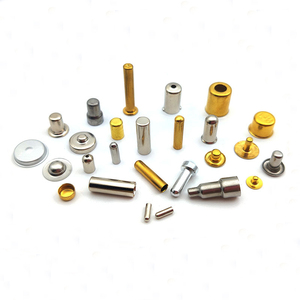
Flagship Huicong Brand ultra-precision stampings executed on hydraulic press lines ranging from 6.3 tons up to 600 tons of clamping force.
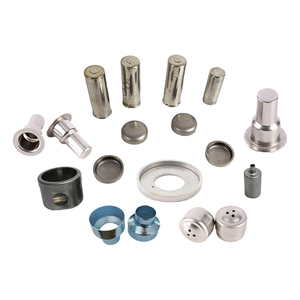
Advanced cylindrical and rectangular vessel draw tooling designed for severe operating pressures, heat exchangers, and filter housing bodies.
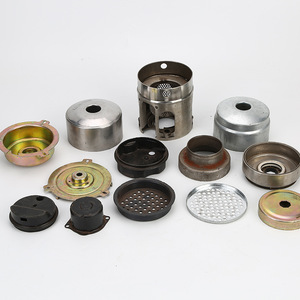
Deep cavity seamless forming with customized bead patterns and edge flanging for commercial kitchenware, HVAC, and pump housing assemblies.
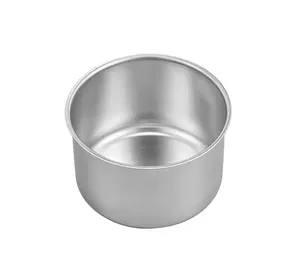
Anodized and passivated aerospace-grade aluminum deep draws delivering exceptional strength-to-weight ratio for critical flight systems.
Deep drawing is a specialized sheet metal forming process in which a metallic blank is radially drawn into a forming die by the mechanical action of a punch. As a premier Top China Deep Drawn Manufacturer & Factory, Huicong Brand engineering operations focus on mastering the complex plastic deformation mechanics required to yield high-aspect-ratio hollow bodies without structural defects such as wrinkling, tearing, or severe earing.
The feasibility of a deep drawn component is governed primarily by the Limiting Draw Ratio (LDR), which defines the maximum ratio of blank diameter to punch diameter that can be drawn in a single operation without fracturing the sidewalls. For standard deep-drawing steels (such as DC04, DD14, and austenitic SS 304), the single-stage LDR typically ranges between 1.9 and 2.2. Achieving deeper cavities requires precise multi-stage re-drawing schedules paired with intermediate vacuum annealing to relieve work-hardening stresses (strain hardening exponent n-value restoration).
| Material Grade | Yield Strength (MPa) | Tensile Strength (MPa) | Max Single-Stage Draw Ratio (LDR) | Typical Applications |
|---|---|---|---|---|
| Stainless Steel 304 / 304L | 205 - 240 | 515 - 620 | 2.10 - 2.25 | Food processing cases, deep drawn covers, medical enclosures |
| Stainless Steel 316 / 316L | 240 - 290 | 580 - 680 | 2.00 - 2.15 | Marine hardware, chemical metering pumps, aggressive fluid shells |
| Aluminum 5052-O | 90 - 105 | 190 - 230 | 1.85 - 1.95 | Aerospace shields, lightweight automotive housings, heat sinks |
| Deep Draw Quality Steel (DDQ) | 140 - 180 | 270 - 350 | 2.20 - 2.35 | Automotive oil pans, compressor cans, fire extinguisher bodies |
| Copper / Brass (C26000) | 110 - 150 | 300 - 380 | 2.15 - 2.30 | Electrical connectors, cartridge cases, acoustic sensor caps |
Controlling wall thinning tolerances down to ±0.02mm requires absolute control over blank holder pressure (BHP). If the blank holder pressure is set too low, the compressive circumferential stresses in the flange area cause plastic instability, producing visible wrinkling. Conversely, excessive blank holder pressure severely restricts material flow into the die cavity, elevating tensile stresses along the cup radius and resulting in necking or catastrophic rupture. At our 16-year production facility, our hydraulic presses utilize closed-loop proportional valve systems to dynamically modulate blank holder force throughout the stroke profile.
16 Years of Manufacturing Rigor | Integrated Tool Room, Press Hall & Quality Control
Our press hall accommodates both rapid-cycle mechanical presses (6.3T to 160T) for shallow precision stampings and heavy-duty double-action hydraulic presses (200T to 600T) for deep continuous vessel draws up to 400mm depth.
Utilizing high-rigidity progressive dies, tungsten carbide die inserts, and wire-EDM tooling fabrication, we maintain extreme dimensional repeatability across high-volume production batches exceeding 500,000 units.
Our tooling design division uses AutoForm FEA strain analysis to simulate sheet metal flow, predict thin-out zones, and eliminate die trial iterations prior to CNC machining, drastically lowering NRE tooling costs and lead times.
The global precision stamping market is undergoing structural shifts driven by electrification, aerospace lightweighting, and stringent carbon neutral compliance mandate. As global procurement directors rethink supply chain risk and technical capability, several defining engineering trends are shaping the future of metal drawing contracts:
Traditional mild steel deep drawn parts are increasingly replaced by 6000-series aluminum and lightweight titanium alloys in EV battery housings and aerospace solenoid covers. Managing the lower formability and higher springback of these alloys demands servo-electric press stroke profiling and warm-drawing die thermal management.
With miniaturization in medical diagnostic devices and 5G RF shielding, demand for micro-deep drawn components (diameters under 5.0mm with wall thicknesses below 0.10mm) is accelerating. Our factory invests heavily in micro-die tooling capabilities to meet these ultra-fine tolerances.
Global buyers are abandoning secondary machining steps. Modern deep drawing dies integrate in-die tapping, side-piercing, roll-threading, and automated vision inspection inside a single press cycle, delivering finished components straight off the machine.
Environmental regulations are driving the adoption of bio-based water-washable lubricants and dry-film lubricant coatings, replacing heavy chlorine/sulfur extreme-pressure oils to simplify degreasing and lower VOC footprint.
By aligning our production capacity with these advanced trends, Huicong Brand ensures that long-term procurement partners receive future-proof components compliant with international RoHS, REACH, and ISO 14001 environmental frameworks.
Direct Technical & Commercial Answers for Global Supply Chain Managers
A metal part is classified as deep drawn when its total depth exceeds its internal diameter or cross-sectional width (typically a depth-to-diameter ratio greater than 0.5). Standard stamping involves shallow bending, blanking, or coining where the sheet metal experiences minimal wall thinning. Deep drawing involves complex 3D plastic deformation, requiring controlled blank holding force to stretch and draw material into seamless tubular or box-shaped cavities.
We protect aesthetic and functional surfaces through three primary measures: first, utilizing premium Physical Vapor Deposition (PVD) coated dies (such as TiCCN or TD coatings) or Ampco bronze inserts; second, applying high-performance synthetic lubricants or protective polyethylene (PE) films on the raw sheet; and third, implementing automated robotic arm transfer systems to prevent inter-part contact during ejection.
Our standard production tolerance on wall thickness is ±0.05mm, but for high-precision OEM applications (such as automotive fuel rails or sensor housings), we maintain tight tolerances down to ±0.02mm. Outer diameter (OD) and inner diameter (ID) tolerances are controlled via secondary ironed re-strike stages to guarantee precision press-fits.
Every shipment from our factory is accompanied by a comprehensive Quality Pass Dossier. This includes Raw Material Mill Test Certificates (MTC with chemical composition and mechanical strain values), Full Dimensional Inspection Reports via CMM (Coordinate Measuring Machine), Surface Roughness Test Logs, Plating/Coating Thickness Certificates, and PPAP Level 3 documentation upon request.
For standard single-stage or progressive tooling, die design and AutoForm simulation require 5 to 7 working days. Die fabrication, wire-EDM cutting, and assembly take 20 to 30 days. Initial T1 samples are supplied with full inspection reports within 35 days of drawing sign-off. Expedited tooling schedules are available upon request.
We operate an end-to-end manufacturing campus. Secondary operations include automated centrifugal disc deburring, ultrasonic degreasing, nitric acid passivation for stainless steel, anodizing for aluminum, electropolishing, powder coating, electroplating (zinc, nickel, chrome), and laser engraving for brand logos or serial numbers.
Work directly with China's leading deep draw tooling engineers. Receive DFM analysis, AutoForm simulation feedback, and competitive factory pricing within 24 hours.
