

4/4.5/5in Hot Pressed Super Thin Continuous Rim Turbo Diamond Circular Saw Blade
Precision diamond turbo cutting disc for chipless cutting of tile, porcelain, ceramic, and dense mineral substrates in industrial cookware plant setups.
Explore our high-performance OEM cookware components, press tooling, and diamond cutting blades engineered for heavy-duty commercial food service and cookware processing plants.
Precision diamond turbo cutting disc for chipless cutting of tile, porcelain, ceramic, and dense mineral substrates in industrial cookware plant setups.

Heavy-duty rotary slitting blade designed for plastic film packaging, rubber gasket trimming, and high-speed automated packaging lines for kitchenware.

Ultra-wear resistant tungsten carbide blade engineered for cutting tough rubber seals, pressure cooker silicone gaskets, and industrial polymers.

Zero-chipping hot-pressed diamond cutting wheel optimized for clean edge processing in high-end ceramic cookware and countertop fabrications.

Precision hole punching tool for sheet metal blanking, gasket hole alignment, and circular component forming in auxiliary cookware fabrication.

Vacuum brazed diamond saw blade for rapid cutting and edge grooving of stone materials, ceramic bakeware, and composite cookware linings.

Heavy-duty industrial round die cutter designed for high-precision circle blanking of metal discs, paper liners, and cookware sealing gaskets.

V-segment dry grooving diamond wheel engineered for industrial floor maintenance, factory wall slotting, and structural cookware test facilities.
The global commercial kitchen equipment market is undergoing a seismic shift driven by induction transition mandates, energy cost volatility, and stringent food safety compliance (LFGB, FDA 21 CFR 175.300, and NSF/ANSI Standard 2). Procuring enterprise-grade commercial cookware from China requires evaluating metallurgical composition, impact-bonding integrity, and deep-drawing press capabilities.
Commercial cookware—ranging from heavy-duty stockpots, saute pans, and steam table inserts to pressure cookers and tri-ply clad frying pans—operates under grueling thermal cycling and mechanical stress. Unlike residential kitchenware, commercial food service gear is subjected to continuous high-BTU gas burners, high-frequency commercial induction hobs, aggressive chemical dishwashing detergents, and constant physical impact. Leading OEM manufacturers must master multi-layer metal cladding, zero-cavity deep drawing, and automated surface passivation to prevent delamination, thermal warping, and stress corrosion cracking.
Selecting the optimal alloy matrix is the fundamental foundation of commercial cookware durability. Enterprise buyers must balance thermal conductivity, magnetic permeability for induction hobs, and corrosion resistance against food acids.
| Material Standard | Microstructure | Thermal Conductivity | Induction Magnetism | Corrosion Resistance | Primary Commercial Application |
|---|---|---|---|---|---|
| AISI 304 / EN 1.4301 | Austenitic (18/8 Cr-Ni) | 16.2 W/m·K | Non-Magnetic (Paramagnetic) | Exceptional (High Acid) | Interior vessel liners, stockpots, steamer plates |
| AISI 430 / EN 1.4016 | Ferritic (16-18% Cr) | 26.0 W/m·K | High Magnetic Permeability | High (Food Service Grade) | Induction base plates, capsulated base discs |
| Tri-Ply Clad (304-Al-430) | Composite Sandwich | 160-200 W/m·K (Core) | Full Induction Compatible | Superior Overall | Premium chef pans, saute pans, commercial skillets |
| 3003 Pure Aluminum | Wrought Aluminum | 220 W/m·K | Inert (Requires SS Plate) | Moderate (Anodized) | Heavy-gauge fry pans, impact-bonded cores |
High-volume commercial cooking requires encapsulation of a thick (4mm–6mm) aluminum core between an AISI 304 body and an AISI 430 ferritic stainless steel base plate. High-tier China manufacturers utilize Friction Impact Bonding at temperatures exceeding 750°C and pressures over 2,500 metric tons. This creates a solid-state metallurgical bond that completely eliminates air gaps, preventing delamination and hot spots during extreme commercial usage.
Tri-ply clad metal sheets feature an interior food-grade 18/10 stainless steel layer for inert food contact, a high-purity aluminum core (1050/3003 alloy) for rapid side-wall heat dissemination, and an exterior magnetic stainless steel layer (SS 430). This 3-layer structural integrity ensures multi-directional heat distribution, reducing energy consumption by up to 30% on high-efficiency induction cooktops.
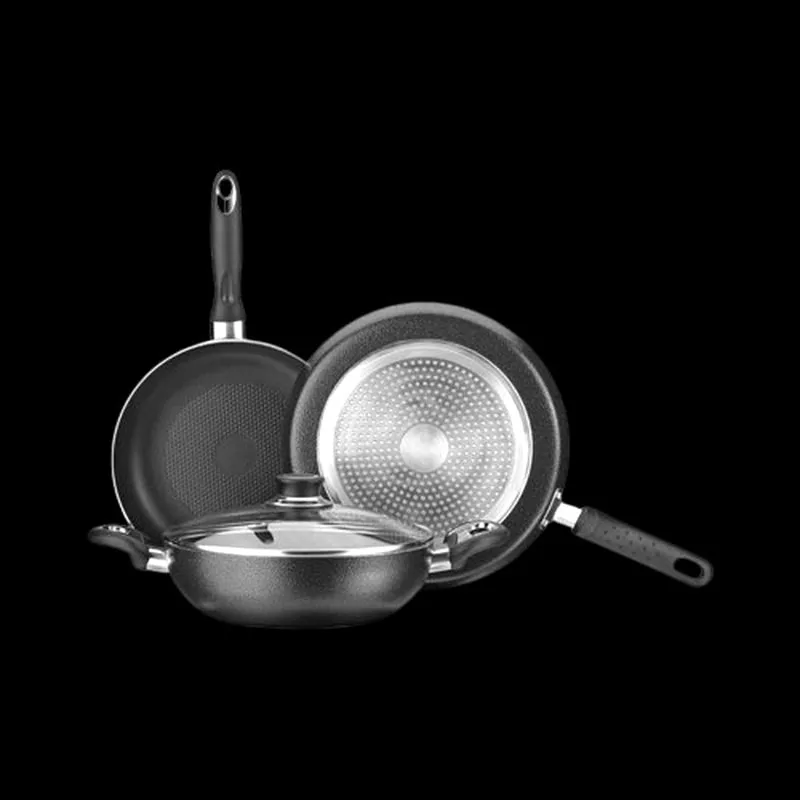
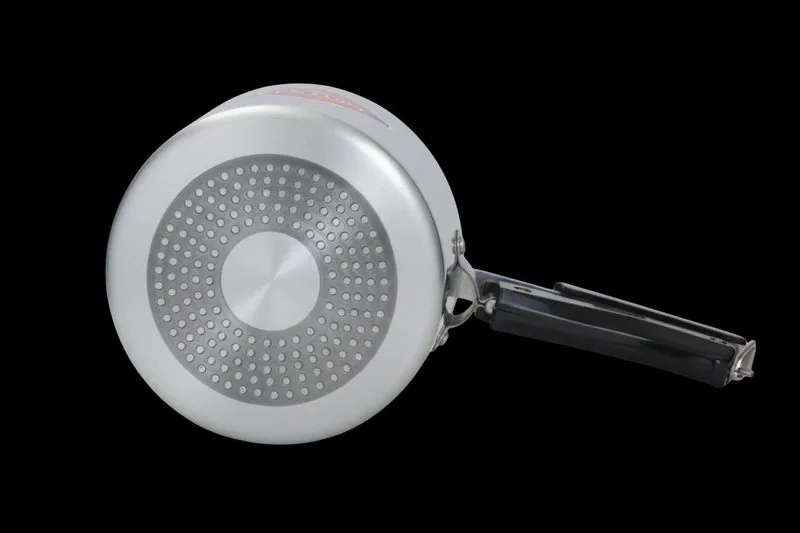
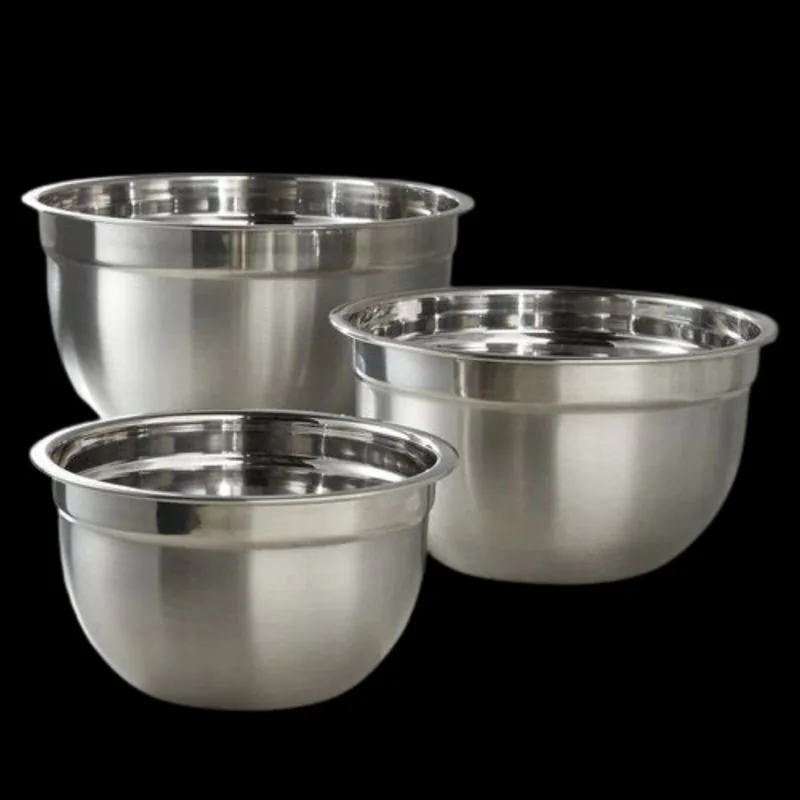
Our advanced manufacturing matrix covers six dedicated OEM component lines, produced entirely in-house using precision dies, multi-stage hydraulic presses, and automated surface polishing.
With over five decades of institutional manufacturing heritage, our plant setup combines automated stamping lines, zero-defect quality control, and direct-port export logistics.
We build and cut stamping, blanking, and drawing dies directly on our plant floor. This guarantees 100% proprietary protection for customer CAD drawings, reduces sample development lead times to under 14 days, and lowers unit tooling costs.
Our multi-facility manufacturing footprint—supported by primary heavy stamping lines and secondary satellite processing units—absorbs seasonal demand surges (Q3–Q4 peak periods) and ensures uncompromised supply chain continuity.
Every coil batch of SS 430 ferritic steel and SS 304 austenitic steel is accompanied by Mill Test Reports (MTRs) detailing chemical analysis (Chromium, Nickel, Carbon) and physical yield testing under ISO 9001:2015 frameworks.
The commercial cookware manufacturing ecosystem is advancing rapidly. B2B buyers and brand managers must align their 3-to-5-year procurement strategies with the following technology vectors:
Global regulations restricting PFAS/PFOA chemicals are accelerating the commercial adoption of non-stick ceramic sol-gel coatings. Next-generation China OEM lines utilize automated robotic spraying and high-temperature curing ovens (400°C) to deliver scratch resistance exceeding 20,000 cycles under BS EN 12983-1 standards.
Commercial kitchens demand ergonomic cookware to minimize chef fatigue. Metallurgical innovations in micro-alloying allow reduction of clad wall thickness from 3.0mm to 2.3mm while maintaining structural rigidity, torsional anti-warping integrity, and induction efficiency.
Automated commercial ghost kitchens and QSR chains are adopting cookware embedded with base heat-sensor cavities or RFID tracking tags. This allows automated induction hobs to modulate wattage dynamically, preventing food scorching and reducing commercial energy footprints.
European and North American buyers increasingly demand ESG accountability. Premier exporters are incorporating up to 75% recycled scrap stainless steel in electric arc furnace (EAF) production, backed by ISO 14064 carbon footprint verification.
Detailed answers to technical, logistical, and compliance questions commonly raised by global purchasing directors and brand managers.
Submit your CAD drawings, product specifications, or target cost requirements directly to our engineering desk. Receive a technical evaluation, die layout plan, and factory-direct quote within 24 business hours.